
01A CLEARER CASTING PURCHASE
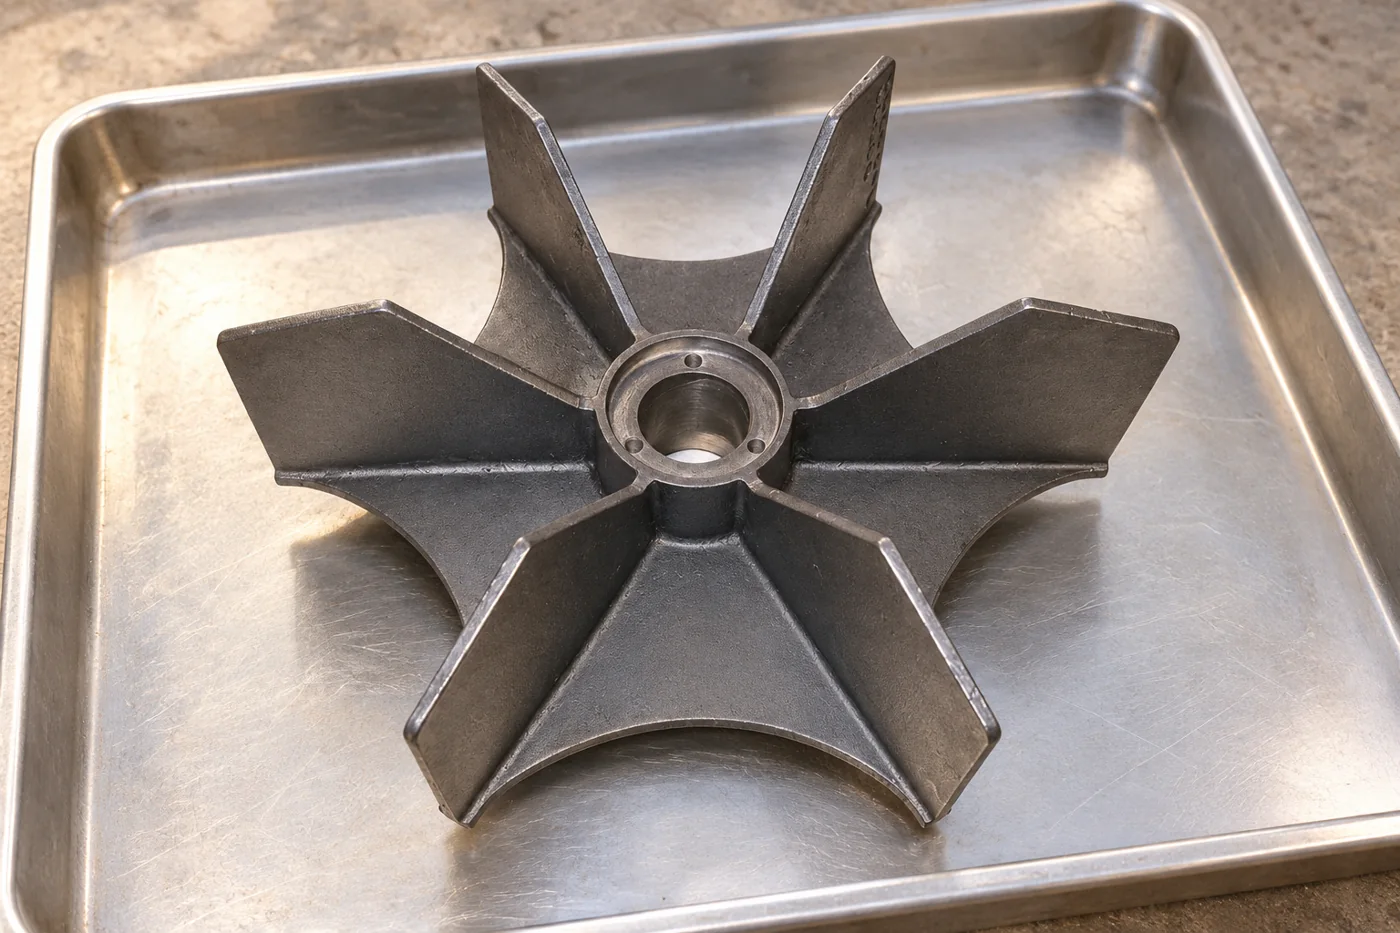
Steel Casting Orders with Linked Production Records
Order the evidence chain alongside the steel casting. Relia’s catalogue includes heat, production-batch and delivery-batch traceability references with selected material, dimensional and examination requirements. Specify the identification level and records your receiving team needs. Each accepted part can then be connected to the relevant material and processing evidence, including split shipments or later treatment groups where applicable.
- Identify
- Part + drawing revision
- Link
- Heat + relevant processing
- Receive
- Delivery group + records
02A CLEARER CASTING PURCHASE
Heat, production and delivery batches identify different events
Relia’s steel-casting offering includes stated heat and batch traceability scope. We can provide dimensional and material test reports; the order needs to connect those records with the actual part identity, selected treatment and dispatch grouping.
A heat identifies a material source, while a production batch can describe a manufacturing grouping and a delivery batch the parts dispatched together. Those identities need not be identical or one-to-one. One delivery may include several production groups; a heat may contribute to more than one later group.
Ask for the mapping your order needs rather than a single batch field used for every stage. At the agreed identification level, connect part number, drawing revision, quantity and material reference to the relevant production and dispatch records. This makes split shipments and mixed heats visible instead of forcing receiving to reconstruct the links.
- 01Heat identityConnect the selected material and relevant test basis.
- 02Production identityConnect the ordered part to its manufacturing grouping and required treatment link.
- 03Delivery identityConnect dispatched quantities and packages to accepted production groups.
- 04Order identityRetain part, revision, grade and purchase reference throughout the mapping.
03A CLEARER CASTING PURCHASE
Material reports contain results and their applicable basis
The material requirement should name the complete grade, governing specification and required condition. The report should identify what was tested, its relation to the heat or component and the results needed for acceptance. Chemical composition and mechanical properties establish different characteristics and should remain distinguishable.
Where the order invokes EN 10204, specify the required inspection-document type and verification responsibilities before production. The standard concerns types of inspection documents; it is not itself a material grade or a guarantee that an unrelated certificate covers the shipment. Keep the ordered technical limits and the material identity available alongside the document designation.
| Record element | Required connection |
|---|---|
| Material definition | Grade, specification, condition and required properties. |
| Test identity | Heat, specimen or component reference applicable to the result. |
| Actual results | Specified chemistry or properties with methods/units as required. |
| Document scope | Agreed inspection-document type and responsible verification. |
04A CLEARER CASTING PURCHASE
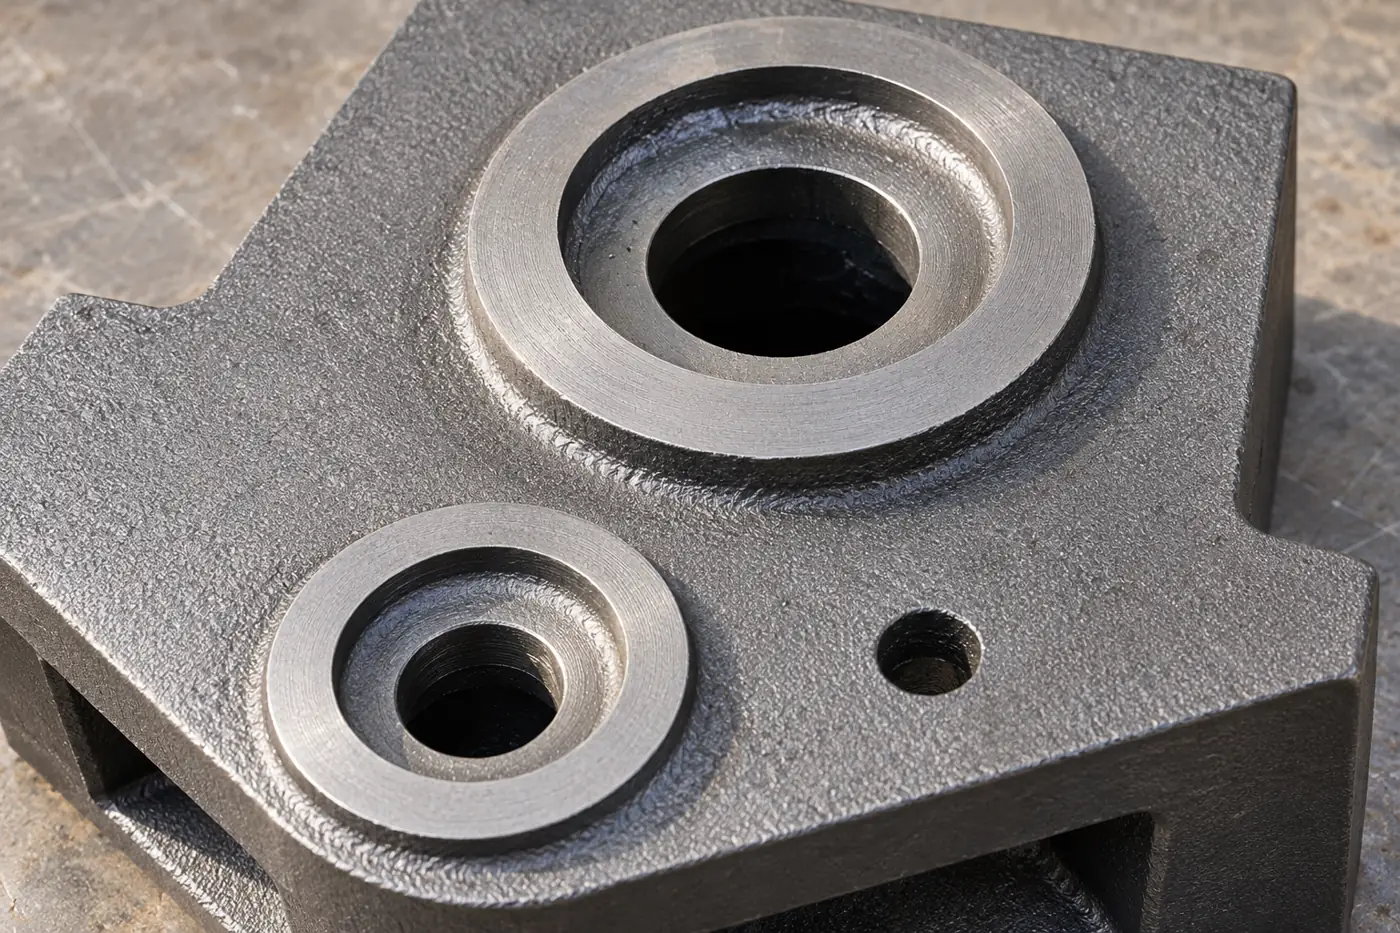
Marking preserves identity without damaging a functional surface
Agree the identification method and location for the actual part. A permanent mark, label or package-level reference has different practical limits, especially after machining, blasting or coating. Do not place a mark on a sealing face or another restricted region simply because it is easy to read there.
The identification plan should explain how the link survives operations that remove or obscure a mark. If individual-part traceability is required, retain it when the batch is divided. If agreed batch-level identification is sufficient, define how mixing is prevented and how receiving connects the parts to their documents.
05A CLEARER CASTING PURCHASE
Treatment records need a mapping to the supplied condition
A heat number does not automatically identify every later treatment operation. Where treatment documentation is required, link the relevant parts or production group to the treatment batch and selected condition. State the records needed, such as the applicable procedure/reference and the evidence relevant to the ordered acceptance.
Do not confuse a process record with a measured material property. A documented treatment cycle can describe what was done; the specified tests establish the required tested characteristics on their stated basis. The order should identify both where needed so the documentation supports the actual delivered condition.
06A CLEARER CASTING PURCHASE
Inspection records state method, coverage and acceptance
Chemical, mechanical, dimensional and NDT checks answer different questions. The inspection plan should identify the characteristic, method, sampling or coverage, acceptance reference and result identity. A dimensional report needs the drawing revision and feature references; a material result needs its relevant specimen or heat basis.
NDT is not a single universal test. Magnetic-particle examination, for example, is used for surface and near-surface indications in ferromagnetic materials. The chosen method must suit the actual alloy and target discontinuities. Naming the method, region and acceptance criteria is more useful than attaching an unqualified NDT-passed line to a shipment.
07A CLEARER CASTING PURCHASE
Split shipments retain their original evidence links
A partial delivery should retain the connection to the original accepted production groups. Map the dispatched quantities to the relevant heat and reports, then carry that mapping into package references. Do not renumber a mixed delivery as one new batch if doing so removes the underlying material identity.
For receiving, a simple cross-reference schedule can be more useful than repeating entire reports in every folder. It should allow a part or box reference to lead to the applicable documents and accepted quantities. The agreed identification level determines how detailed that schedule must be.
08A CLEARER CASTING PURCHASE
Revisions and corrective work remain visible in the record
A report for an earlier drawing may not address a changed bore, wall or material condition. Keep the technical revision attached to the inspected characteristics and identify any later operation that affects them. If corrective work or reinspection is required, retain the affected identity and resulting acceptance record.
The final dossier should distinguish original results, approved changes and follow-up checks. This prevents a superseded report from being mistaken for acceptance of the latest supplied version. It also gives repeat procurement a clearer basis for identifying which specification and inspection package were actually accepted.
- 0101Release the grade, drawing and required record schedule.
- 0202Connect manufacturing and test identities to the parts.
- 0303Record affected changes, corrective work and reinspection.
- 0404Issue the aligned delivery index and applicable final records.
09A CLEARER CASTING PURCHASE
Packing connects physical quantities with the dossier
Keep accepted groups separated or otherwise controlled according to the agreed traceability level. Package references should connect the quantity inside to the part/revision and applicable record index. Protect identification during transport and avoid labels that detach or become unreadable before receipt.
If several grades or trial versions share a shipment, retain their distinction in both the pack list and document schedule. Your receiving team should be able to reconcile quantities and locate the correct results without inferring material identity from a casting’s appearance or the position of a box on the pallet.
10A CLEARER CASTING PURCHASE
The traceability RFQ specifies a usable handover
Send the part schedule, drawings, selected steel grade and quantities with the required record chain. Identify the marking level, material and treatment evidence, inspection methods and delivery-index format. Name the approval stages at which your team needs the documents.
We can review the casting and documentation scope together so the quotation identifies the required evidence and responsibilities. The deliverable is an order-linked record package for the actual supplied parts, not an invented example certificate or a general qualification document presented as the material history of your shipment.
11 YOUR NEXT STEP
Bring your component into the conversation
Tell us which component you need, the material, quantity and required supplied condition. Relia will connect your enquiry with the casting, machining and evidence relevant to that part.
Technical reading and scope
Technical references explain the process. Component specifications and agreed order records define the actual supply.
DIN EN 10204: Types of inspection documentsTWI: Magnetic-particle examination scope- [email protected]
- Phone
- +86 18561762631
- +1 404 203 0971
- Company and address
- Qingdao Relia Industries Co., Ltd.
Shuyuan Road, Qingdao, Shandong, China