
01A CLEARER CASTING PURCHASE
Grey-Iron Water Pump Housings
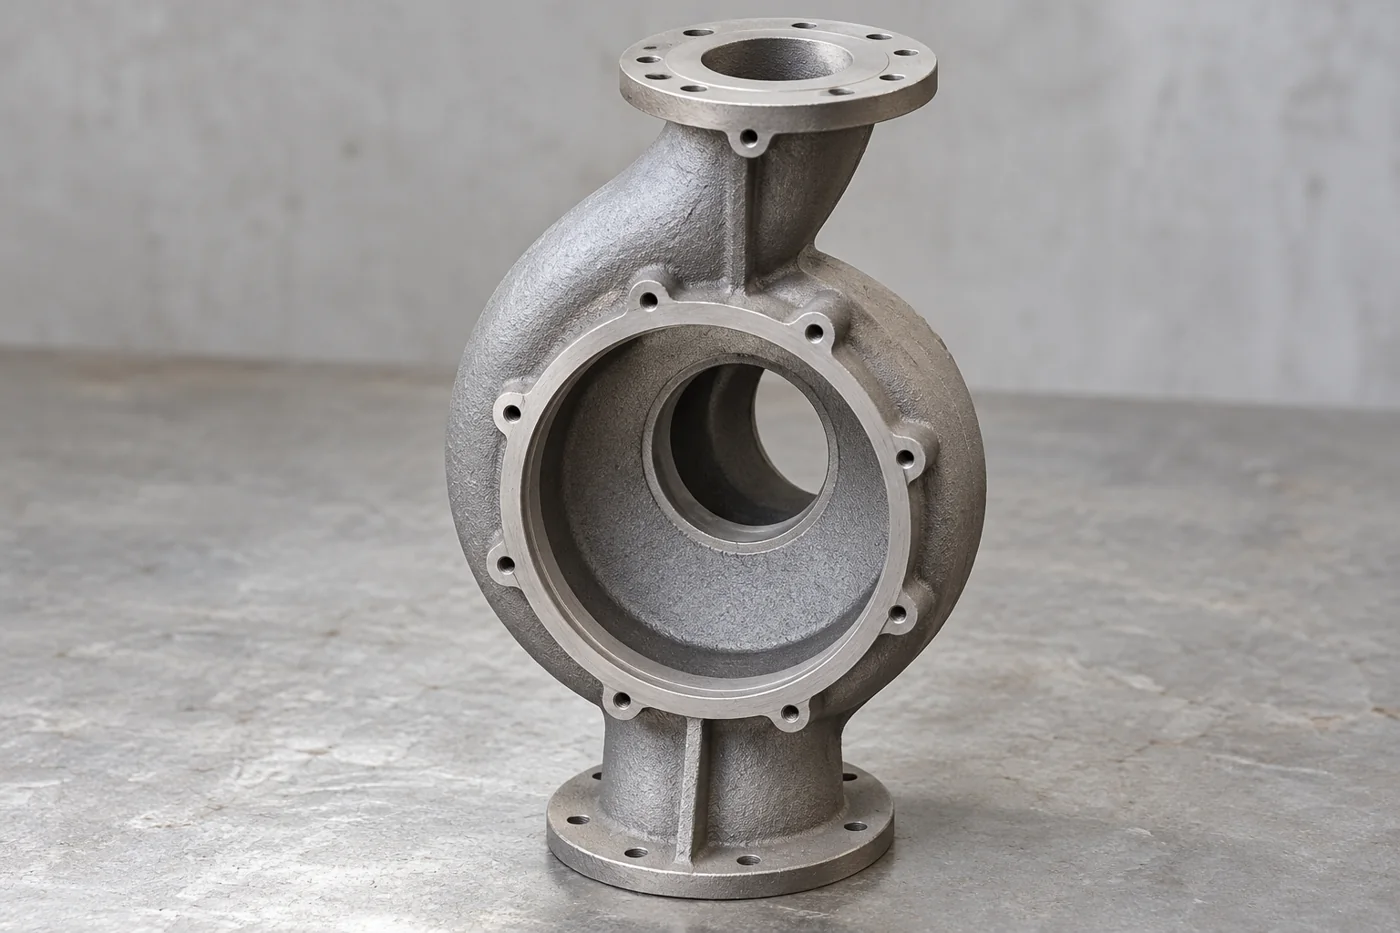
Buy the pump body and its finished sealing interfaces as one component. Relia manufactures sand-cast housings, casings and volutes with selected machining and surface work, including HT200 and HT250 grey-iron options. Define the chamber, register, gasket land and connections together so the sample addresses both the internal flow body and the fit your assembly needs.
- Component
- Housing, casing or volute
- Iron
- HT200 / HT250 options
- Supply
- Cast + selected finishing
02A CLEARER CASTING PURCHASE
Pump bodies and finished connections supplied together
Relia Casting has its own sand-casting and machining production. For pump buyers, we supply drawing-based bodies and volutes, with grey-iron housing routes through sand or shell casting and a separate green-sand pump-body offering. Our main factory route is coated sand or shell moulding, while the actual housing drawing determines the route selected.
This suits a pump OEM buying a new housing and a maintenance supplier replacing a defined casing. You can combine the blank, locating and sealing features, selected finish and dimensional/material reports in the component scope. We can also provide real workshop and equipment photographs when you assess the manufacturing source.
03A CLEARER CASTING PURCHASE
Grey iron and chamber geometry matched to the water duty
Our HT200 and HT250 housing options let you buy a defined grey-iron component rather than a generic pump-shaped blank. Keep the complete grade and delivered condition with the water chemistry, temperature and pressure duty. Ductile iron and steel remain separate material choices when the design needs a different property balance.
The chamber section, tongue region where present and impeller envelope belong to that same design. A shifted core can change the wall and internal clearance even when the outside looks correct. The useful material record and housing measurements therefore describe the selected grade and the actual flow-body geometry together.
| Selection field | Useful purchase-order definition |
|---|---|
| Housing material | HT200 or HT250 with governing material specification |
| Duty input | Water chemistry, temperature and pressure conditions |
| Cast section | Wall thickness and local transitions on the drawing |
| Material record | Required grade evidence linked to supplied batch |
04A CLEARER CASTING PURCHASE
The gasket face and cover register need different controls
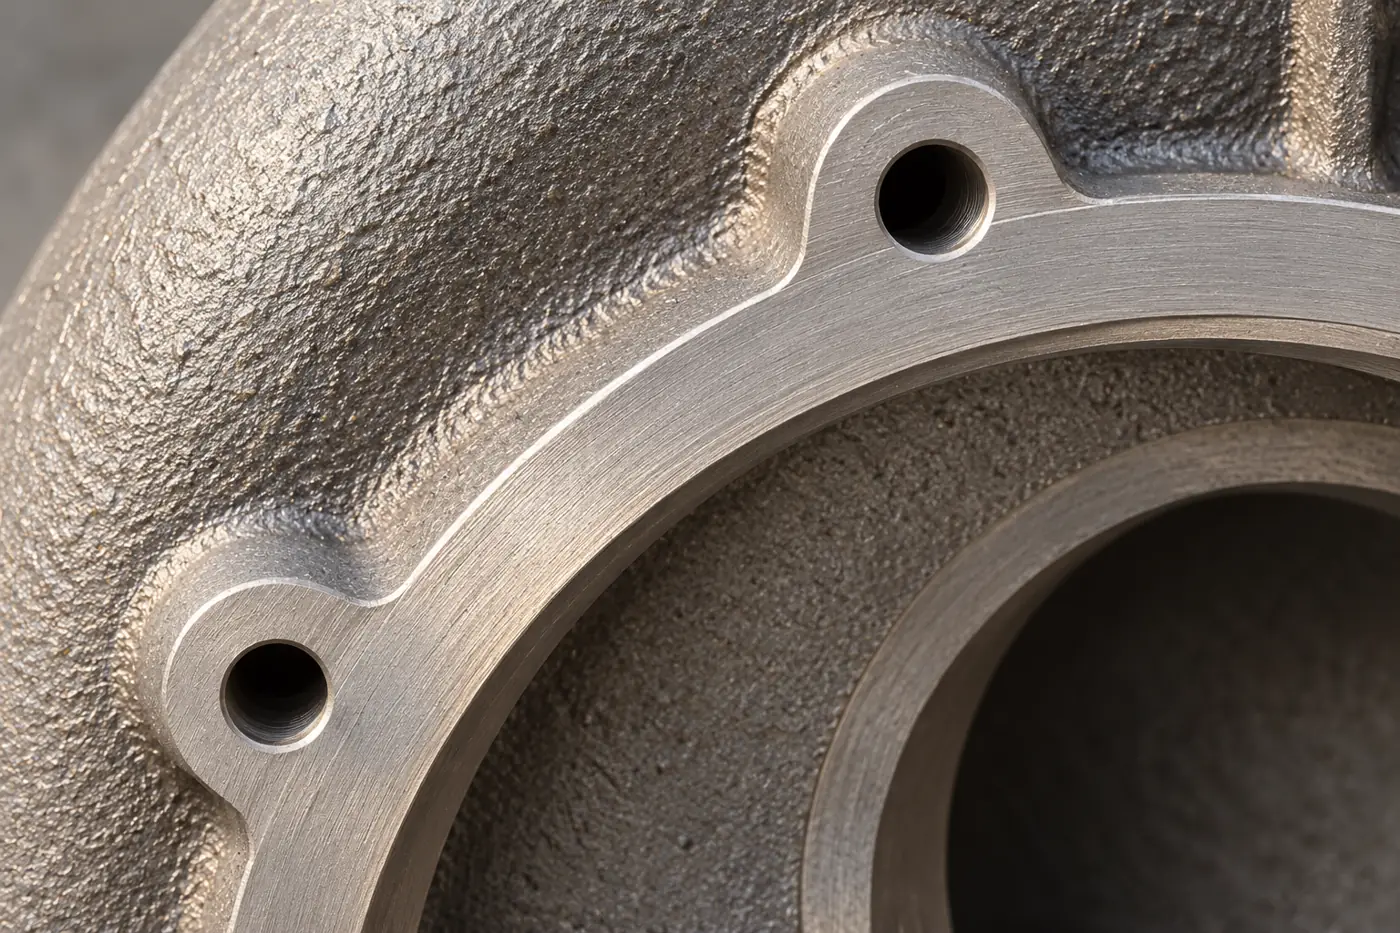
The gasket land needs the surface condition and geometry required by your sealing arrangement. The cover register locates a mating component and needs its own diameter and positional relationship. One surface-roughness note cannot describe both functions.
Mark gasket width, interrupted areas, register depth and the relation to the shaft axis. Keep paint off the specified contact zones. Machining the sealing face successfully still leaves the bolt pattern and locating diameter to be checked against their own drawing references.
- Sealing
- Gasket-land geometry and surface
- Location
- Register diameter and shaft-axis relationship
05A CLEARER CASTING PURCHASE
Mould and core preparation lead to usable machining stock
The housing pattern establishes the outside form and parting arrangement; the core establishes the chamber and passages. Their locating features need to hold those shapes in the same relationship while leaving stock on the cover, nozzle and mounting faces. For a green-sand route, the moulding medium contains sand, clay, water and additives; shell moulding is a separate selected route. The proposed preparation and core-seating checks should suit that choice.
After casting, gate removal and internal cleaning expose the blank for section and stock checks. Machining then creates stable datums before finishing the register, sealing lands and hole pattern. A useful process plan connects each handover to an output: located core geometry, sufficient wall/stock, a cleaned chamber and drawing-related finished measurements. Extra cutting cannot recover a wall that lacks metal.
- 01Form the chamberPattern, parting and core seats establish inside-to-outside location
- 02Check the blankAssess chamber sections and local stock before finish cutting
- 03Create referencesMachine stable mounting and locating datums
- 04Finish the jointRelate register, sealing land and bolt pattern to the pump axis
- 05Release the housingLink final geometry, material evidence and agreed internal condition
06A CLEARER CASTING PURCHASE
Dimensional acceptance and pressure integrity answer different needs
For dimensional acceptance, prioritise the cover register, gasket face, bolt pattern and mounting-plane relationships. For fluid containment, put any required leak or pressure test into a separate test instruction with medium, pressure, hold duration and acceptance criterion. A successful dimensional check does not reveal every leakage path.
Assign the test to the supplied condition: a raw housing, plugged machined casing or assembled pump are different test objects. This lets purchasing compare quotations that include the same preparation, plugs, inspection records and delivered state.
07A CLEARER CASTING PURCHASE
Nozzle orientation and fastener access preserved
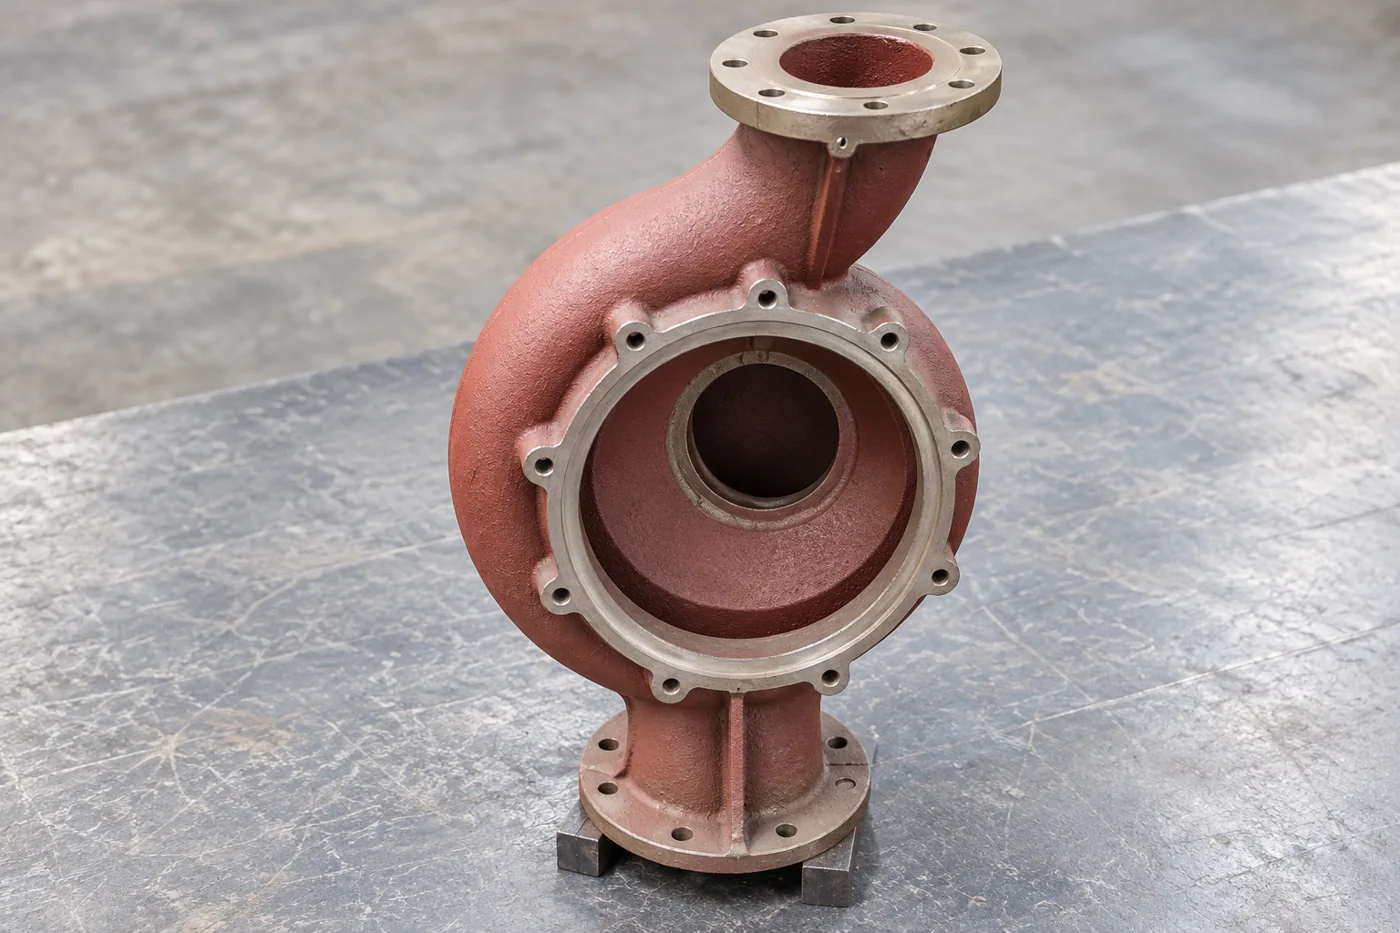
A nozzle can have the correct nominal size yet face the wrong direction for the installation. Dimension its orientation, flange clocking and usable gasket face from the pump's mounting references. Show clearance needed for the adjoining pipe, bolt and tool access.
Where polishing or coating is requested, distinguish internal flow surfaces from external appearance areas. Our listed machining, polishing and coating options can then be allocated to surfaces that benefit from them, while registers and sealing lands retain their specified final condition.
- Connections
- Nozzle clocking and flange access
- Finish
- Selected coating or polishing boundaries
08A CLEARER CASTING PURCHASE
A sample joins factory measurements to the pump assembly
For a new housing, Relia follows drawing review, sample manufacture and inspection, your confirmation, then batch production. The sample report is most useful when its feature map follows the cover register, gasket land, nozzle direction and mounting datums your assembly actually uses. Material results and the agreed internal-condition record should identify that same part.
You then check the released cover and pump installation. A change to a register or nozzle is carried into the accepted housing revision before repeat work. This gives both teams a manufacturing reference that explains the approved assembly, rather than leave a physical sample as the only description of the result.
- 0101Measure register, gasket face and mounting datum relationships
- 0202Verify chamber sections and defined internal-cleaning condition
- 0303Trial the released cover and connection arrangement
- 0404Freeze housing and mating-part revisions for repeat supply
09A CLEARER CASTING PURCHASE
Clean passages and protected sealing lands at receipt
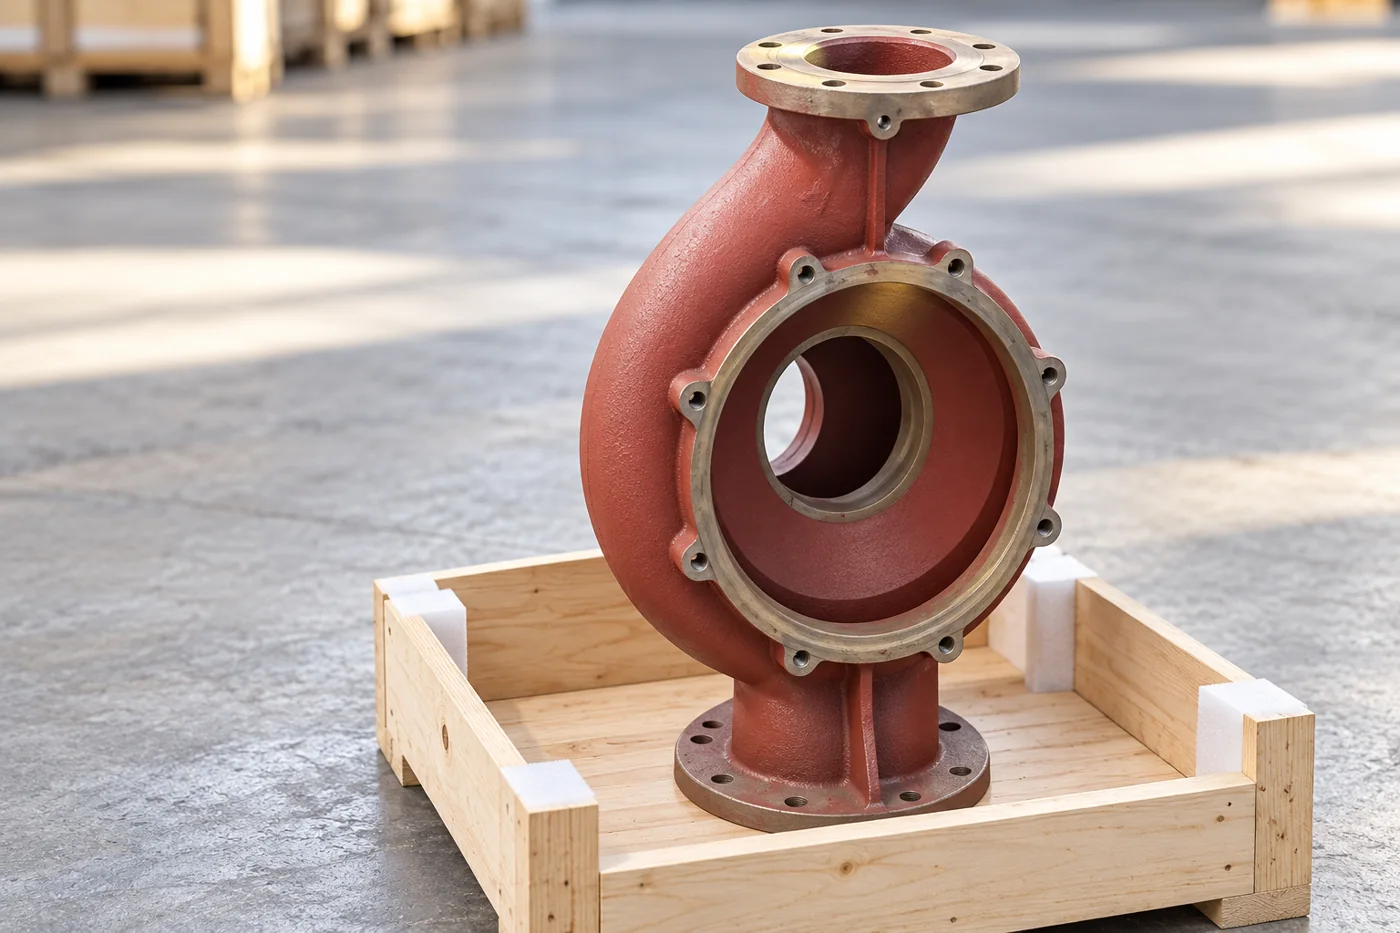
Internal preparation belongs before final protection and packing. Specify removal of core residues, loose shot, machining chips and burrs from accessible passages; then define the cleanliness evidence needed for your pump assembly. Coating should not conceal unaccepted cast surfaces.
Wooden-case packing is offered for these castings. Protect machined gasket lands and registers from contact damage, cover openings after cleaning and identify the housing revision. Your receiving team can then inspect the same functional features used for sample approval.
- Internal state
- Cleaning before openings are covered
- Protection
- Wooden-case scope and protected joint faces
10A CLEARER CASTING PURCHASE
An assembly package with clear release evidence
A useful housing purchase brings three outputs together: the correct cast flow body, finished interfaces for your assembly and records that explain the supplied part. Relia can connect casting, machining and selected surface work around that outcome. You can keep further machining at your plant or include the nominated interfaces in our supply.
The practical starting pack is the chamber model, finished drawing, iron requirement and quantities, with the joint and mounting features highlighted. We can then discuss the sample and supplied state directly. Your comparison remains focused on a usable housing and the work remaining at your next operation.
11 YOUR NEXT STEP
Bring your component into the conversation
Tell us which component you need, the material, quantity and required supplied condition. Relia will connect your enquiry with the casting, machining and evidence relevant to that part.
Technical reading and scope
Technical references explain the process. Component specifications and agreed order records define the actual supply.
Volute casing geometry and pump arrangementsISO 8062-3 — casting tolerances and machining allowancesGreen-sand moulding medium — AFS- [email protected]
- Phone
- +86 18561762631
- +1 404 203 0971
- Company and address
- Qingdao Relia Industries Co., Ltd.
Shuyuan Road, Qingdao, Shandong, China