Custom Gray Ductile Iron Sand Cast Pump Bodies Gearbox Machinery Housings Counterweights with ISO 8062 Tolerance
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
Size50 - 1200 mm,
-
Surface TreatmentShot Blasting, Primer Painting, Powder CoatingMaterialsHT200 HT250 HT300 Gray Iron, QT450 Ductile Iron
-
Casting ProcessGreen Sand Casting and Resin Sand CastingMaterial GradeHT200, HT250, HT300, QT450-10, QT500-7
-
Casting Weight Range0.5 - 500 kgDimensional ToleranceCT9 - CT11 per ISO 8062
-
Tensile Strength200 - 500 MPa by GradeHardnessHB 170 - 241
-
Wall ThicknessMinimum 5 mmPattern MakingWood, Resin and Aluminum Pattern
-
TestingSpectrometer, Tensile Test, UT Flaw DetectionApplicationPump Body, Gearbox Housing, Counterweight
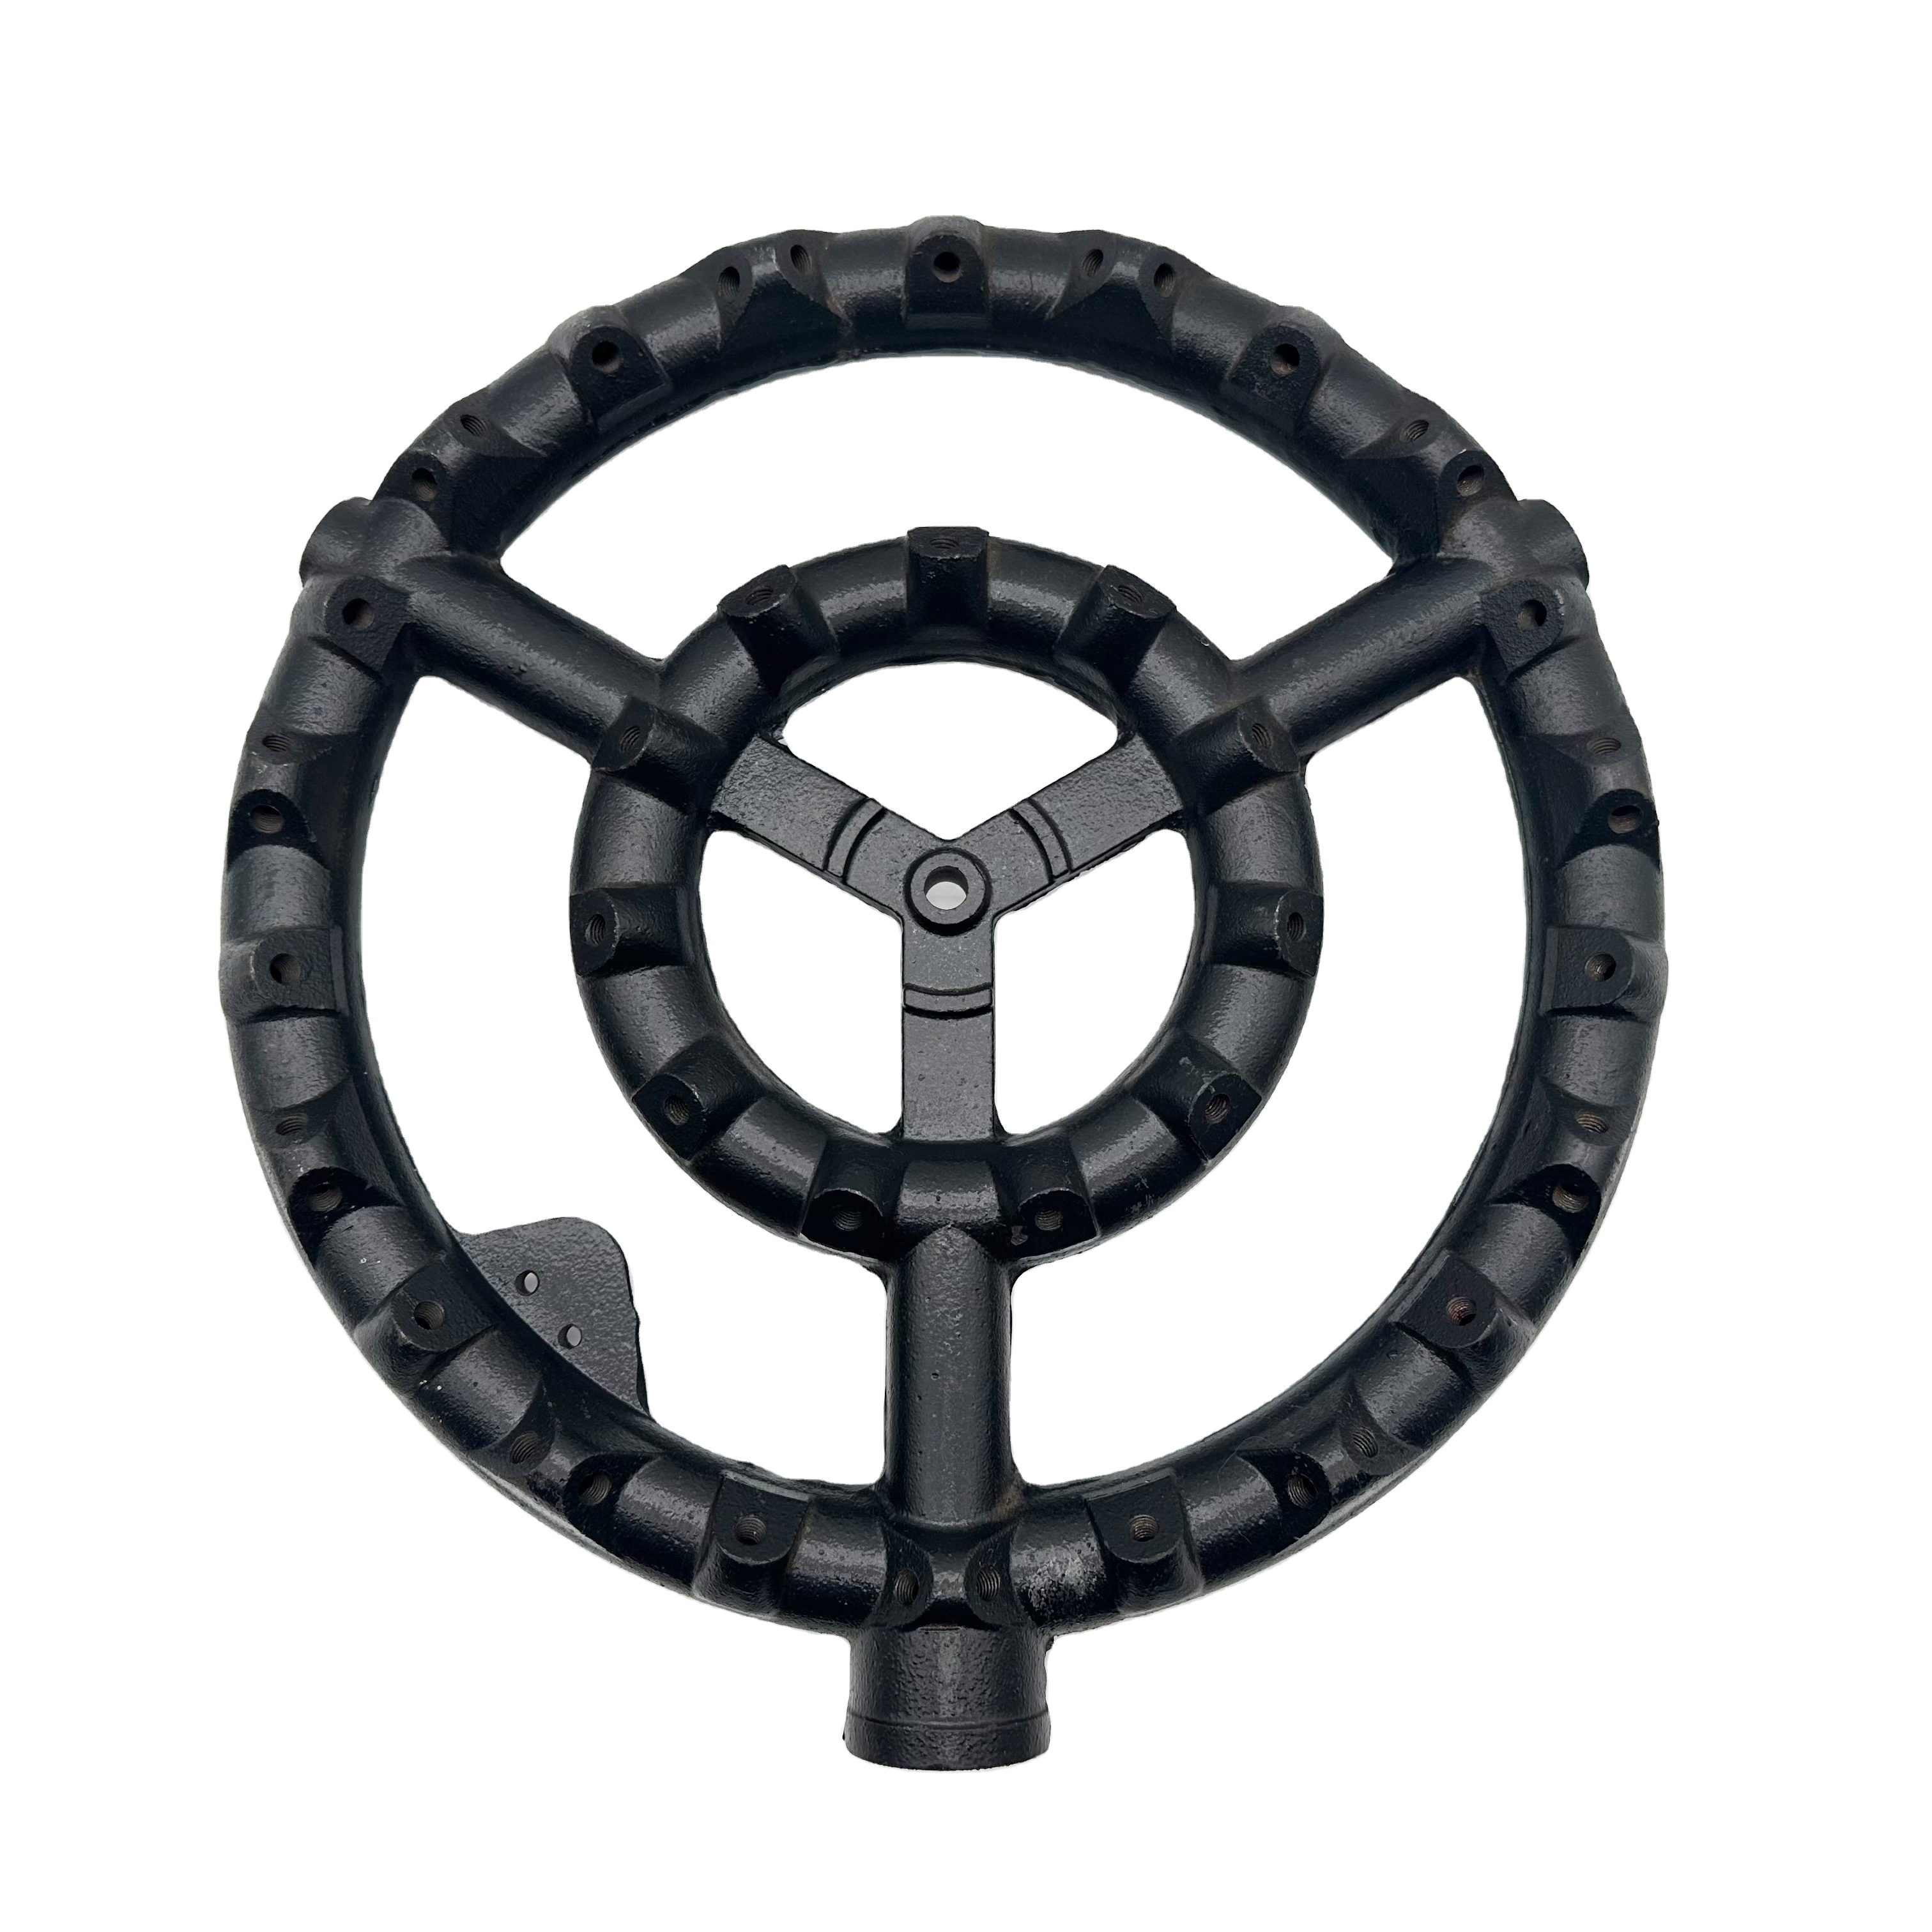
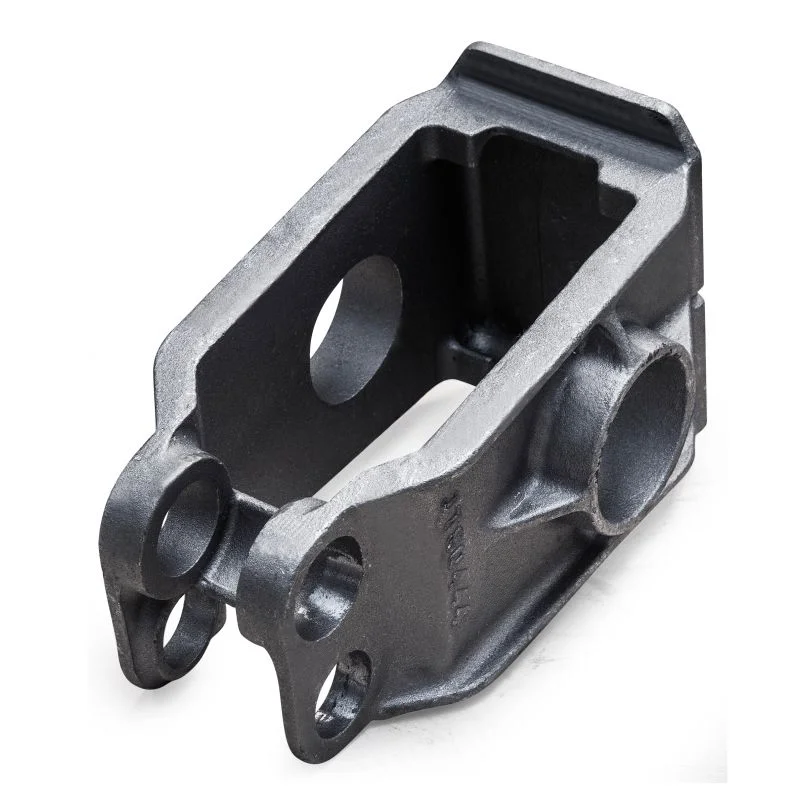
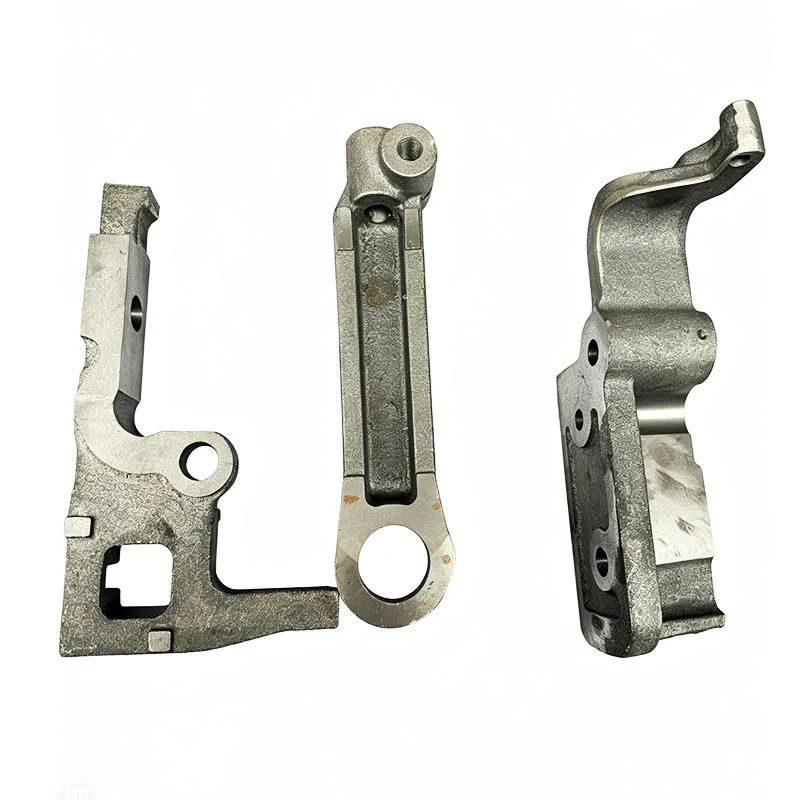
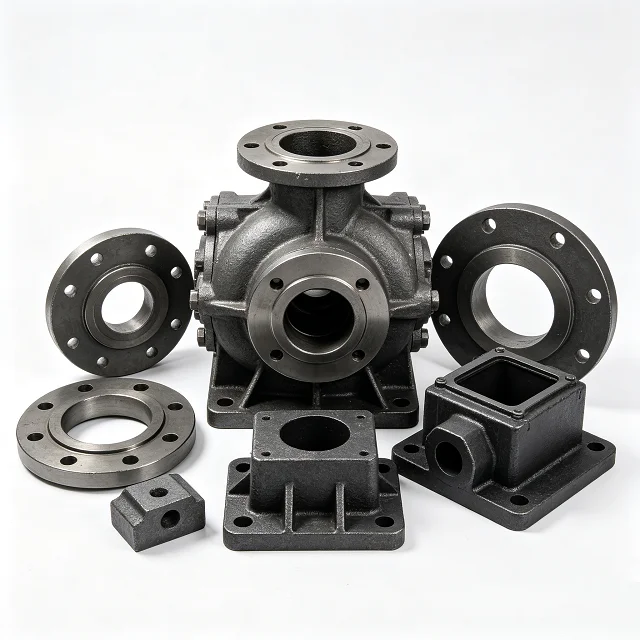
Custom sand castings serve pump bodies, gearbox or machinery housings and counterweights. Material selections are HT200, HT250, HT300, QT450-10 or QT500-7. Choose the grade and green- or resin-sand route for the actual component drawing and required delivered condition.
Match dimensions and properties to the selected grade
The size reference is 50–1200 mm, with a minimum wall-thickness reference of 5 mm to be checked against the geometry. Dimensional tolerance is CT9–CT11 per ISO 8062. Define the controlled dimensions and measurement basis for the part’s mounting, locating and mating areas.
Property references are tensile strength 200–500 MPa by grade and hardness HB170–241. Specify the actual values and test requirements for the chosen iron, rather than using the full range as one material definition.
Choose pattern and surface requirements
Wood, resin and aluminum patterns are available. Identify the pattern deliverable and controlled geometry needed for the selected molding request. Finish choices include shot blasting, primer painting and powder coating; mark coverage or masking around functional surfaces and define visual acceptance.
Set the inspection and approval records
Testing references include spectrometer analysis, tensile testing and UT flaw detection. Agree the selected methods, coverage and acceptance limits for the pump body, housing or counterweight being ordered. Provide quantity and the controlled revision with the material and surface requirements, keeping sample and production approval tied to the same component definition.