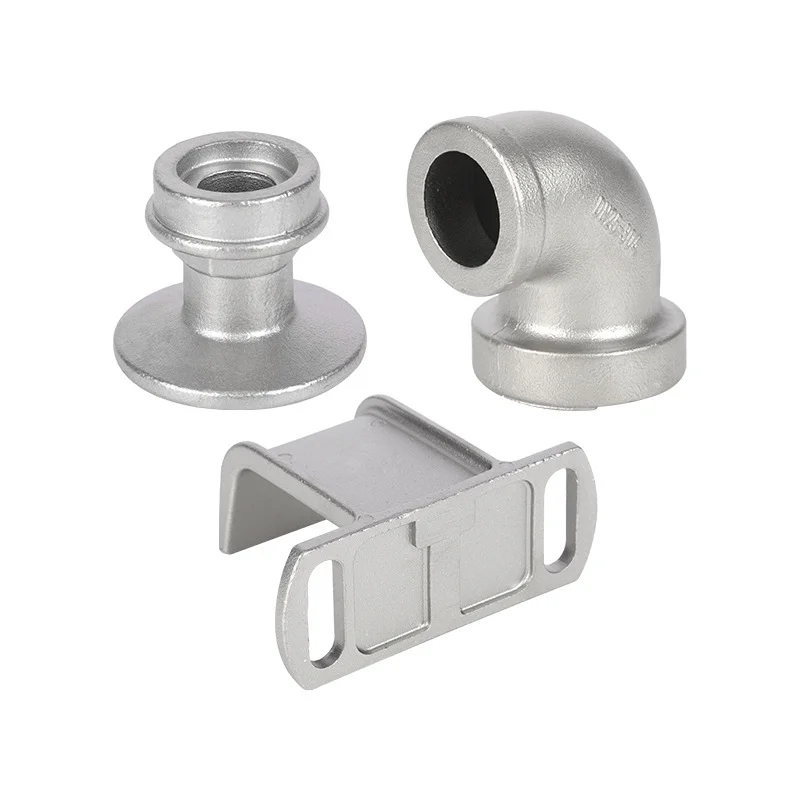
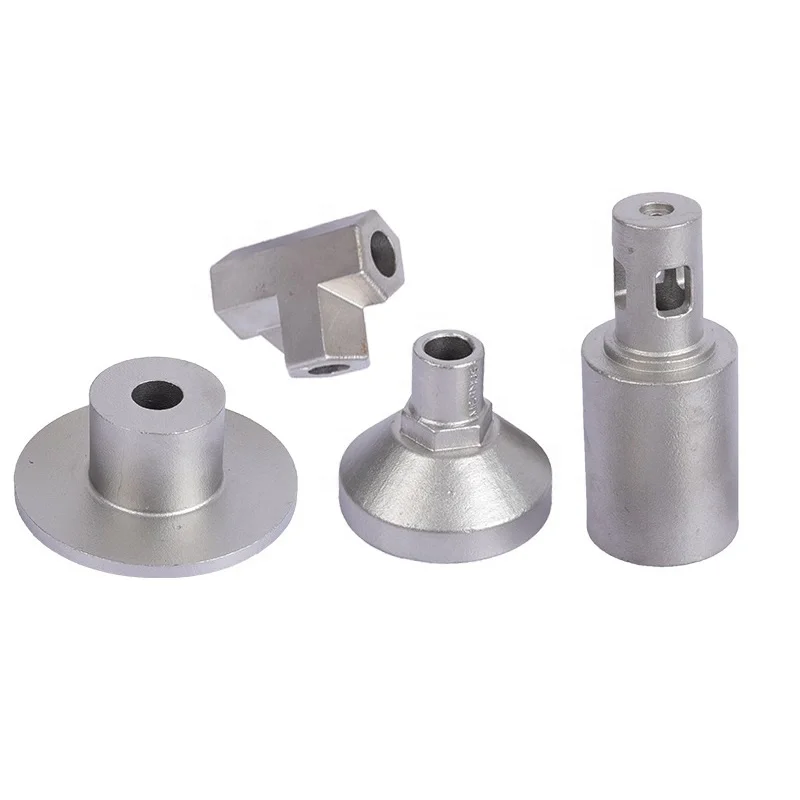
Custom Aluminum or Stainless Steel Storz Fire Hose Coupling Adapters and Caps with Silica Sol or Sand Casting
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
Casting ProcessLost Wax Investment Casting, Silica Sol, Medium Temperature Wax
-
Precision GradeCT5--CT12, ±0.05--0.5 mm (By Size)CertificationISO9001, Material Traceability (COC), PPAP Supported
-
Surface FinishRa 1.6 - 3.2 Micro (As Cast), Electro-polishing ServiceHeat TreatmentQuenching & Tempering, Normalizing, Annealing
-
Testing ServiceCMM Inspection, Material Spectral Report, PT/MT/NDTSecondary ProcessCNC Machining In-House, Polishing, Assembly
-
Sample Lead TimeDFM Review 72 Hours, Samples 5--10 DaysTypical ApplicationPump Impeller, Valve Body, Marine Hardware, Food/Medical Parts
-
Supplier TypeOEM/ODM Custom Manufacturing Factory with Design Support
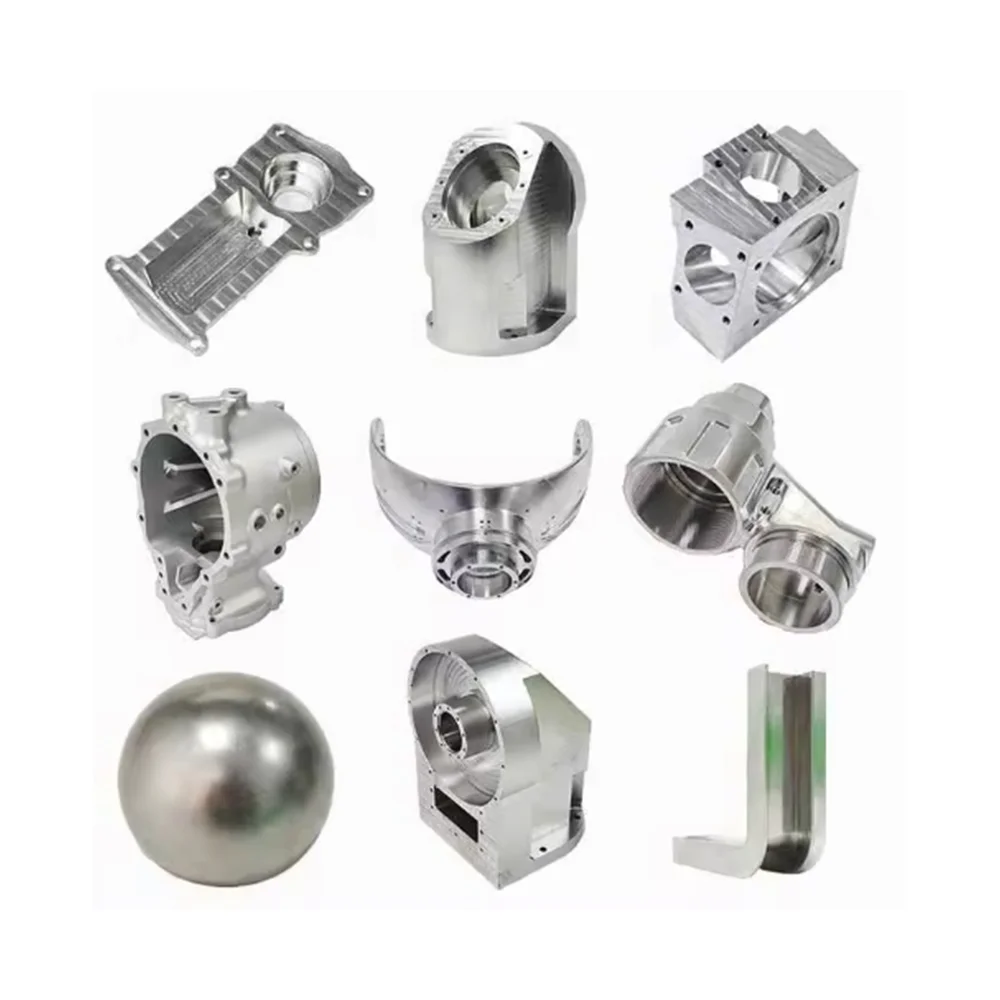
Custom Storz fire-hose couplings, adapters and caps can be requested in aluminum or stainless steel. OEM and ODM manufacturing includes design support. Lost-wax investment casting uses silica sol and medium-temperature wax, with sand casting as another enquiry route for a suitably defined fitting.
Define the fitting and service conditions
Specify the actual material grade, connection interfaces and operating duty. Identify the fire-hose assembly and any required pressure, sealing or application approvals. Broader applications include pump impellers, valve bodies, marine hardware and food or medical parts, each requiring its own component definition and acceptance scope.
Allocate dimensional and surface requirements
Precision references are CT5–CT12 and ±0.05–0.5 mm by size. Agree the controlled features and applicable manufacturing stage. For the as-cast Ra1.6–3.2 Micro requirement, define the unit convention and surfaces to be assessed. Electropolishing is offered as a separate surface service.
Select processing and testing
Heat-treatment options include quenching and tempering, normalizing and annealing where appropriate for the selected metal. Secondary services include in-house CNC machining, polishing and assembly. Testing services cover CMM inspection, a material spectral report and PT, MT or other NDT selected for the alloy and component.
Agree traceability and approval records
ISO 9001, material-traceability COC and PPAP support are listed references. Establish the relevant documents and scope for the ordered fitting. Supply the controlled drawing, quantity and initial approval requirements, keeping any design change linked to the selected material, interfaces and agreed inspection plan.