HT200 HT250 Grey-Iron Bearing Blanks and Sand Castings — Custom CNC Lathe Turning and Ductile-Iron Enquiries
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
Sizecustom
-
Surface TreatmentAs CastMaterialsGray Iron
-
Machining TypeCNC Lathe Machining Center Turning Parts Processing Copper Parts ProceDimensional Accuracy±0.01mm
-
Processable Materialsductile iron casting ,grey castingMaximum Machining SizeConsult Customer Service
-
Supports Custom ToleranceSupports Custom ToleranceMachinable Surface RoughnessConsult Customer Service
-
Sample Lead Time8-15 daysProcessing Time7 days
-
BrandRelia
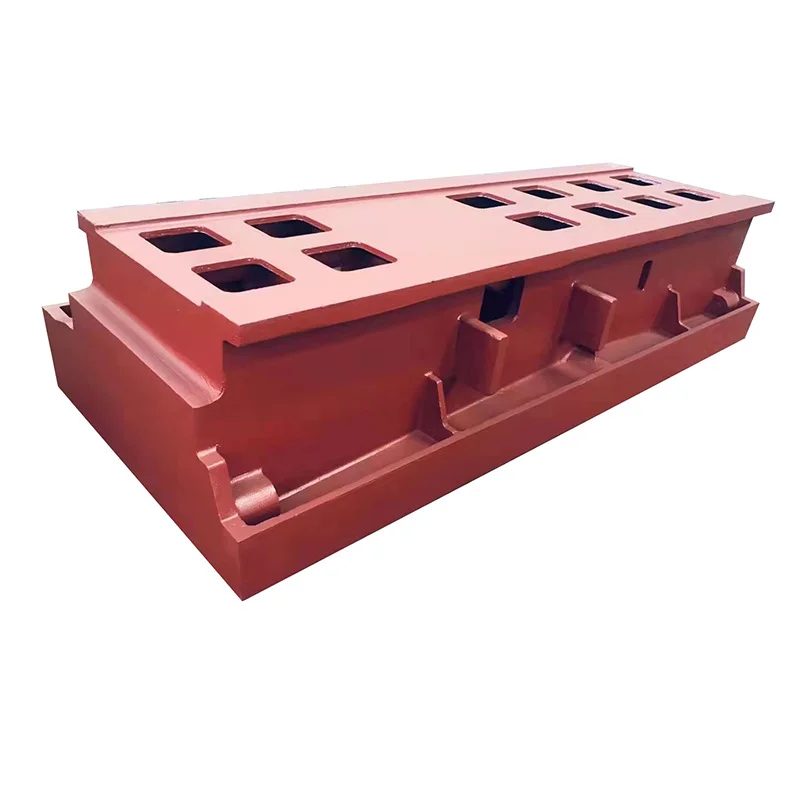
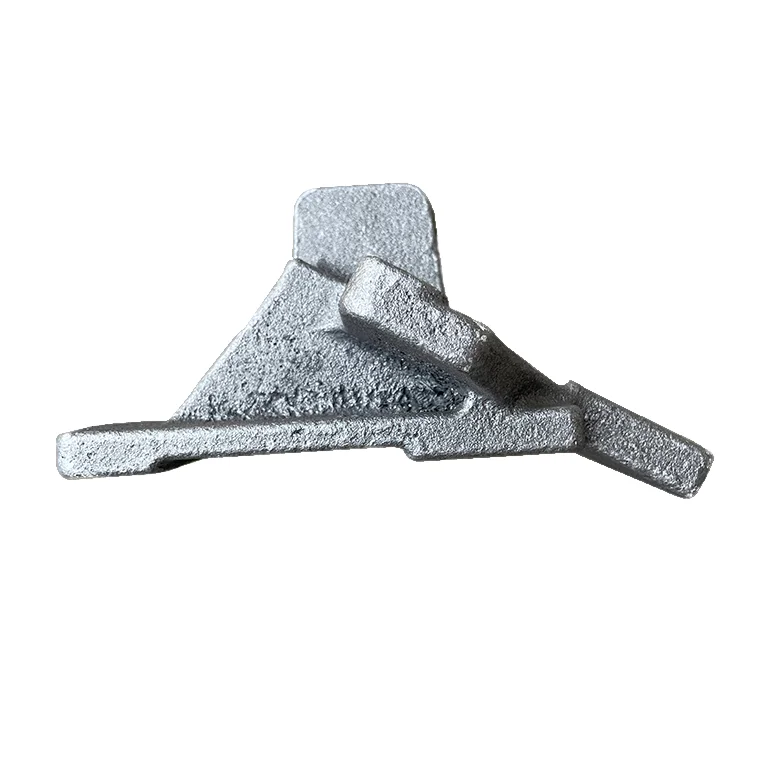
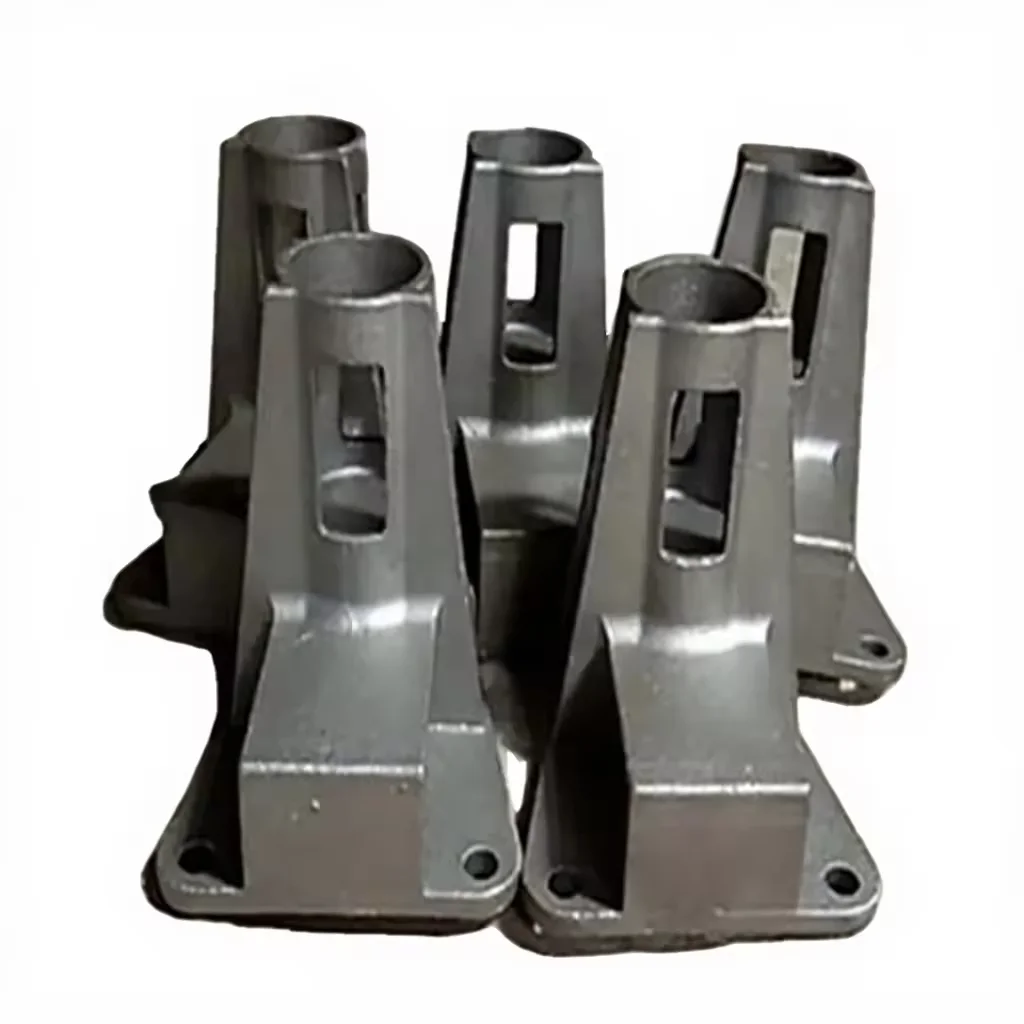
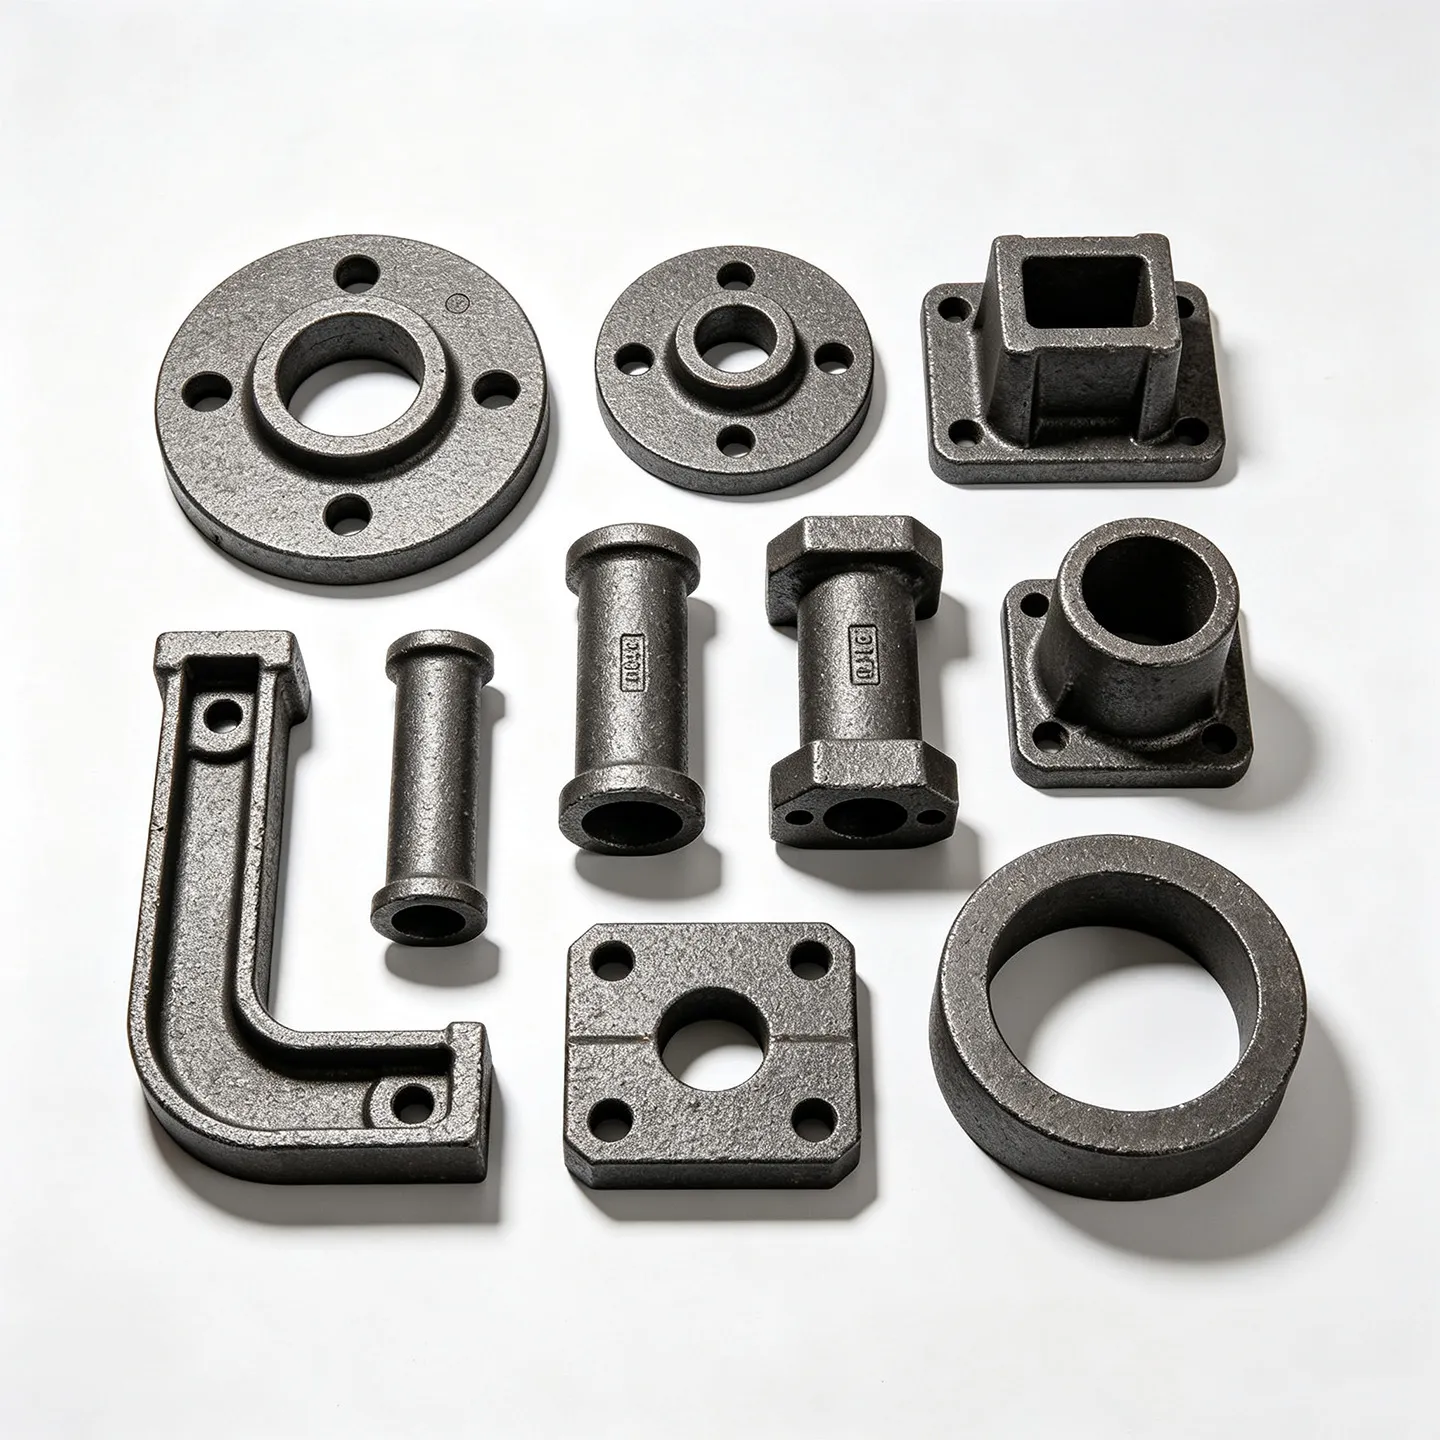
HT200 and HT250 grey-iron bearing blanks are offered through custom sand-casting enquiries, with an as-cast surface condition and optional machining work. Ductile-iron components can be requested as a separate grade selection for the actual drawing and assembly requirement.
Define the blank and the finished bearing interfaces
Provide the bearing-blank geometry and identify the bores, mating faces and locating surfaces that require machining. Specify HT200 or HT250 grey iron, or the complete separately selected ductile-iron grade. The distinction between the supplied blank and its finished interfaces helps establish what the ordered component must include.
Apply accuracy requirements at the machining stage
CNC lathe, machining-center and turning enquiries are named. The dimensional-accuracy reference is ±0.01 mm, with custom tolerance supported. Assign the required limits to agreed dimensions and inspection stages; discuss the maximum machining size and required machined roughness against the actual component drawing.
- Supply the blank drawing and selected iron grade.
- Mark bores, datums and finished mating interfaces.
- Specify tolerances and the required roughness parameter.
- Identify as-cast surfaces and optional machining work.
- State quantity and component-acceptance requirements.
Keep the ordered material and supply condition clear
Copper-part processing is a separate machining enquiry and should have its own drawing and material brief. For the bearing blank, keep the iron grade, as-cast condition and any agreed machining in one controlled order definition. State the assembly duty and acceptance criteria needed by the design, including any performance checks required for that specific component.