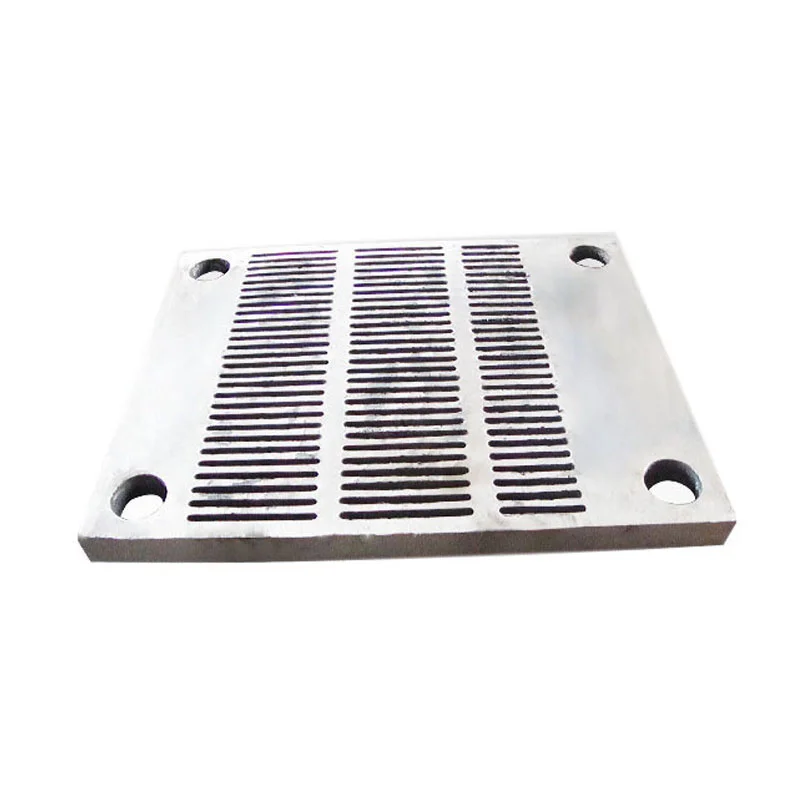
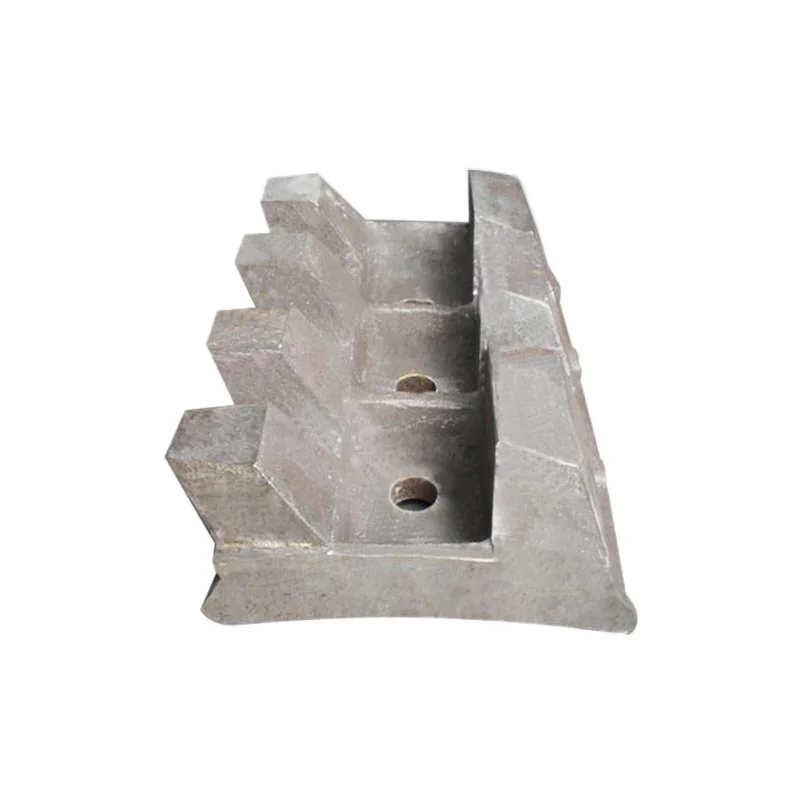
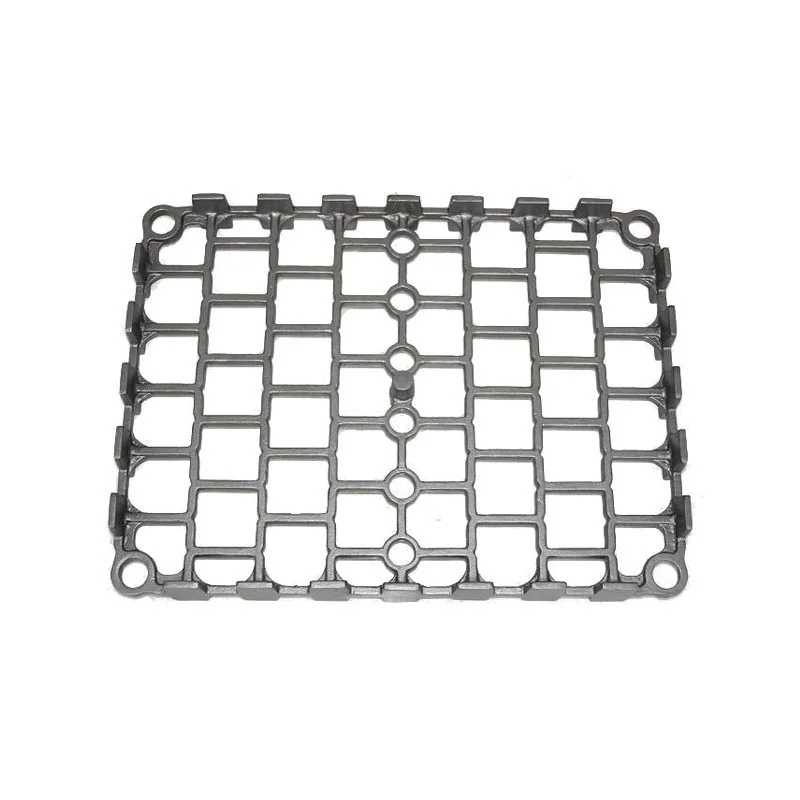
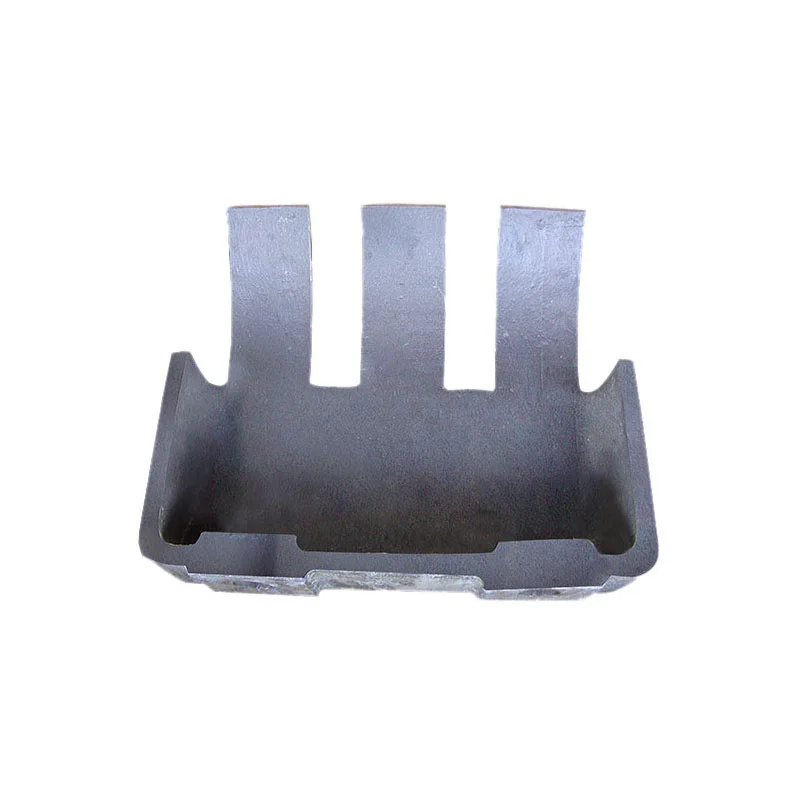
Custom A356 Aluminum Brass Stainless Steel Grey Iron Sandguss Sand Casting Parts and Investment Casting
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
MaterialStainless Steel,Steel,Brass,Copper,Aluminum,Iron,Plastic
-
TechnologyInvestment Casting,Sand Casting,Machining,Welding,ForgingMachiningBroaching,DRILLING,Milling,Turning,Tapping,Wire
-
ProcessMolds,Casting,Deburring,Machining,Surface Treatment,PackingWeightAvailable from 0.01 Kg-10T
-
StandardISO,GB,DIN,JIS,ANSI,BSW,ASTM,ASME,BS,API,ENCasting ToleranceCT4-CT8
-
Machining Tolerance+/-0.02mmSurface TreatmentPolishing, Passivating, Sandblasting, Zinc plating, Oxide black
-
CertificationIS09001: 2015,TUV
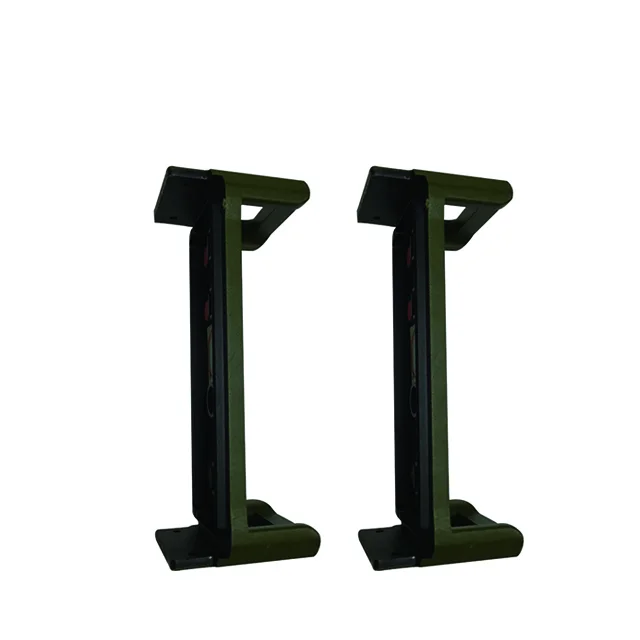
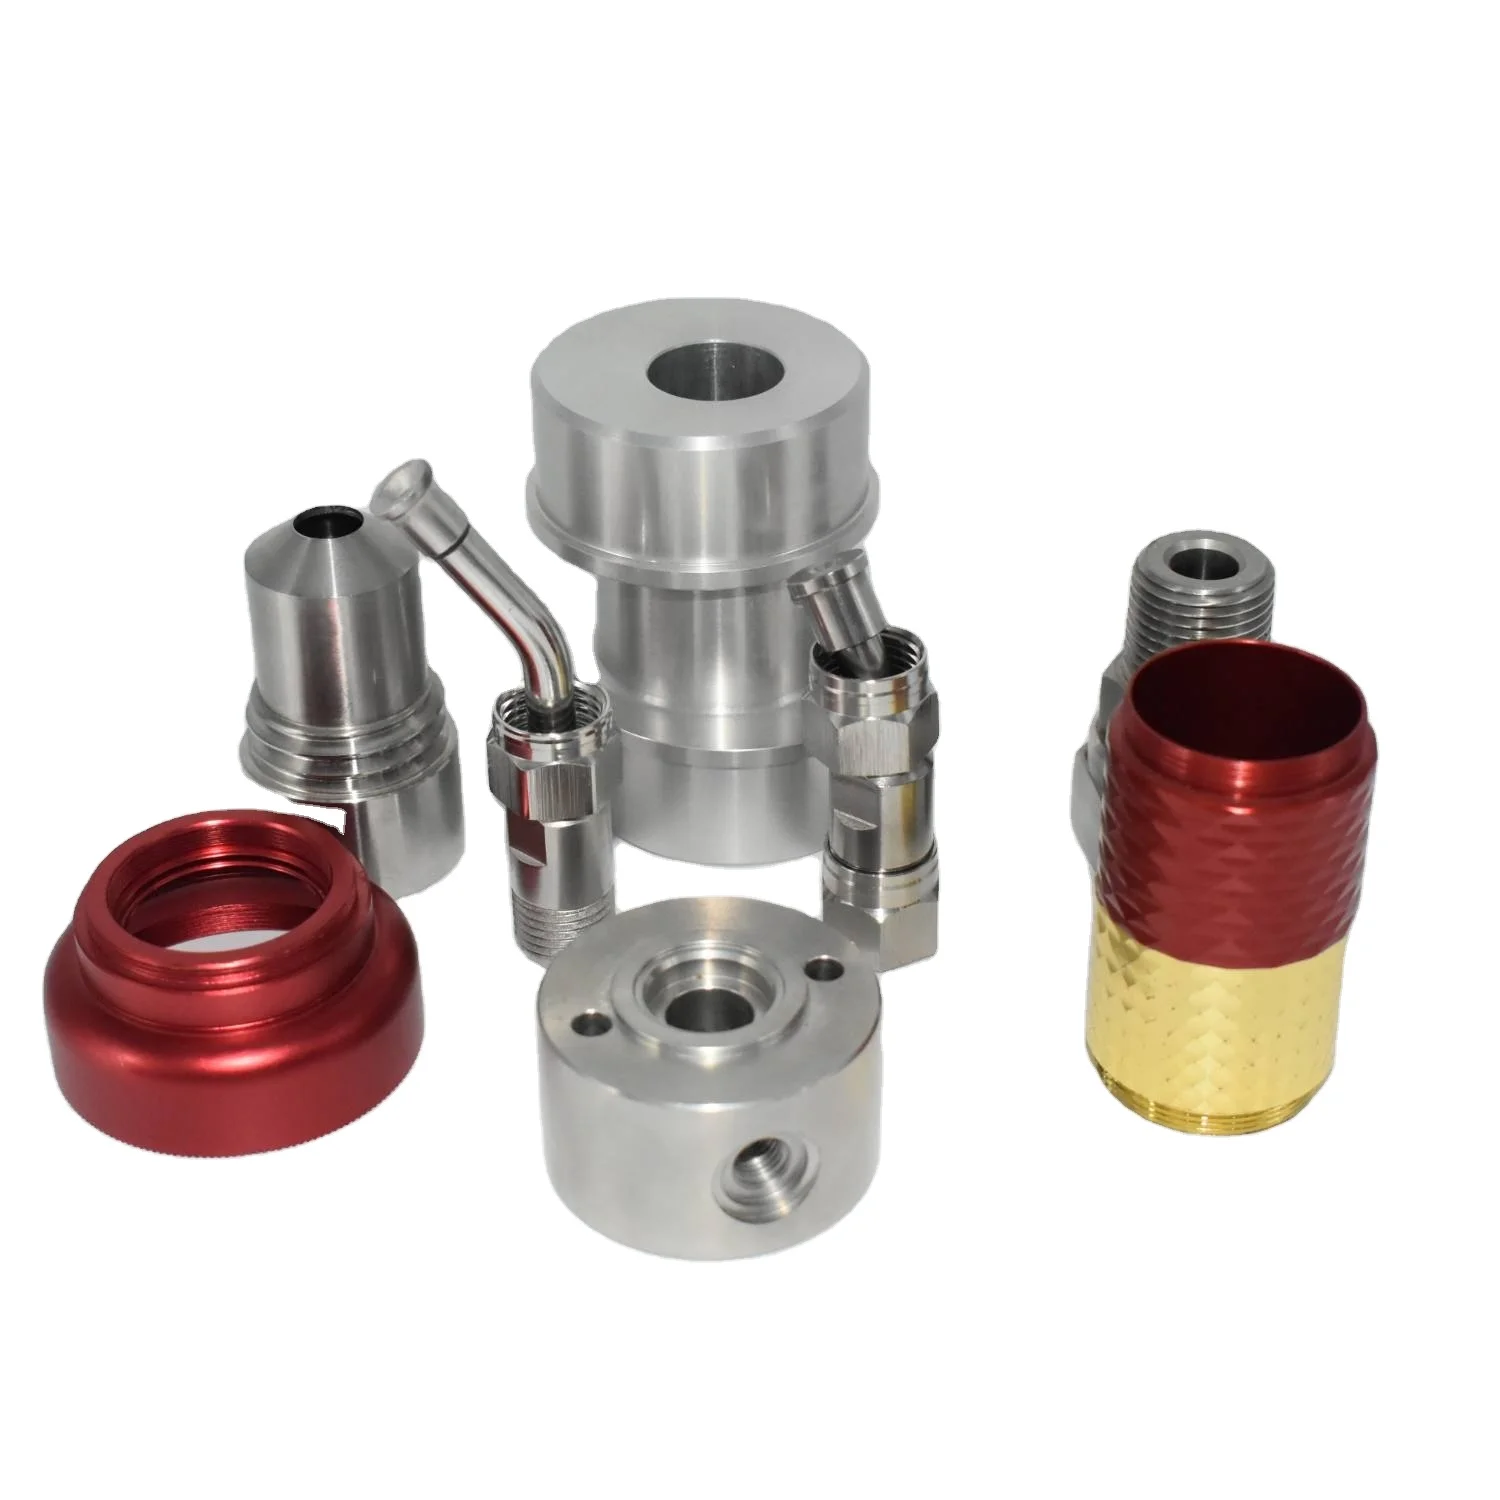
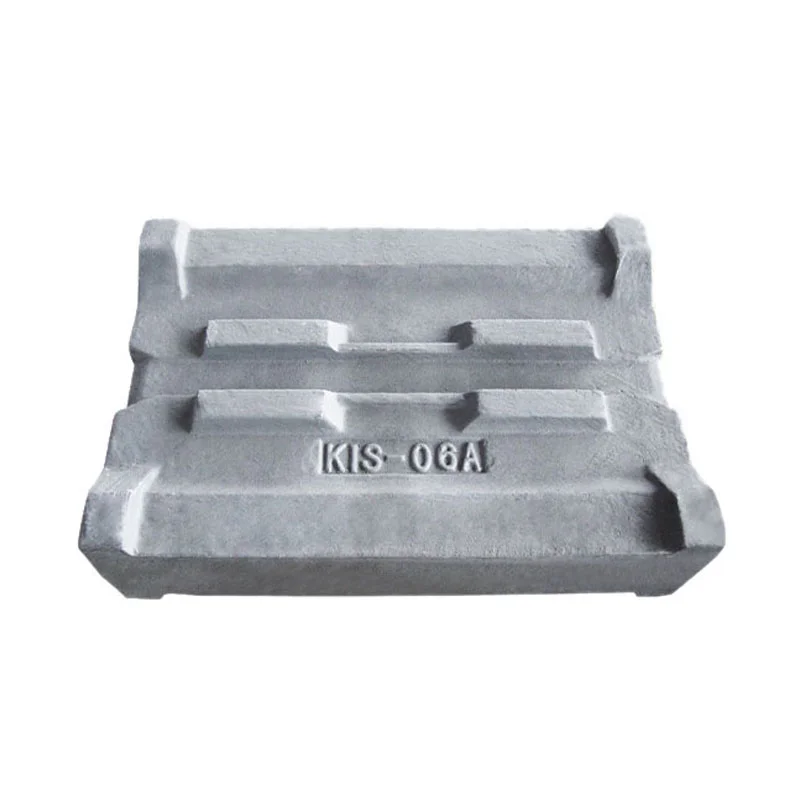
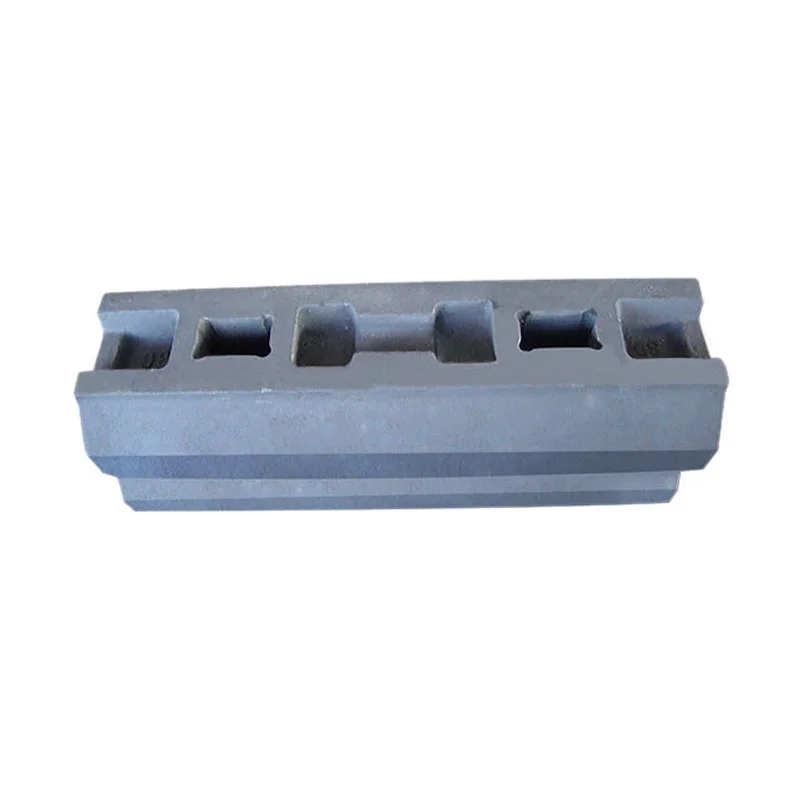
Custom sandguss and sand-casting enquiries include A356 aluminum, brass, stainless steel and grey iron, with additional steel, copper and plastic component requests. Investment casting, machining, welding and forging are named service routes. Choose a suitable material and process for each item rather than combining every route into one production sequence.
Build the enquiry around the component geometry
Identify the finished interfaces and any areas where the cast form remains visible. The casting-tolerance reference is CT4–CT8, while machining tolerance is stated as ±0.02 mm. Assign these references to agreed dimensions and delivery stages so that the inspection basis reflects the actual work being ordered.
Select the operations required by the drawing
The machining scope offers several ways to create the finished geometry. Use the drawing to identify which operations are needed and what their acceptance points are.
- Broaching for the specified internal or external profile.
- Drilling and tapping for the marked hole and thread requirements.
- Milling for the designated faces or pockets.
- Turning for the selected rotational geometry.
- Wire processing, with the actual wire method identified in the enquiry.
Close the finish and document requirements
Supply scope includes molds, casting, deburring, machining, surface treatment and packing as applicable to the selected part. Finish choices include polishing, passivation, sandblasting, zinc plating and black oxidation. Name the required standard and edition from the stated standard families, and identify the relevant ISO9001-related or TUV qualification document and scope. Include quantity, material acceptance and the inspection record needed for approval of the finished component.