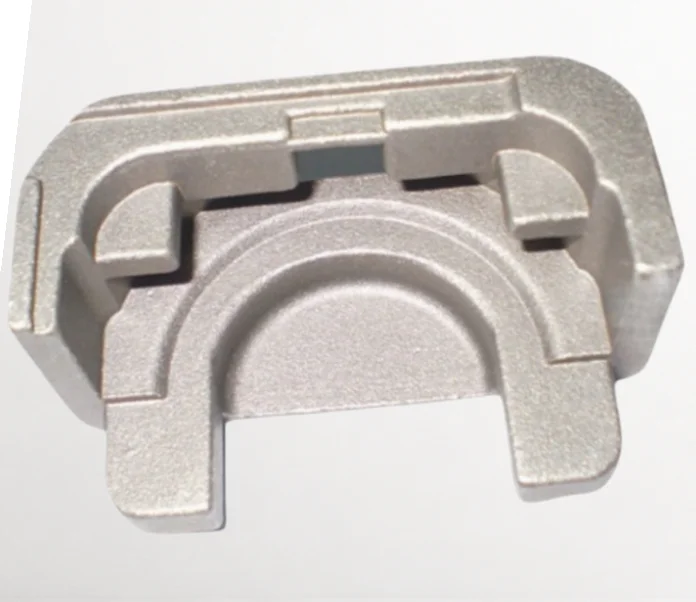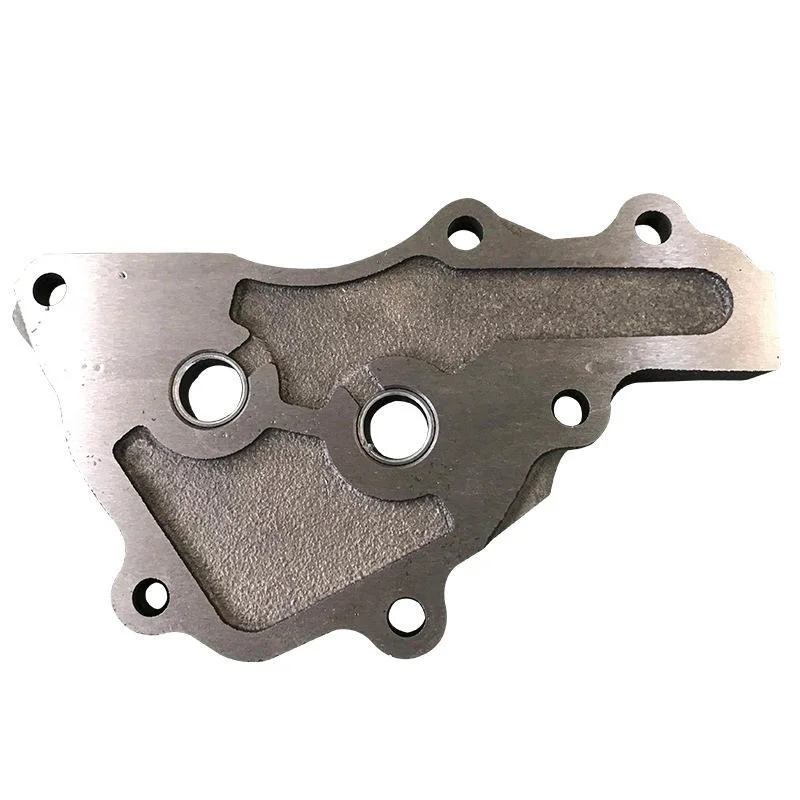
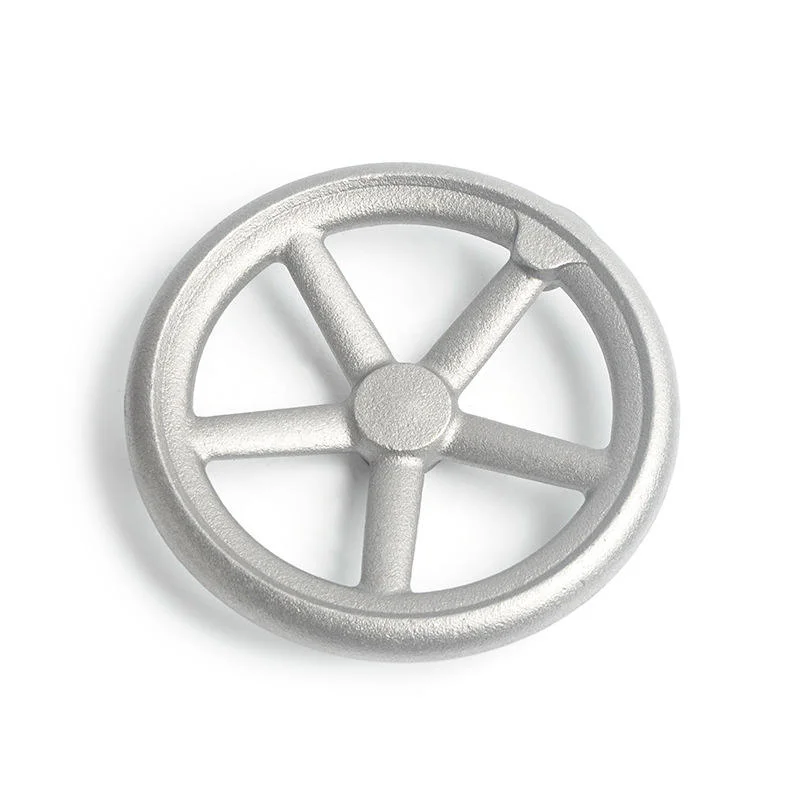
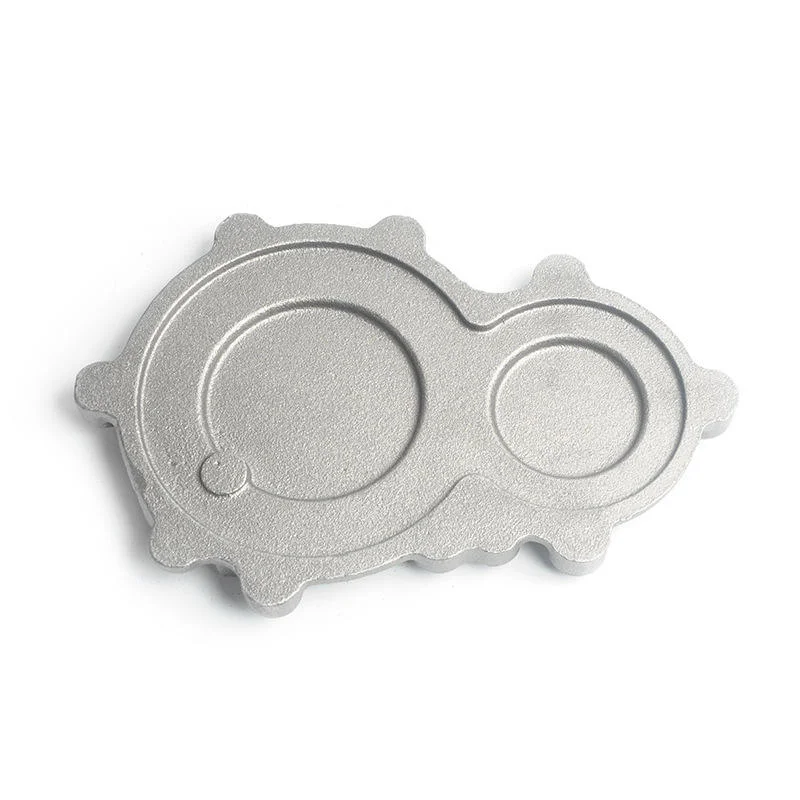
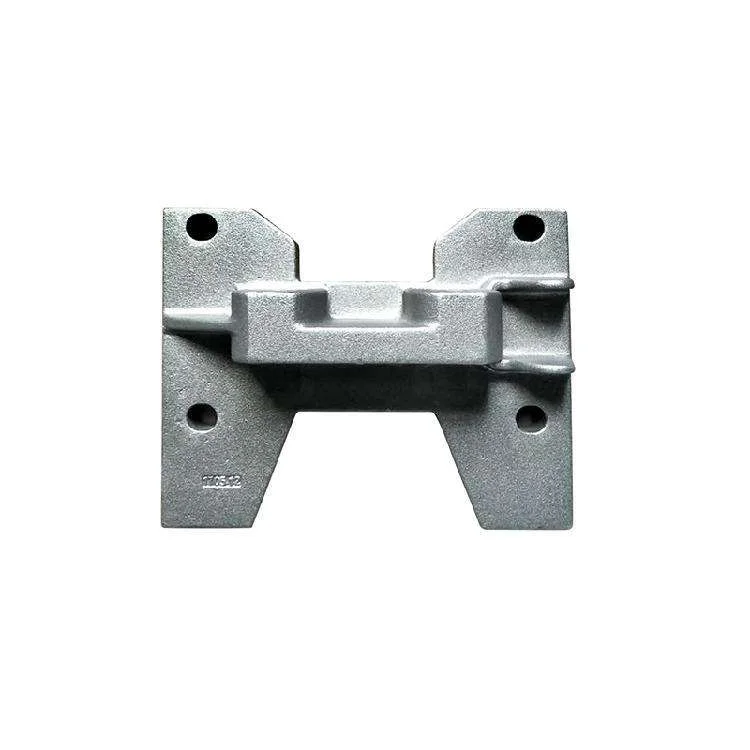
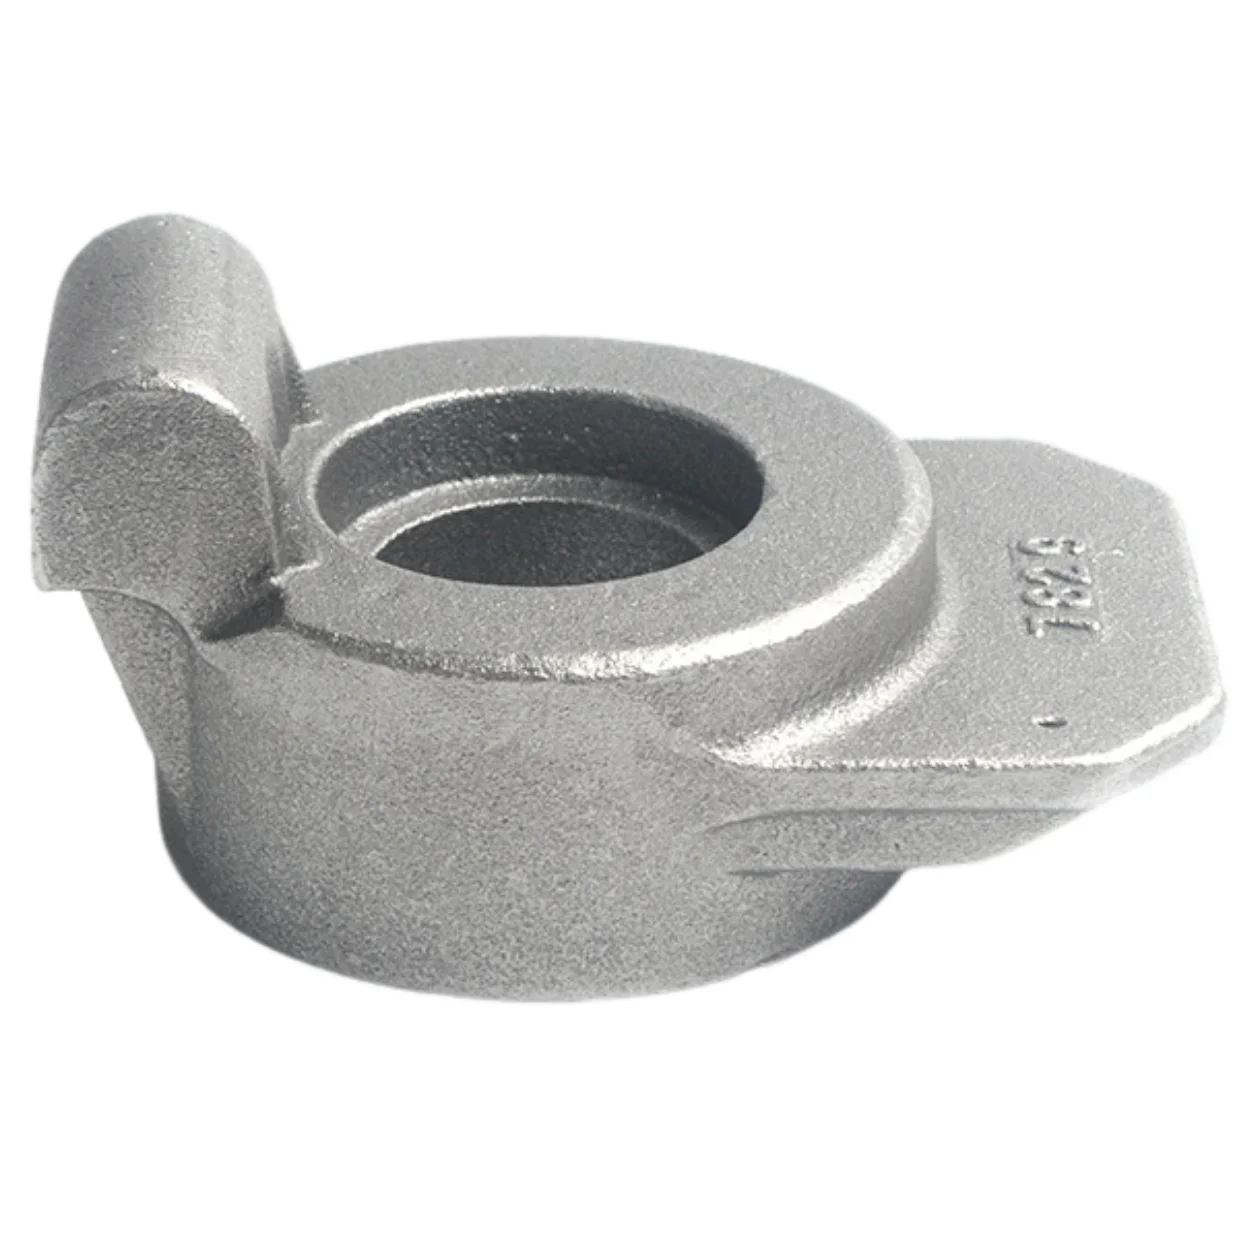
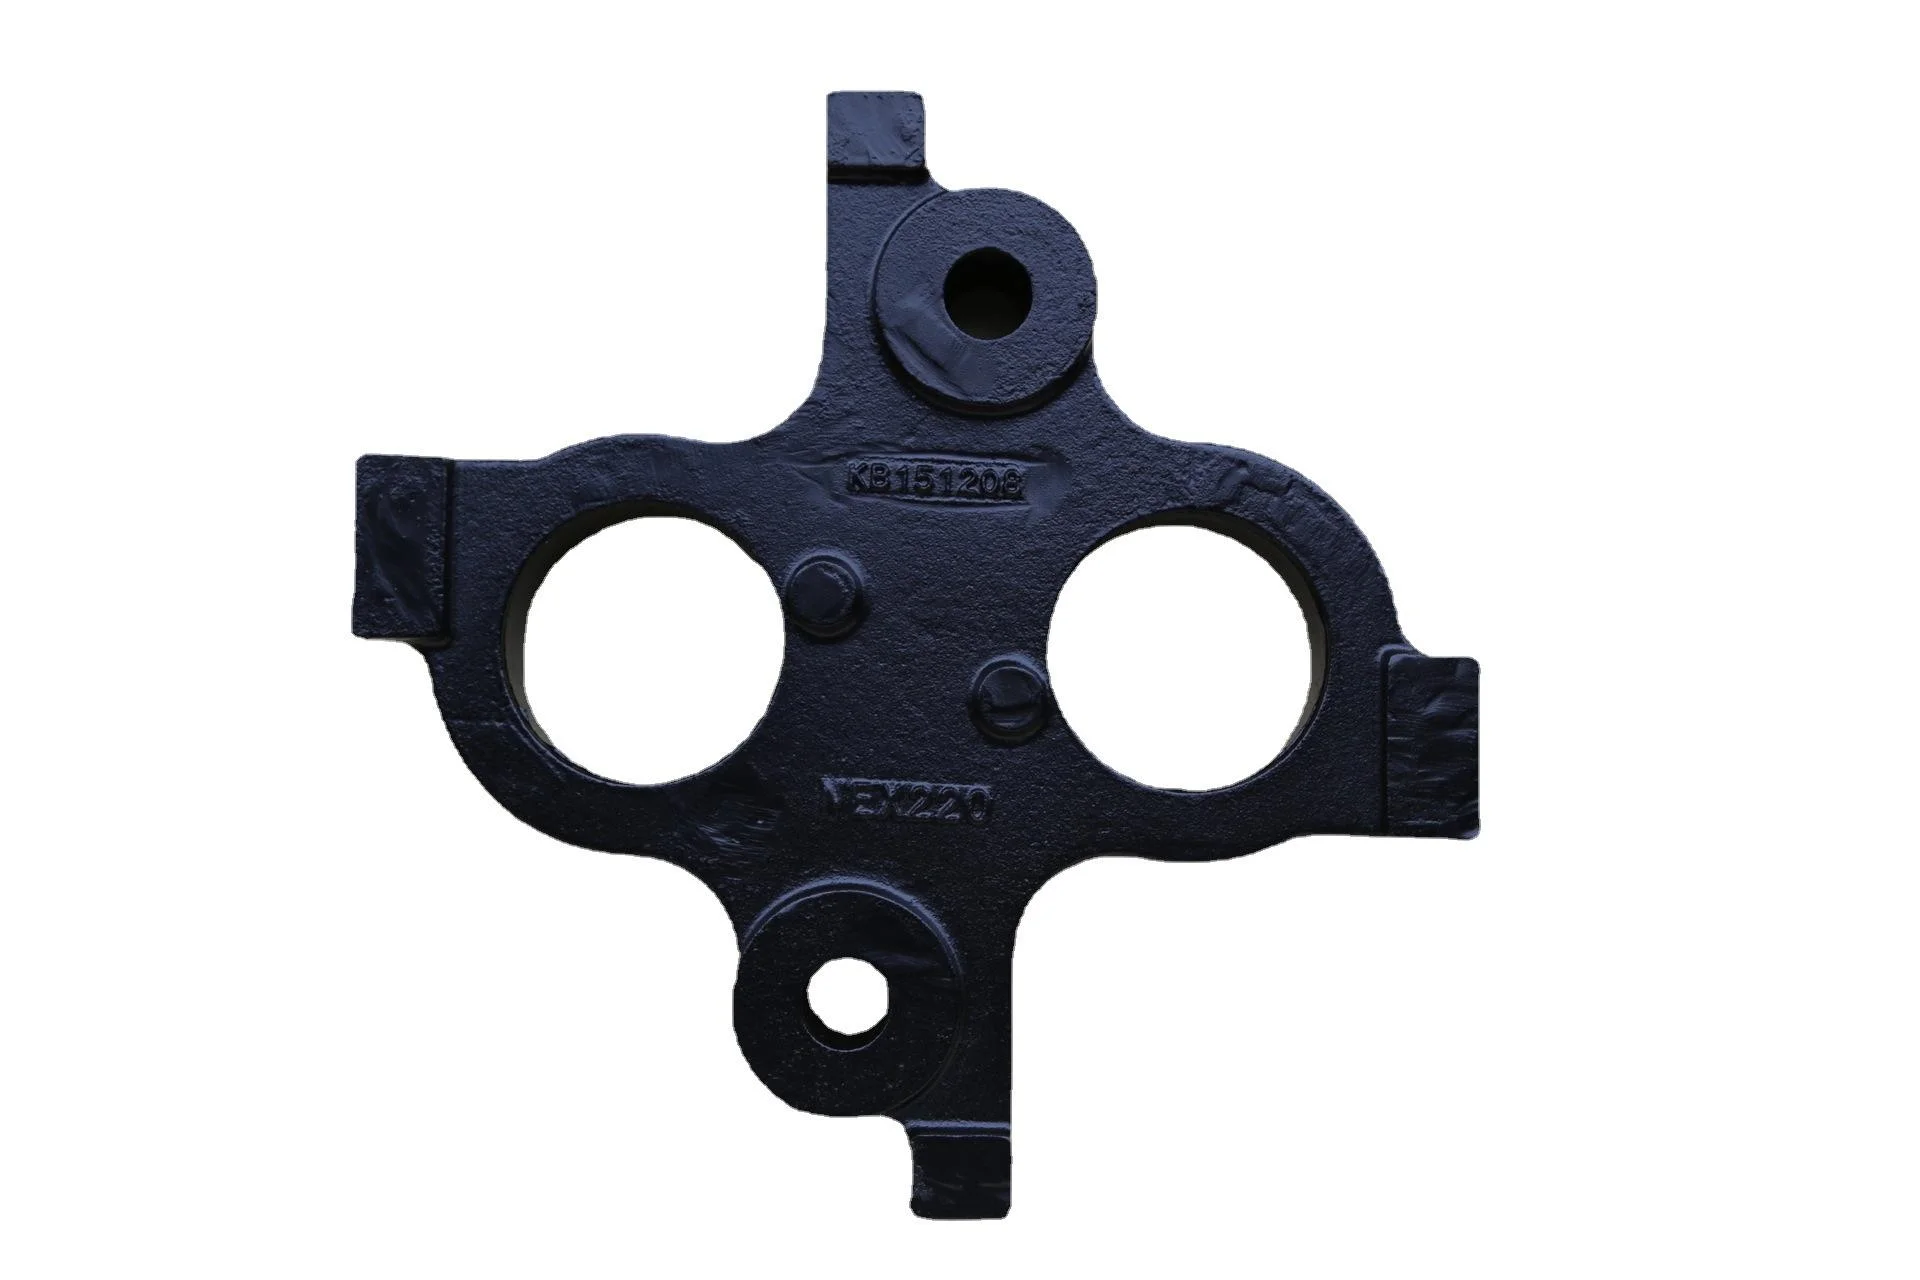
Custom GG25 GGG40 GGG45 GGG50 Agricultural Ring Wheel Castings with CNC Machining
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
MaterialGrey iron GG25 ductile iron GGG40 GGG45 ggg50
-
Type:ring wheelCertificationISO/TS16949
-
Outside diameter500mm 700mm or customizedApplicationused for agricultural machinery
-
Lead timeabout 25 daysMax weight10 Ton
-
MIN tolerance+-0.02SurfacePower coating,EP,H.D.G EG
-
Cast classCT8
Custom agricultural ring-wheel enquiries include GG25 grey iron and GGG40, GGG45 or GGG50 ductile iron. Separate cast-steel and ADC12 die-cast components are also requested within the broader service scope. Select the full grade and manufacturing route for the individual drawing.
Define the ring-wheel diameter and interfaces
Outside-diameter choices are 500 mm, 700 mm or customized, and the cast-class reference is CT8. Show the mounting geometry and the datums relating it to the wheel’s outer form. Include the machinery application and the supplied condition required for assembly.
- Provide the controlled drawing and required quantity.
- Specify the complete material designation and standard.
- Mark CNC-machined interfaces and finished dimensions.
- Identify material and dimensional acceptance records.
Assign the minimum-tolerance requirement
The minimum-tolerance reference is ±0.02, with its unit and applicable dimension to be defined for the selected part. Identify the convention, supplied stage and measurement arrangement used for acceptance. This makes the requirement specific to the actual interface rather than an unassigned limit across the whole casting. Include any access constraints that affect measurement of the finished mounting interface.
Close the treatment and document scope
Define the actual treatment system for Power coating, EP, H.D.G or EG finish requests, including coverage and contact-surface boundaries. Identify the applicable ISO/TS16949 qualification document and scope. Any sample or first-part approval should use the same grade, controlled drawing and supplied condition that governs production of the ordered component.