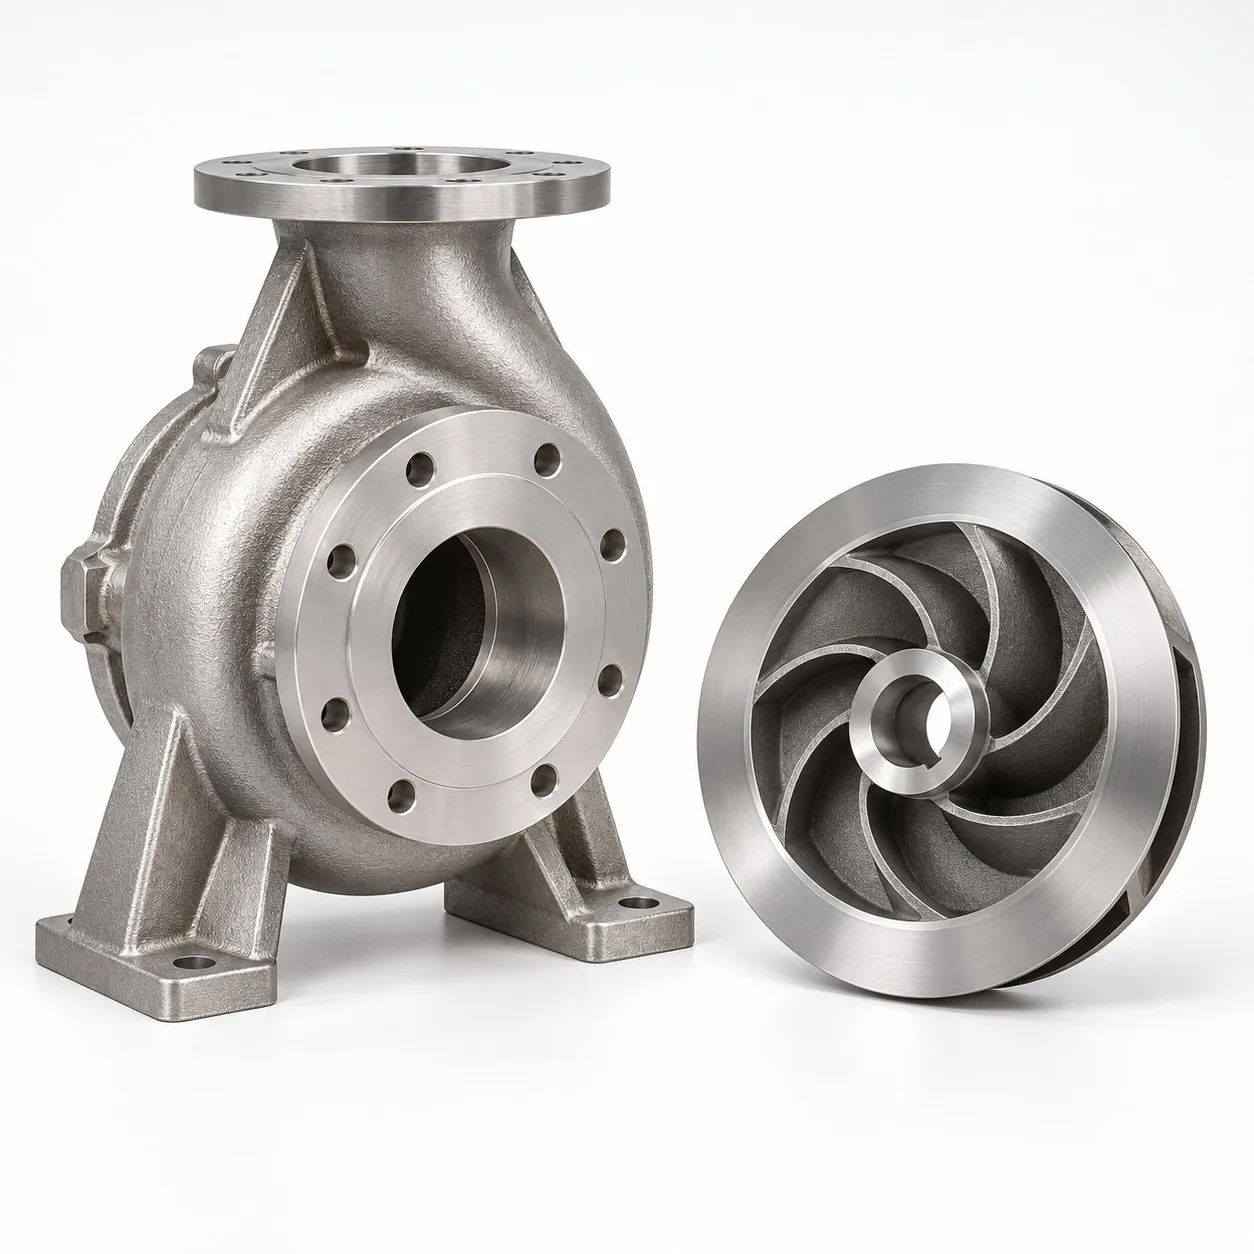
Custom OEM Centrifugal-Pump Impeller Castings for Marine and Industrial Use — Sand, Lost-Wax and Die Routes
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
Casting MethodDie Casting
-
MaterialStainless Steel, Ductile Iron, Aluminum, Spectrometer AnalysisSurface TreatmentShot Blasting, Powder Coating, Hot Dip Galvanized, E-coating, Painting
-
Tolerance & Surface RoughnessCT4-CT6 (Investment), CT10-CT12 (Sand), Ra 1.6-3.2 (Smooth Finish)Tooling & Mold DesignIn-house Tooling Design, Mold Manufacturing, Prototyping Service
-
Service TypeOEM/ODM Custom Manufacturing / PrototypingDrawing FormatsSTEP, STP, IGES, DXF, DWG, PDF
-
CertificationISO 9001, IATF 16949 , AS 9100 , CE, RoHSQuality Control100% Inspection, CMM, Projector, Caliper, Salt Spray Test
-
Lead Time7-10 Days (Prototype), 15-25 Days (Mass Production)
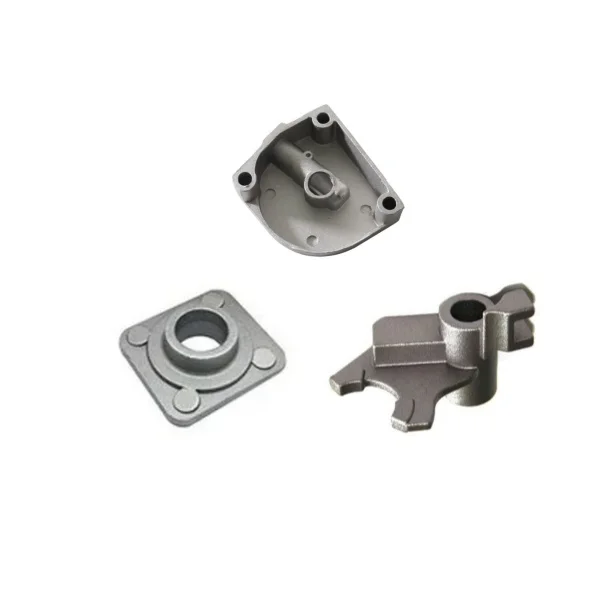
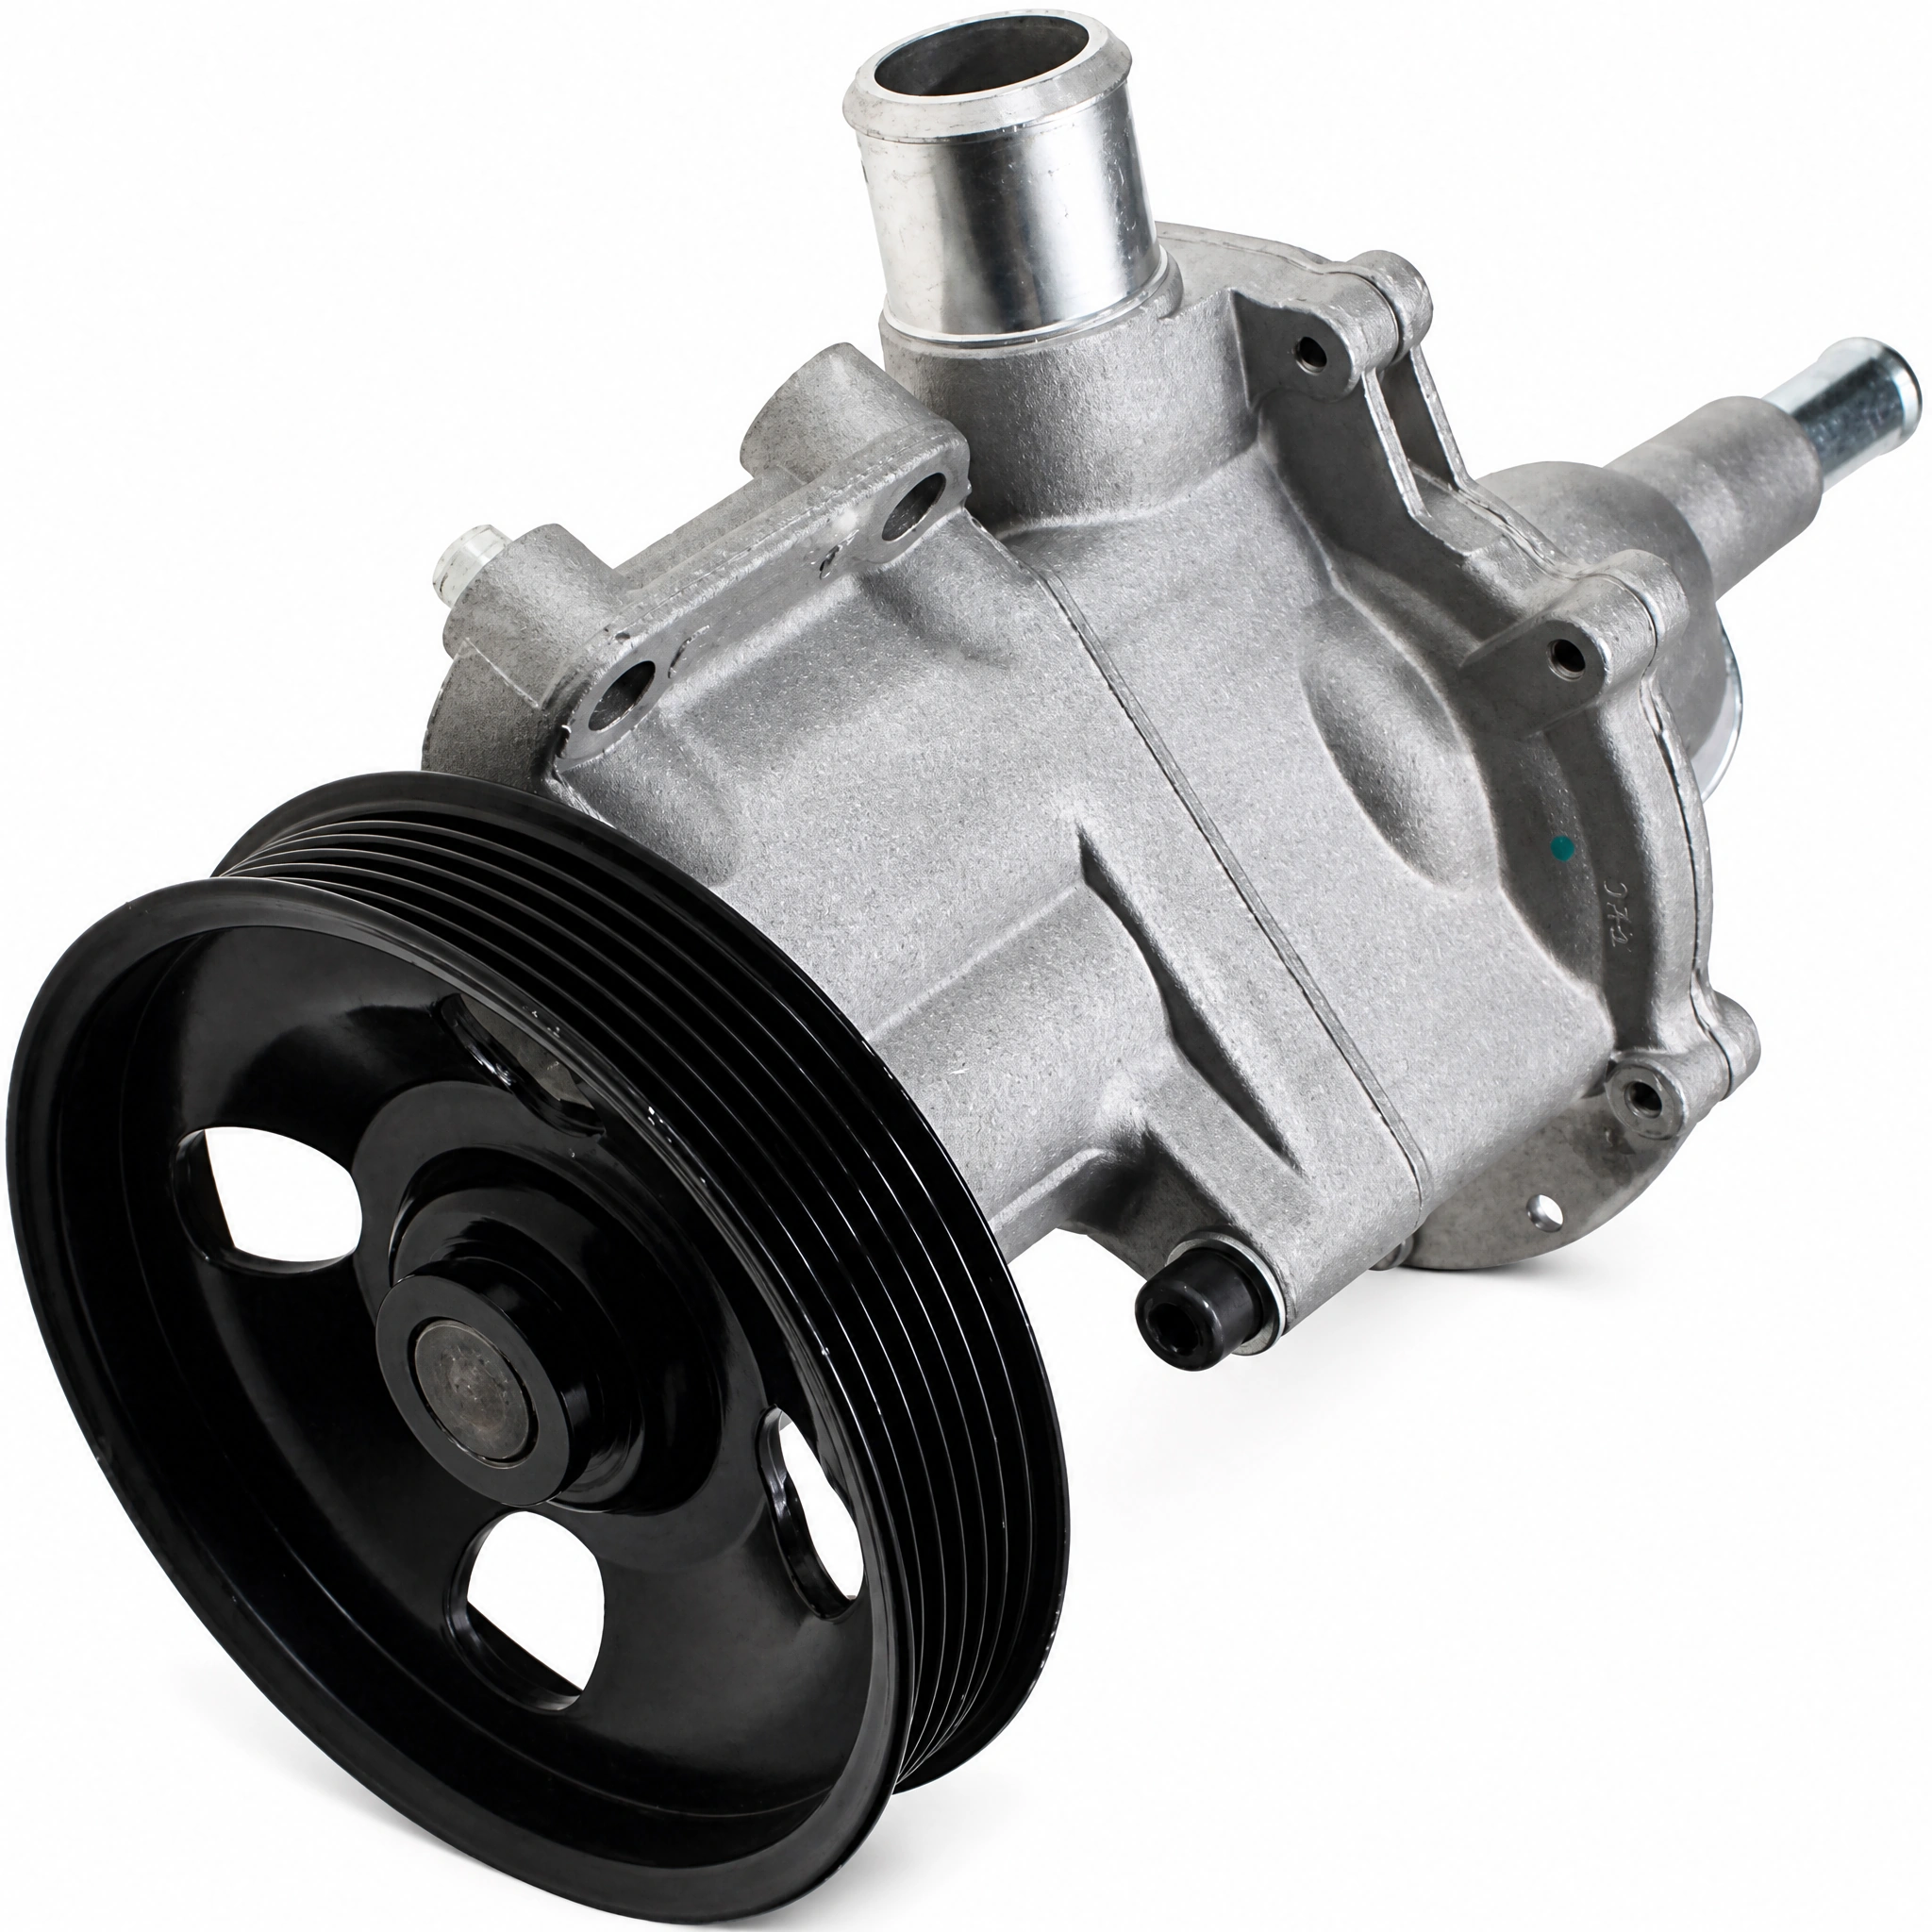
Custom centrifugal-pump impellers are offered for marine and industrial enquiries in stainless steel, ductile iron or aluminum. OEM/ODM manufacturing, in-house tooling design, mold manufacture and prototyping support can be scoped around the actual impeller drawing and its intended duty.
Link the geometry to the pump duty
Provide the blade geometry, hub interface and mating dimensions together with the operating conditions that influence material selection. Sand, lost-wax/investment and die casting are named route enquiries. Select the grade and casting method for this impeller before defining the required finished interfaces and surface condition.
Apply the tolerance references to the chosen route
CT4–CT6 is the investment-casting reference, while CT10–CT12 is the sand-casting reference. The smooth-finish entry is Ra 1.6–3.2; agree its unit and the surfaces it controls. These references help frame a drawing review when their process scope and inspection locations are kept clear.
Build an inspection plan for the impeller
The stated quality scope includes 100% inspection, spectrometer analysis, CMM, projector, caliper and salt-spray testing. Allocate the relevant checks to material, geometry and the selected finish. Shot blasting, powder coating, hot-dip galvanizing, e-coating and painting are named finish choices to match to the actual metal and service environment.
- Submit STEP/STP, IGES, DXF, DWG or PDF information.
- Specify grade, casting route and pump interfaces.
- Identify controlled surfaces and acceptance measurements.
- Request applicable ISO9001, IATF16949, AS9100, CE or RoHS documentation within its relevant scope.