OEM Bronze Impeller and Stainless-Steel Precision Castings — Investment Lost-Wax Casting with CNC Machining
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
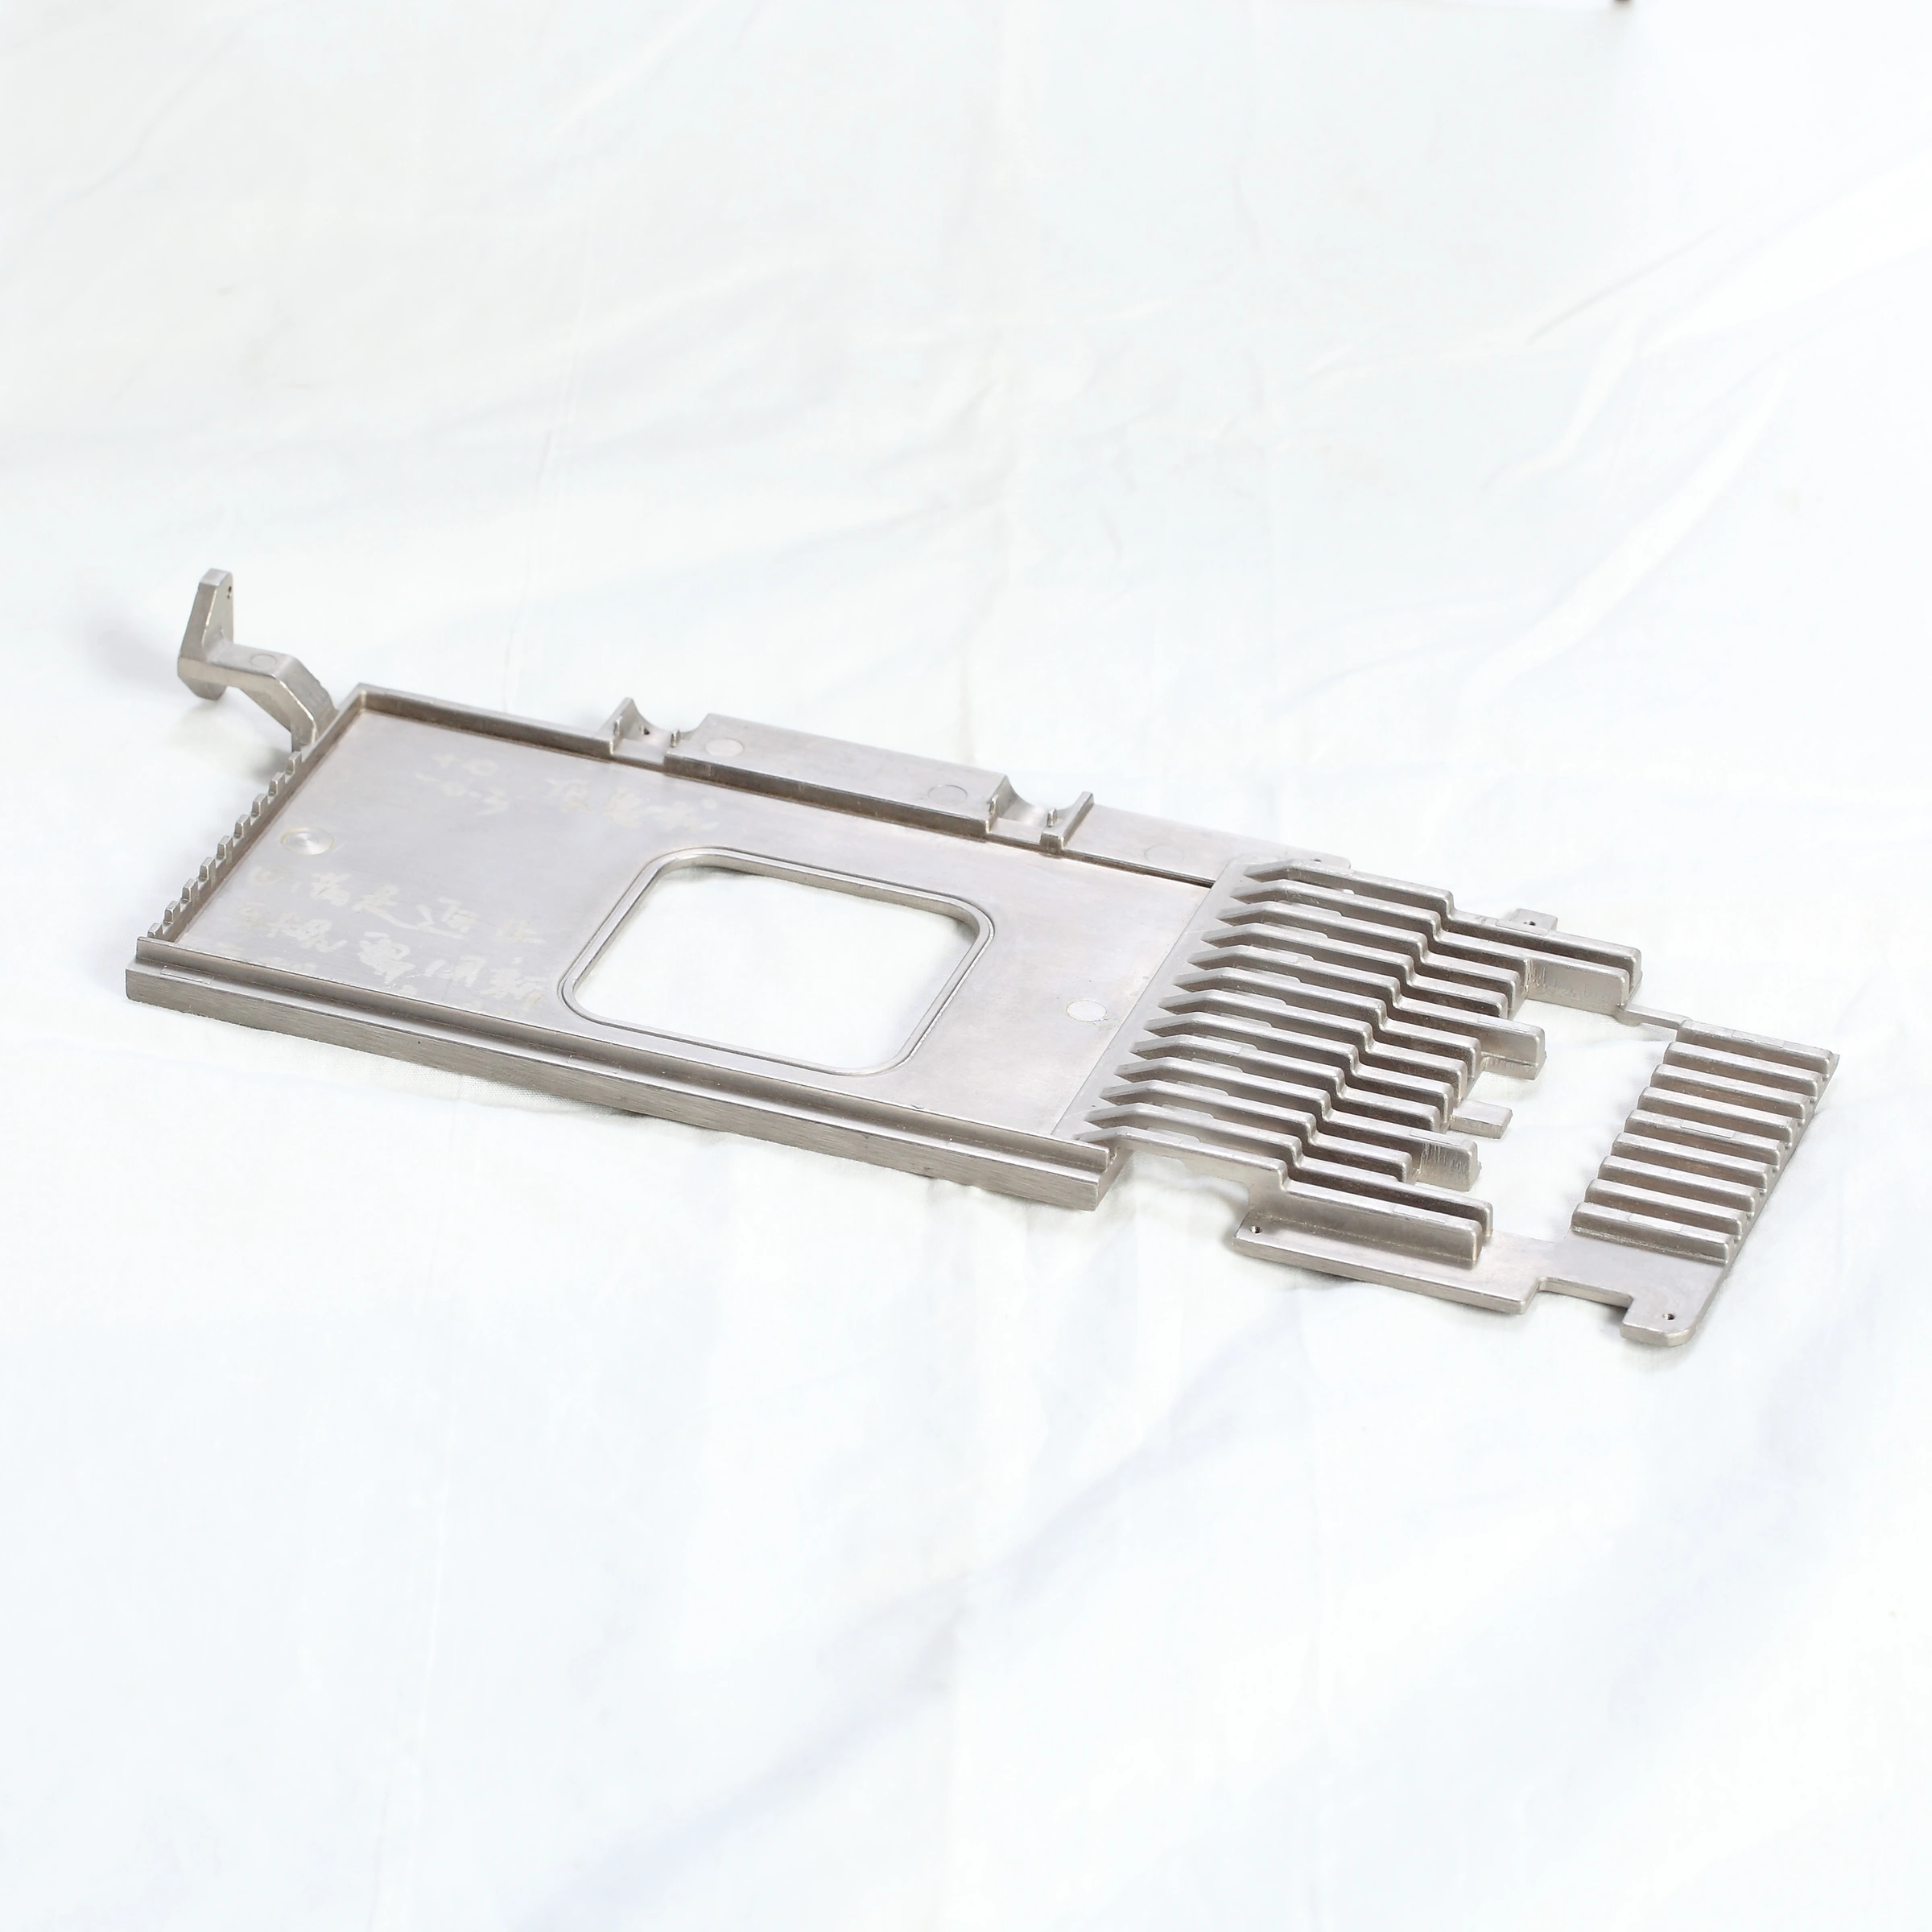
NameStainless steel die casting
-
MaterialcustomSurface treatmentNo cape burr sand hole
-
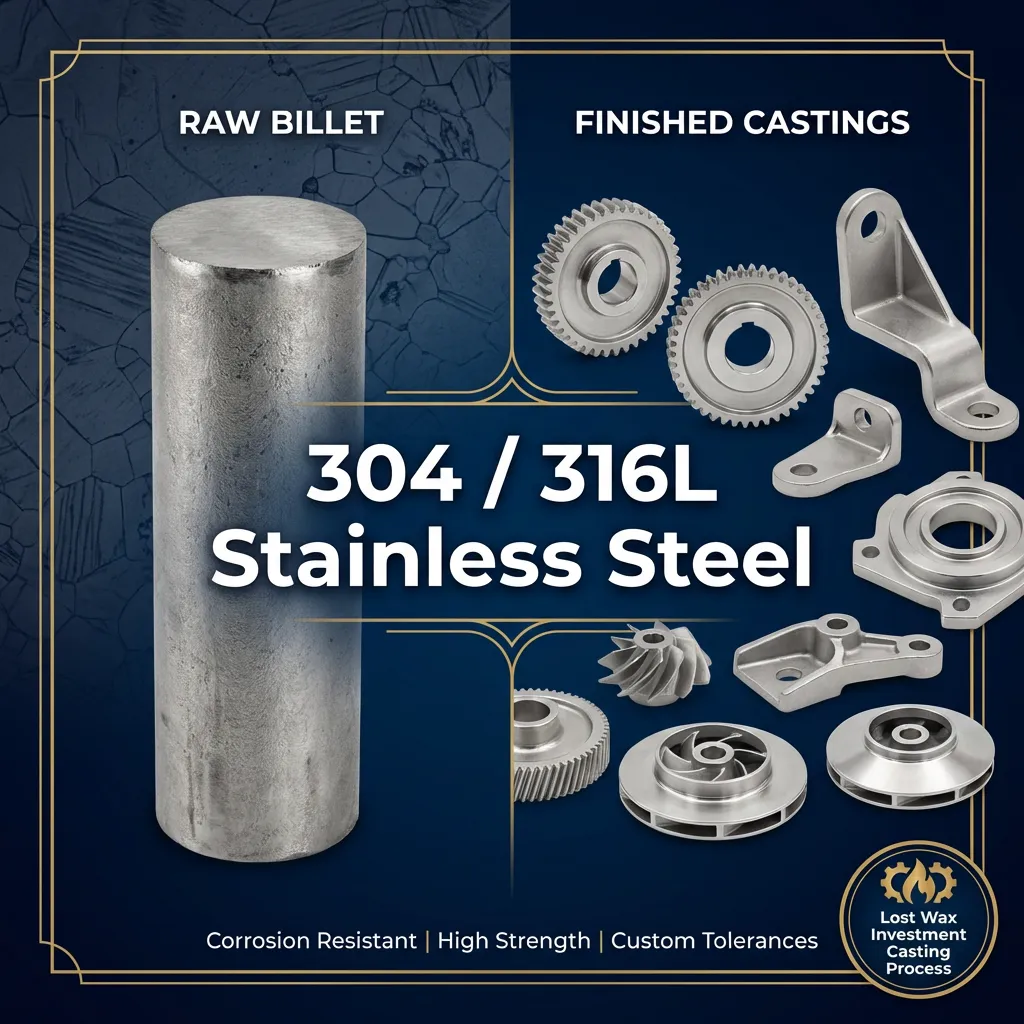
ColorCUSTOMKeywordStainless steel precision casting
-
Quality Control100% InspectionTolerance0.2mm
-
Machining ProcessLost Wax+CNC MechiningLead Time15-35 Days
-
SurfacePerfect Appearance
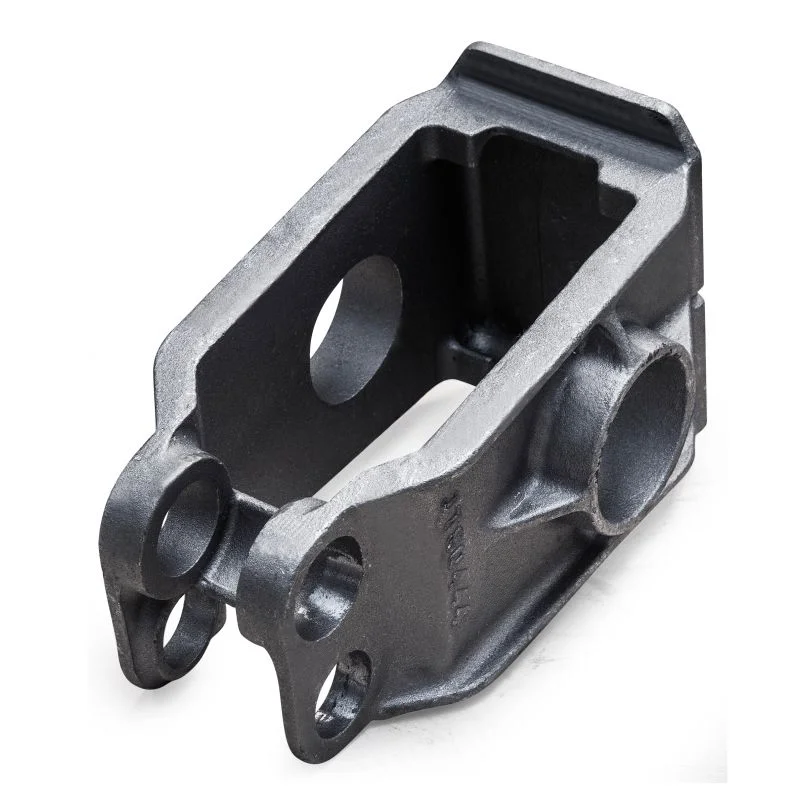
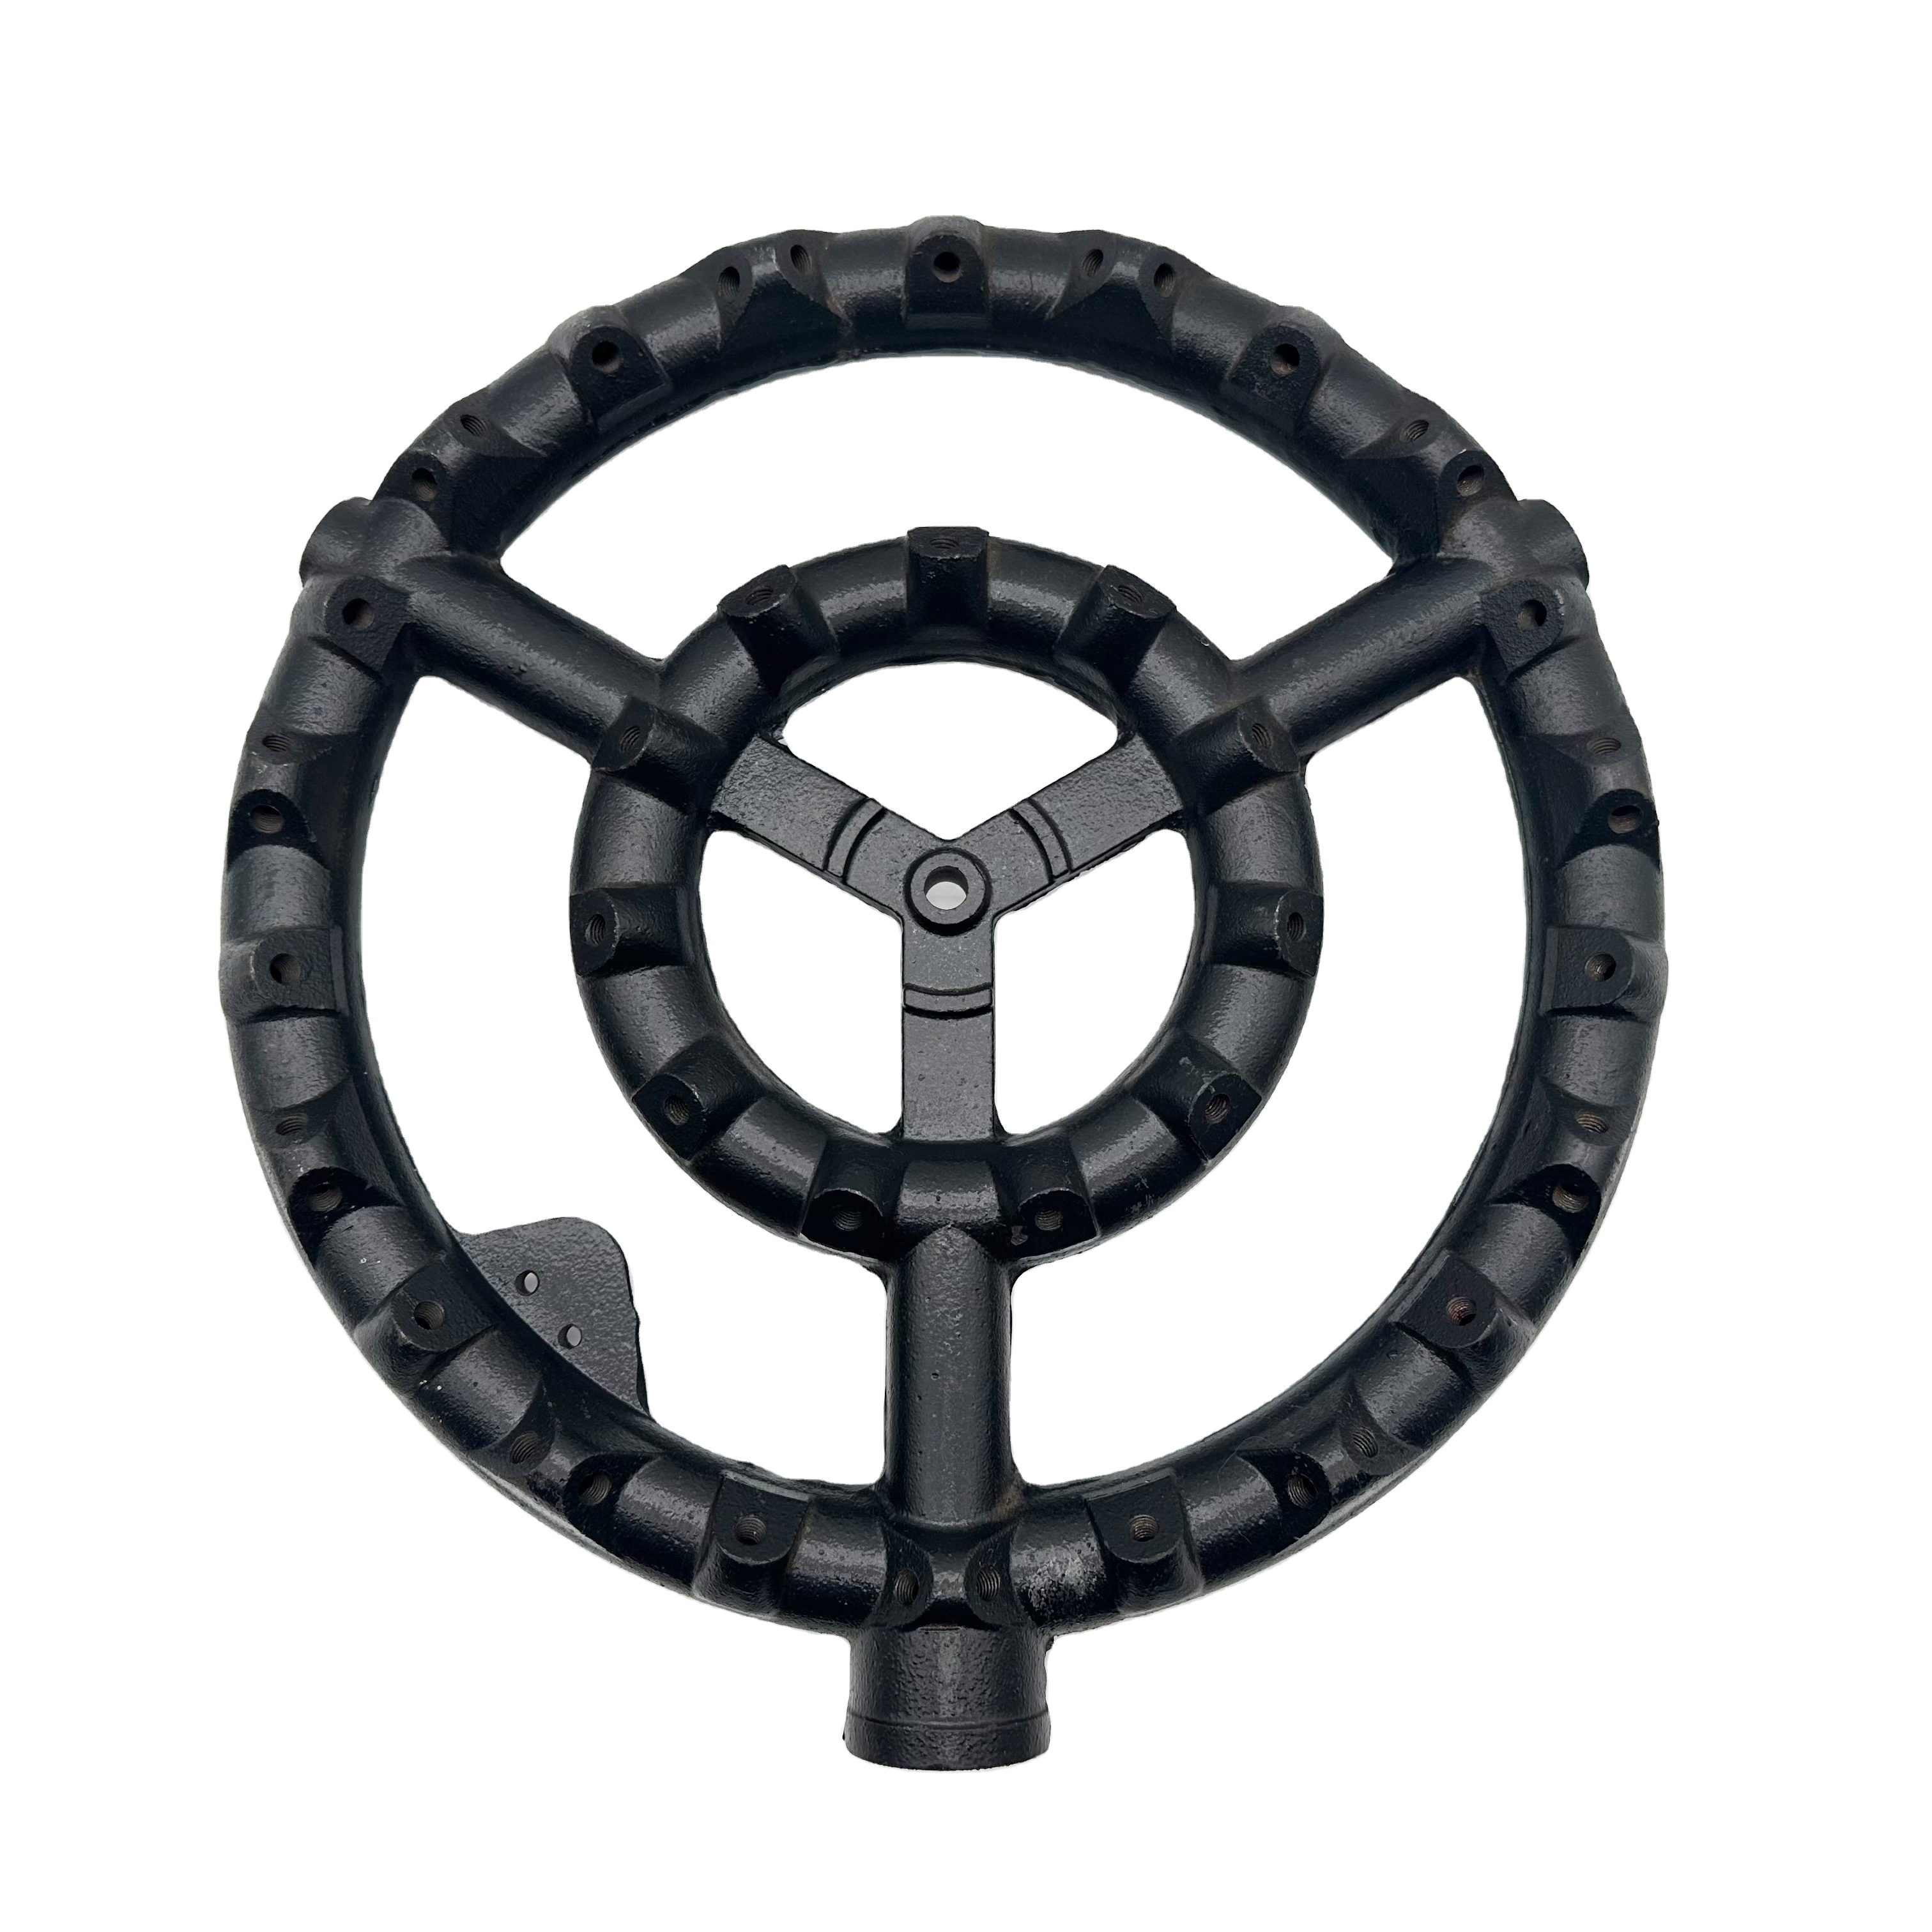
OEM precision-casting enquiries include bronze impellers and separately selected stainless-steel investment/lost-wax components. CNC machining, customized material and color can be defined around the actual drawing and the required finished condition.
Distinguish the impeller from other cast components
For a bronze impeller, provide the blade geometry, hub or shaft connection and service conditions. A stainless-steel component should identify its own grade and mating requirements. Each item can then have a clear material and acceptance brief rather than sharing an assumed component definition.
Match the process and precision scope to the item
Lost-wax casting plus CNC machining is the named process. A stainless-steel die-casting request should have its own agreed manufacturing definition. The stated tolerance reference is 0.2 mm; locate the applicable dimensions and process stages on the drawing so the machining and inspection scope follows the actual part.
- Identify the bronze impeller or stainless-steel component.
- Select the full grade and agreed casting route.
- Mark machined interfaces and dimensional limits.
- Specify custom color and visible-surface acceptance.
- State quantity and the required inspection records.
Define the appearance and operational checks
Quality control is stated as 100% inspection, with appearance requirements for flash, burr and sand-hole control. Identify the surfaces and checking criteria needed for acceptance. For an impeller, include any required balancing or service tests in the design brief so those requirements are considered for the selected component.