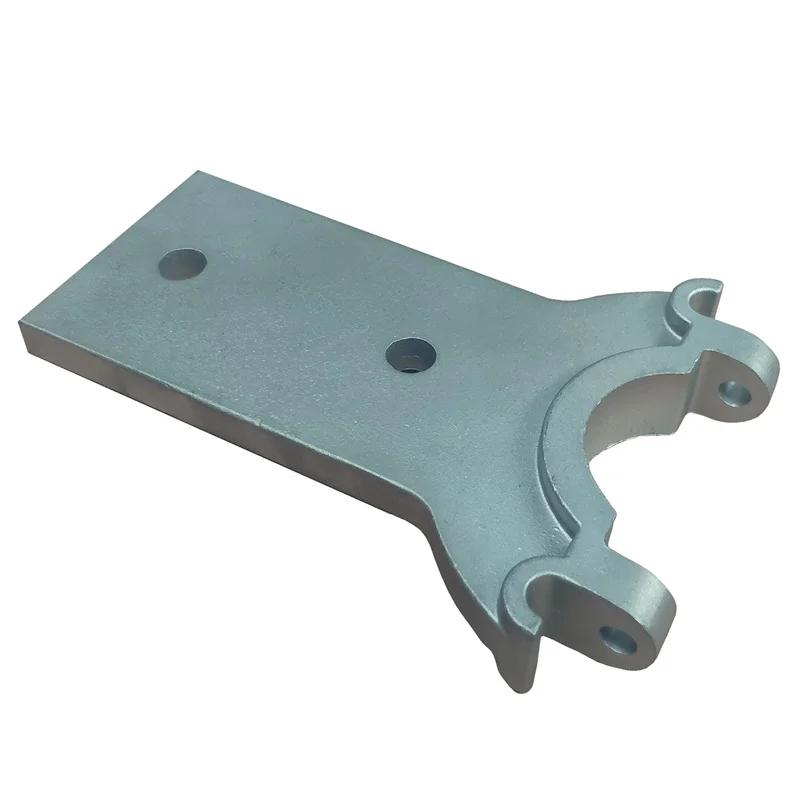
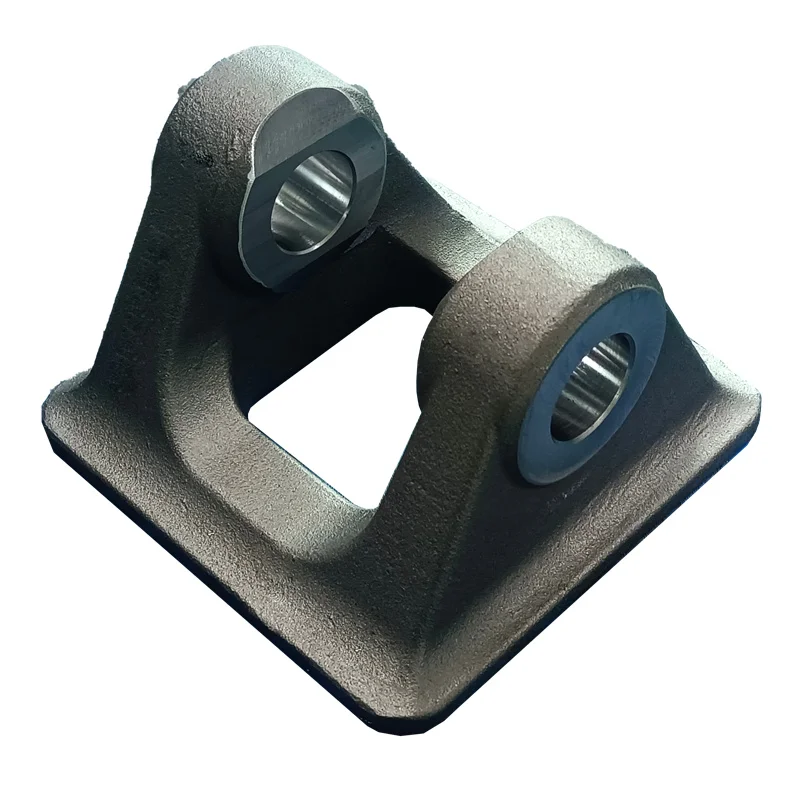
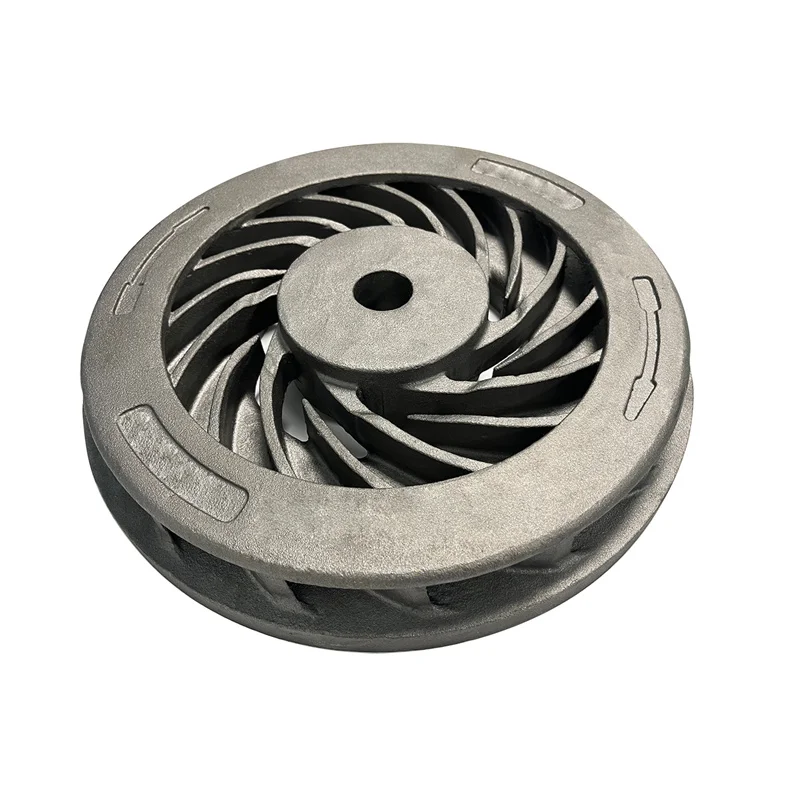
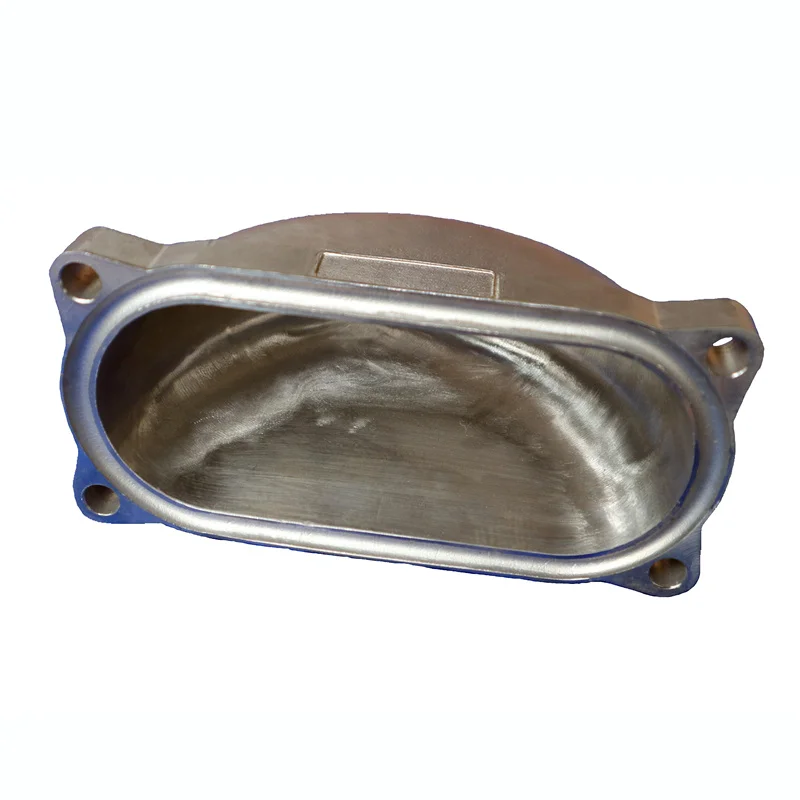
Precoated Sand or Lost Wax Investment Railway Casting with CNC Quench Temper Shot Blasting and Assembly Services
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
Nameprecoated sand casting factory
-
Keywordsmodel castingAppplicationRailway
-
ProcessLost wax investment casting+CNC machinedHeat TreatmentQuench and temper by 2 set mesh belt furnaces
-
Surface TreatmentShot blasting+AssemblingMachining Facility50+ Machining centers,80+ CNC machines
-
InspectionMT/UT/RT/100% visual+100%gage/CMMStandardASTM. AISI. DIN. BS. JIS. NF. AS.
-
CertificationIATF16949/ISO14001
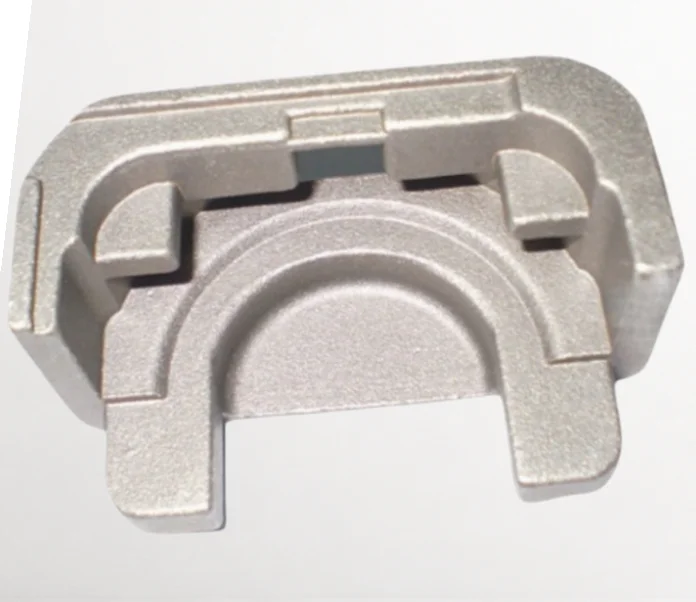
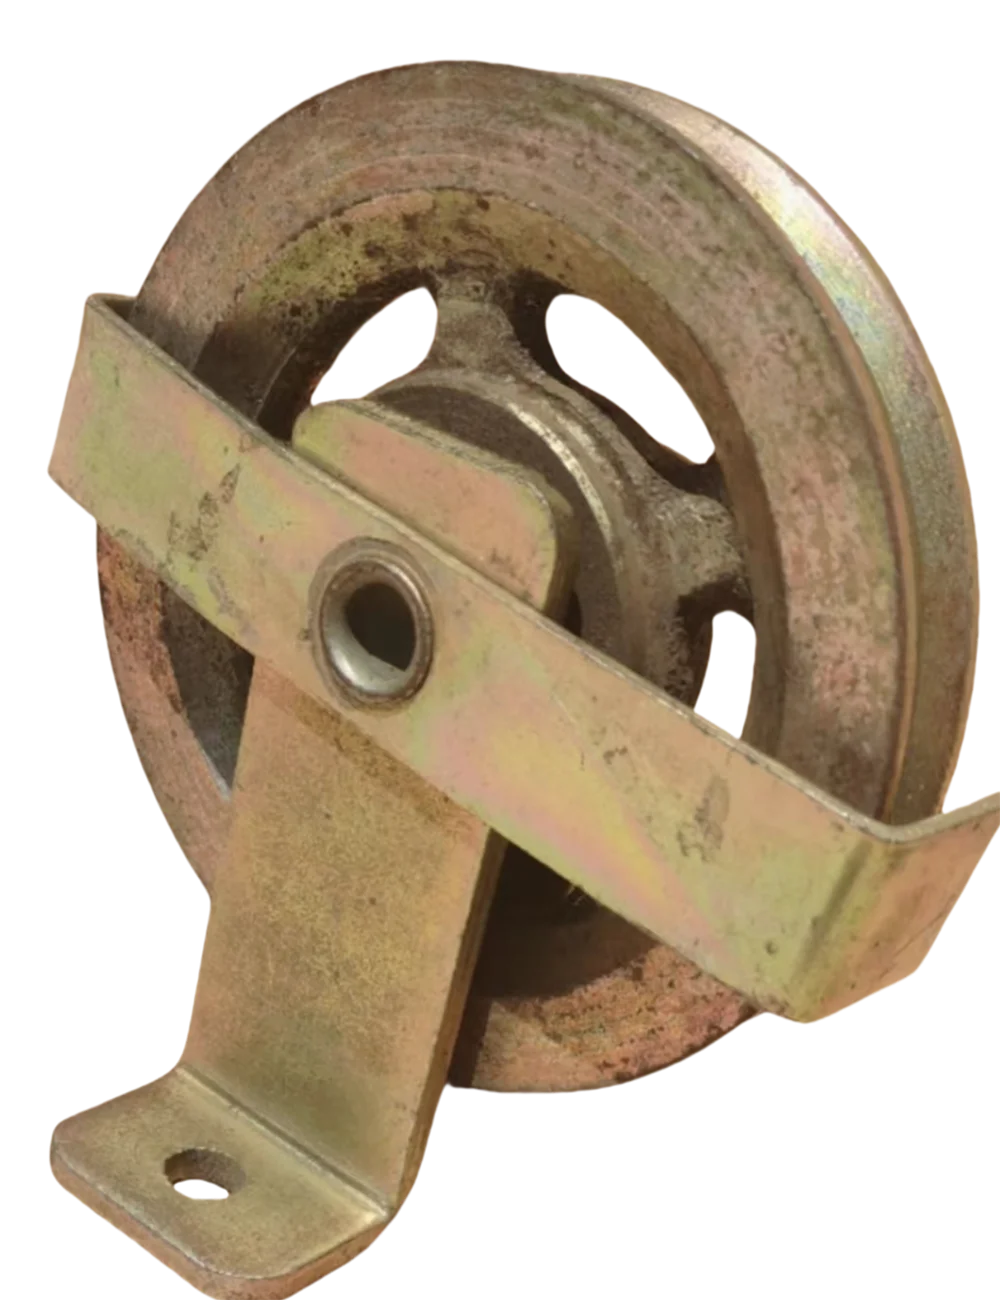
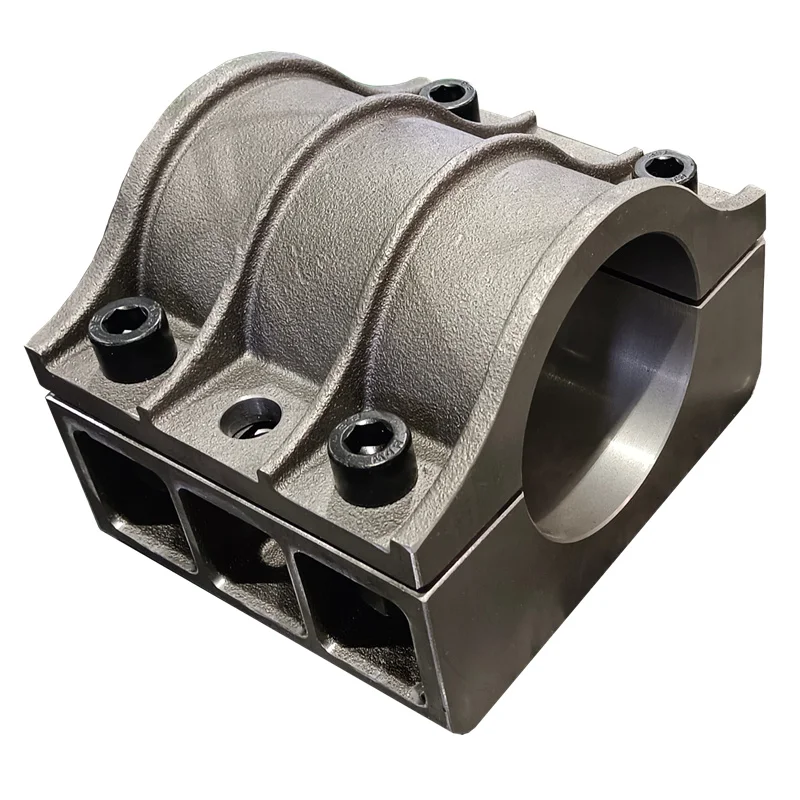
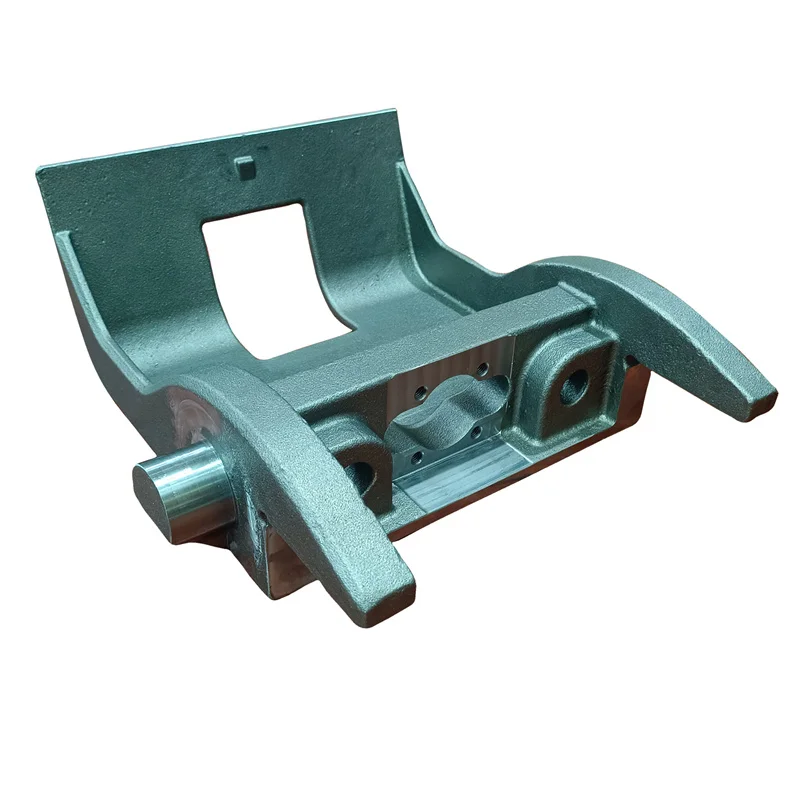
Railway-component enquiries can use selected precoated-sand or lost-wax investment casting with CNC machining, shot blasting and assembly. Define the actual supplied part, complete material specification and compatible route first. The finished component and any assembled interfaces need their own drawing-controlled acceptance requirements.
Allocate thermal and machining resources
Quenching and tempering resources include two mesh-belt furnaces. More than 50 machining centers and more than 80 CNC machines are named service resources; agree their actual work allocation for the selected design. Identify the thermal condition, machining operations and finished interfaces required by the railway component.
Specify examination areas and methods
Available inspection methods include MT, UT, RT and CMM. The stated complete checking scopes are 100% visual examination and 100% gauge checks, rather than an automatic percentage for every other method. Define the examination areas, acceptance criteria and records appropriate to the chosen material and part.
- Select applicable documents within ASTM, AISI, DIN, BS, JIS, NF or AS standard families.
- Request IATF16949 and ISO14001 records with the relevant holder and activity scope.
- Identify the shot-blasted surfaces and required result at assembled contacts.
Establish the railway work package
Provide the controlled drawing revision, quantity and operating duty. Mark dimensional relationships assessed after processing and any assembly checks needed for acceptance. Agree the initial component-approval records and actual project qualifications before production. Keep material, route and inspection changes connected to that supplied-item definition, so a later request addresses the same railway component and required finished condition.