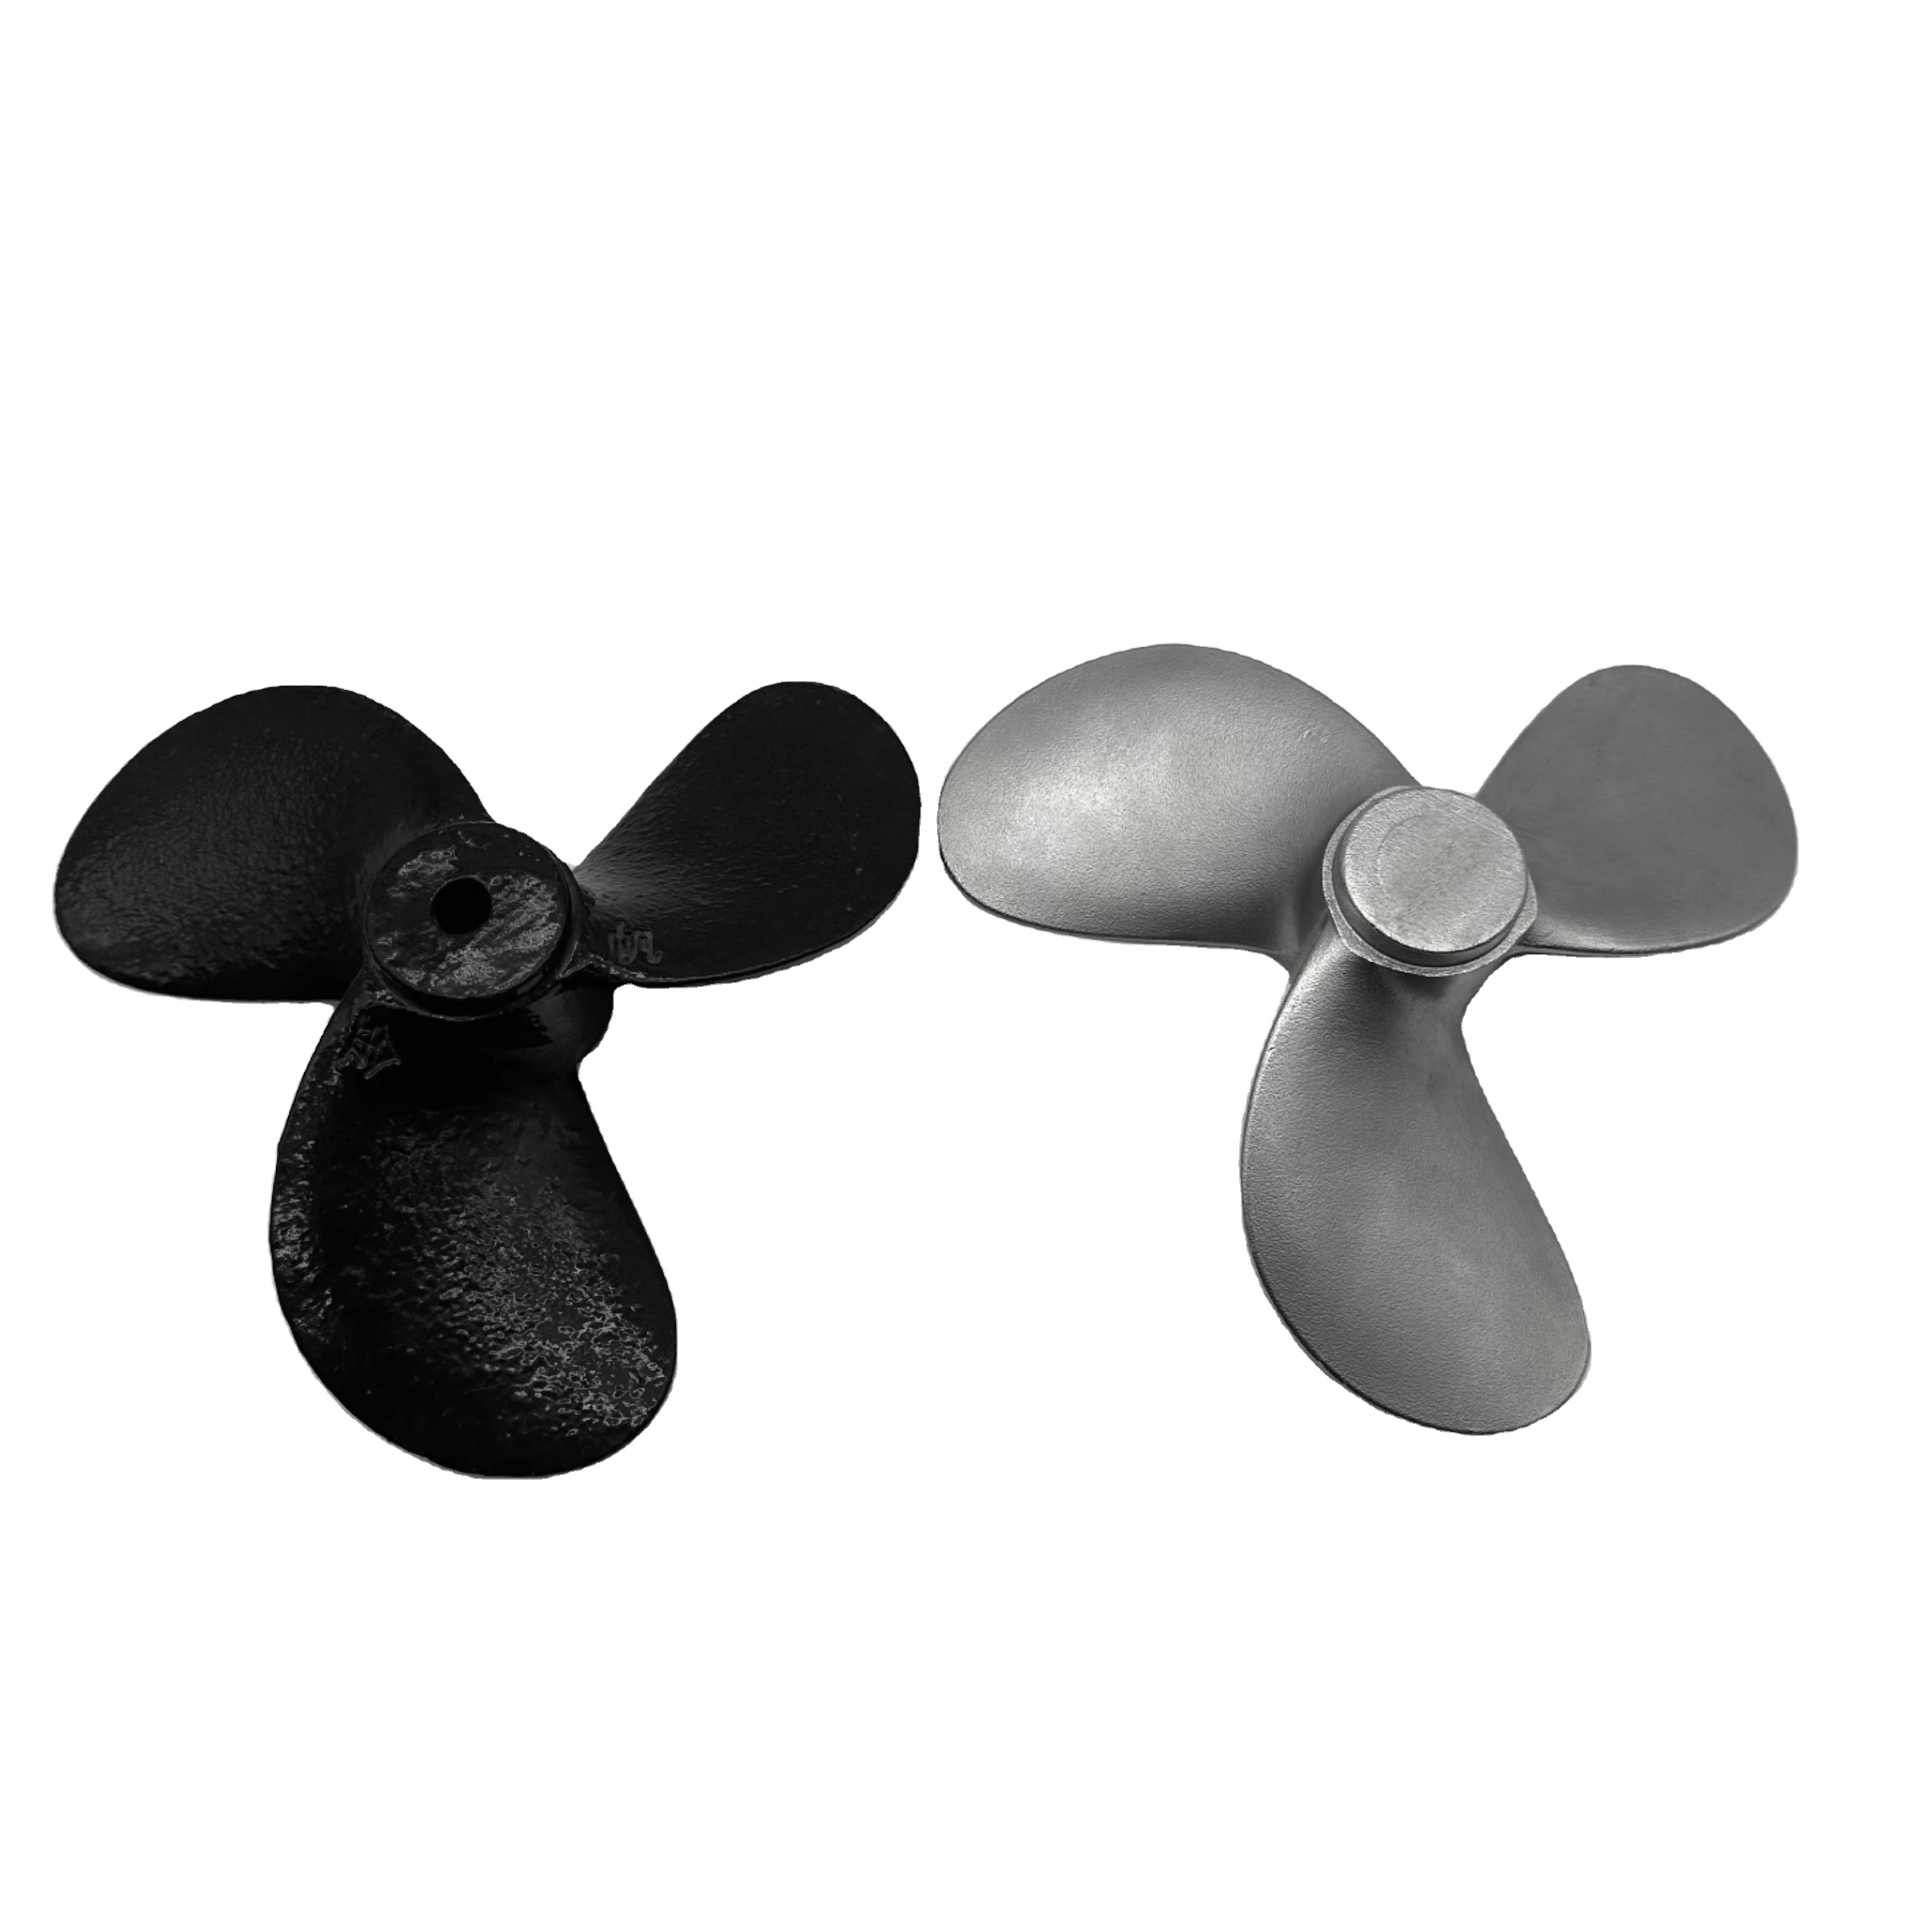
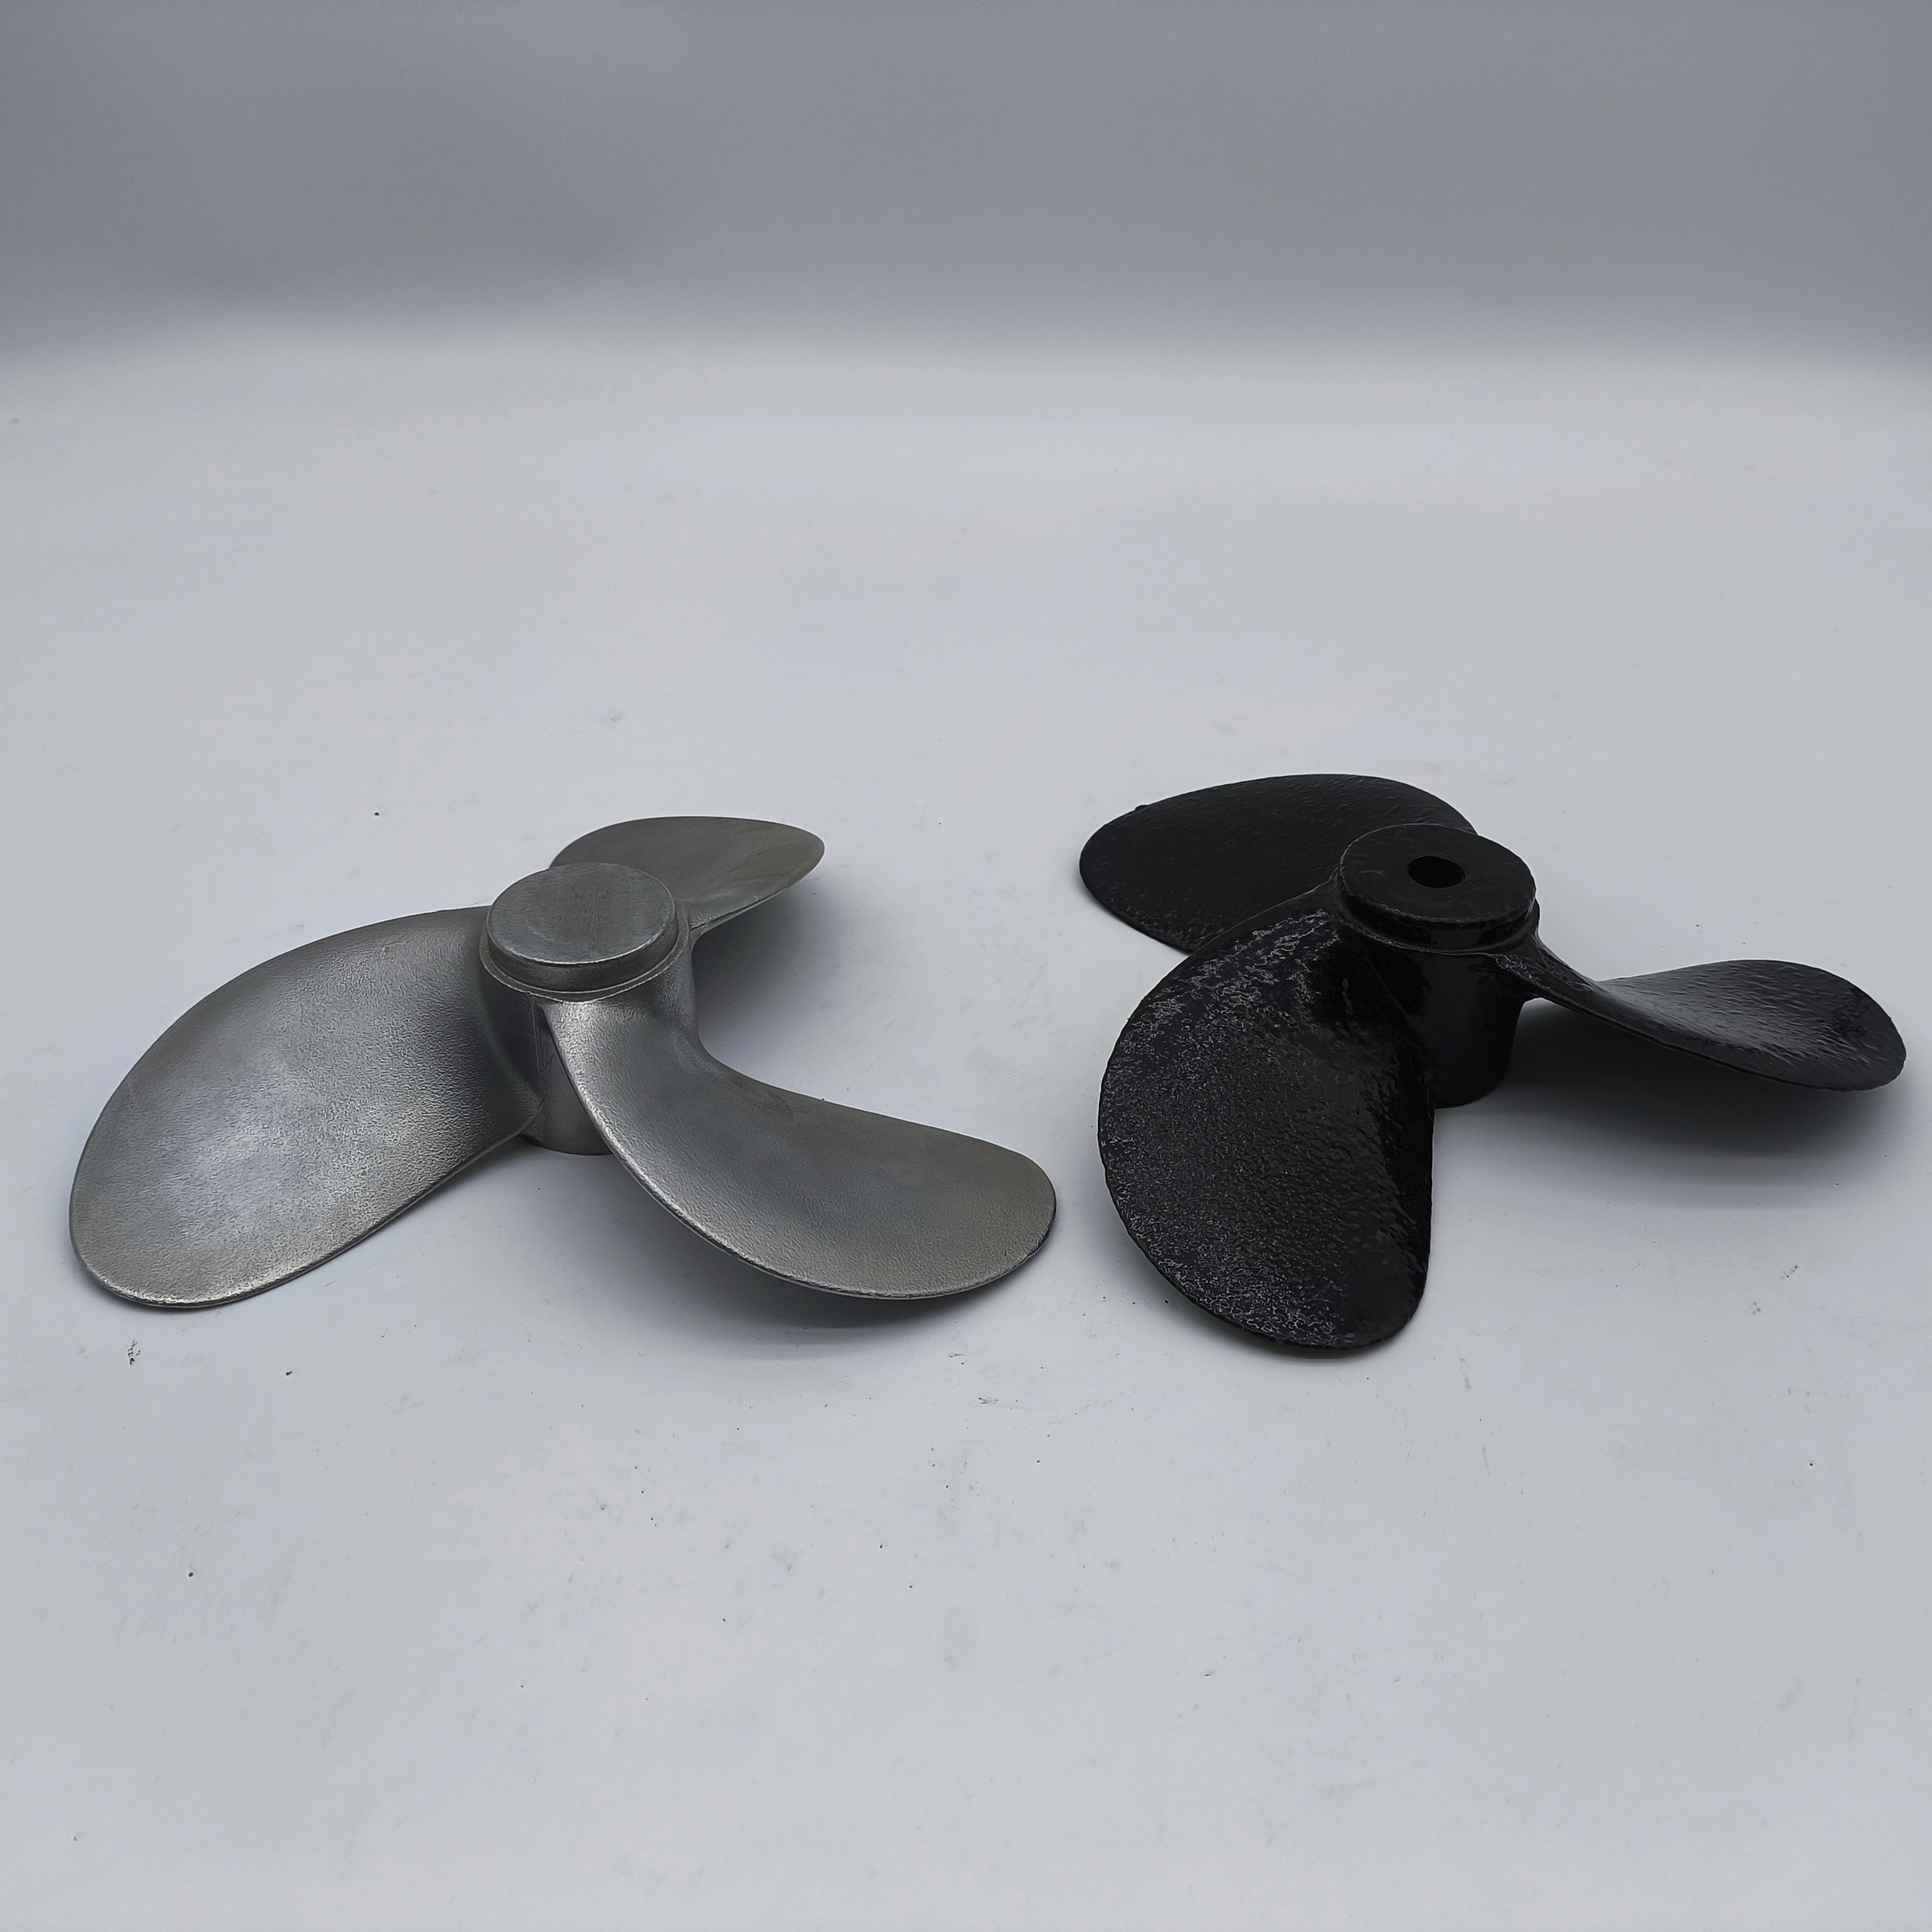
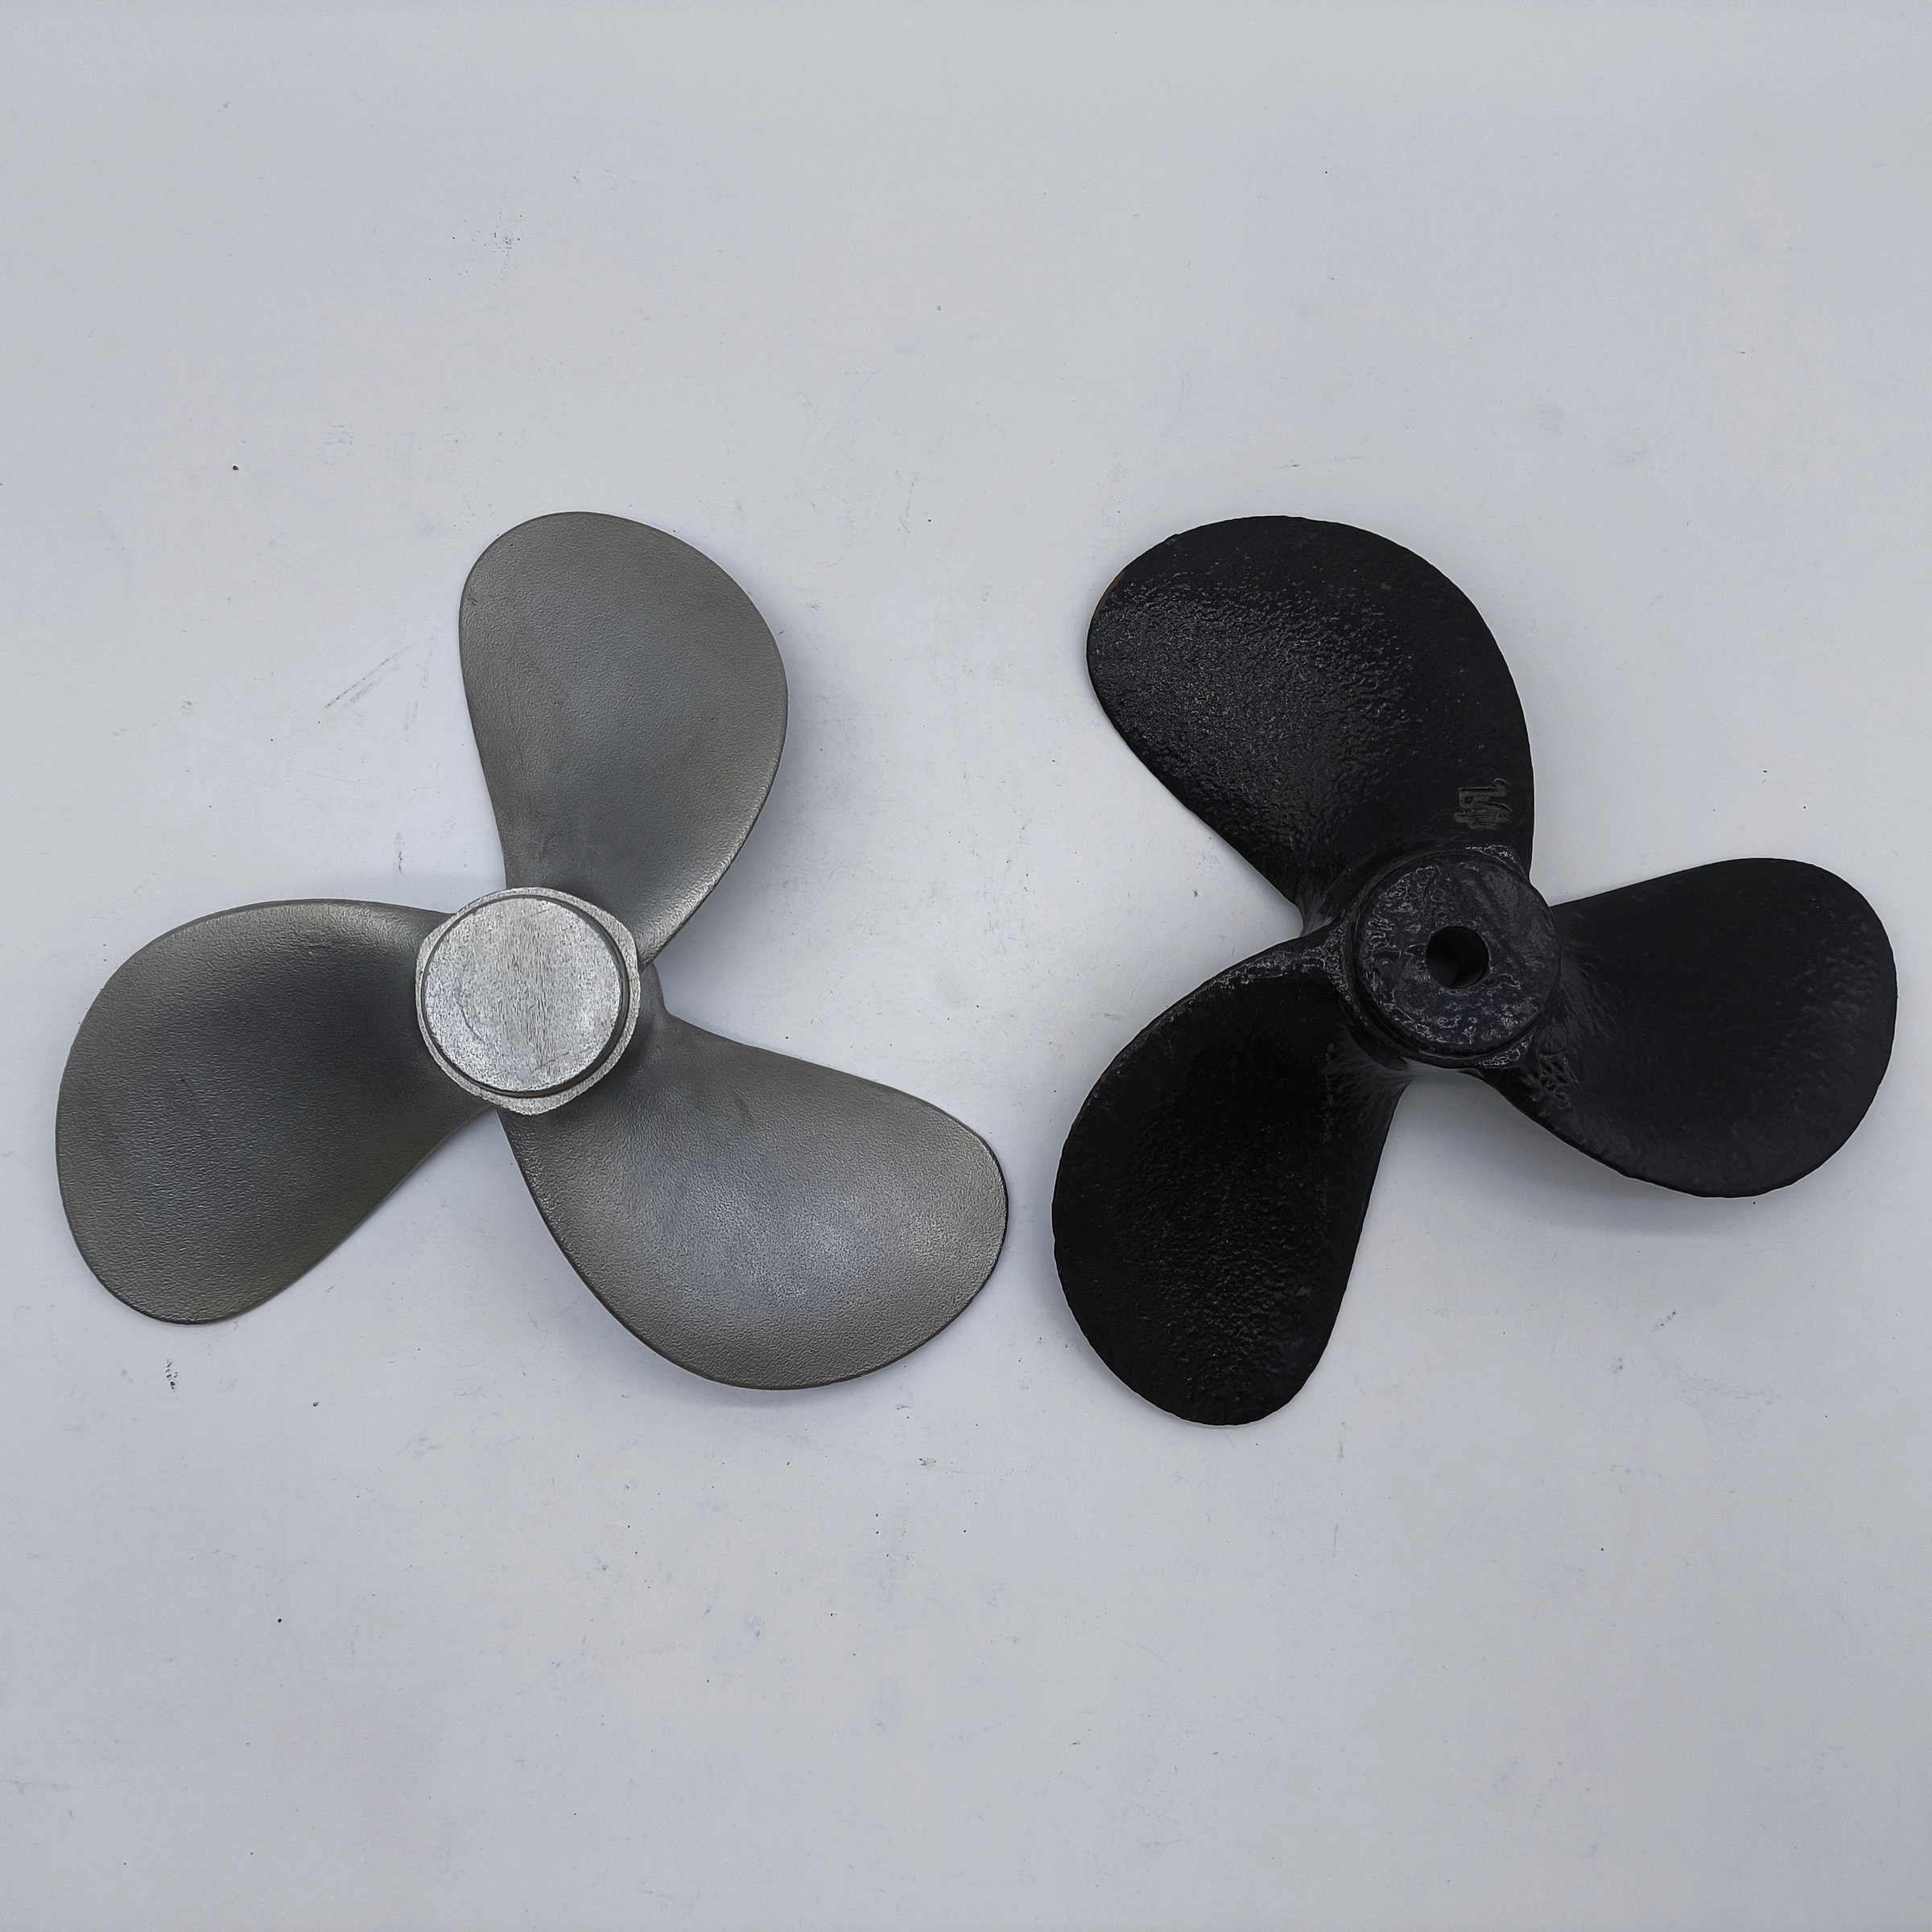
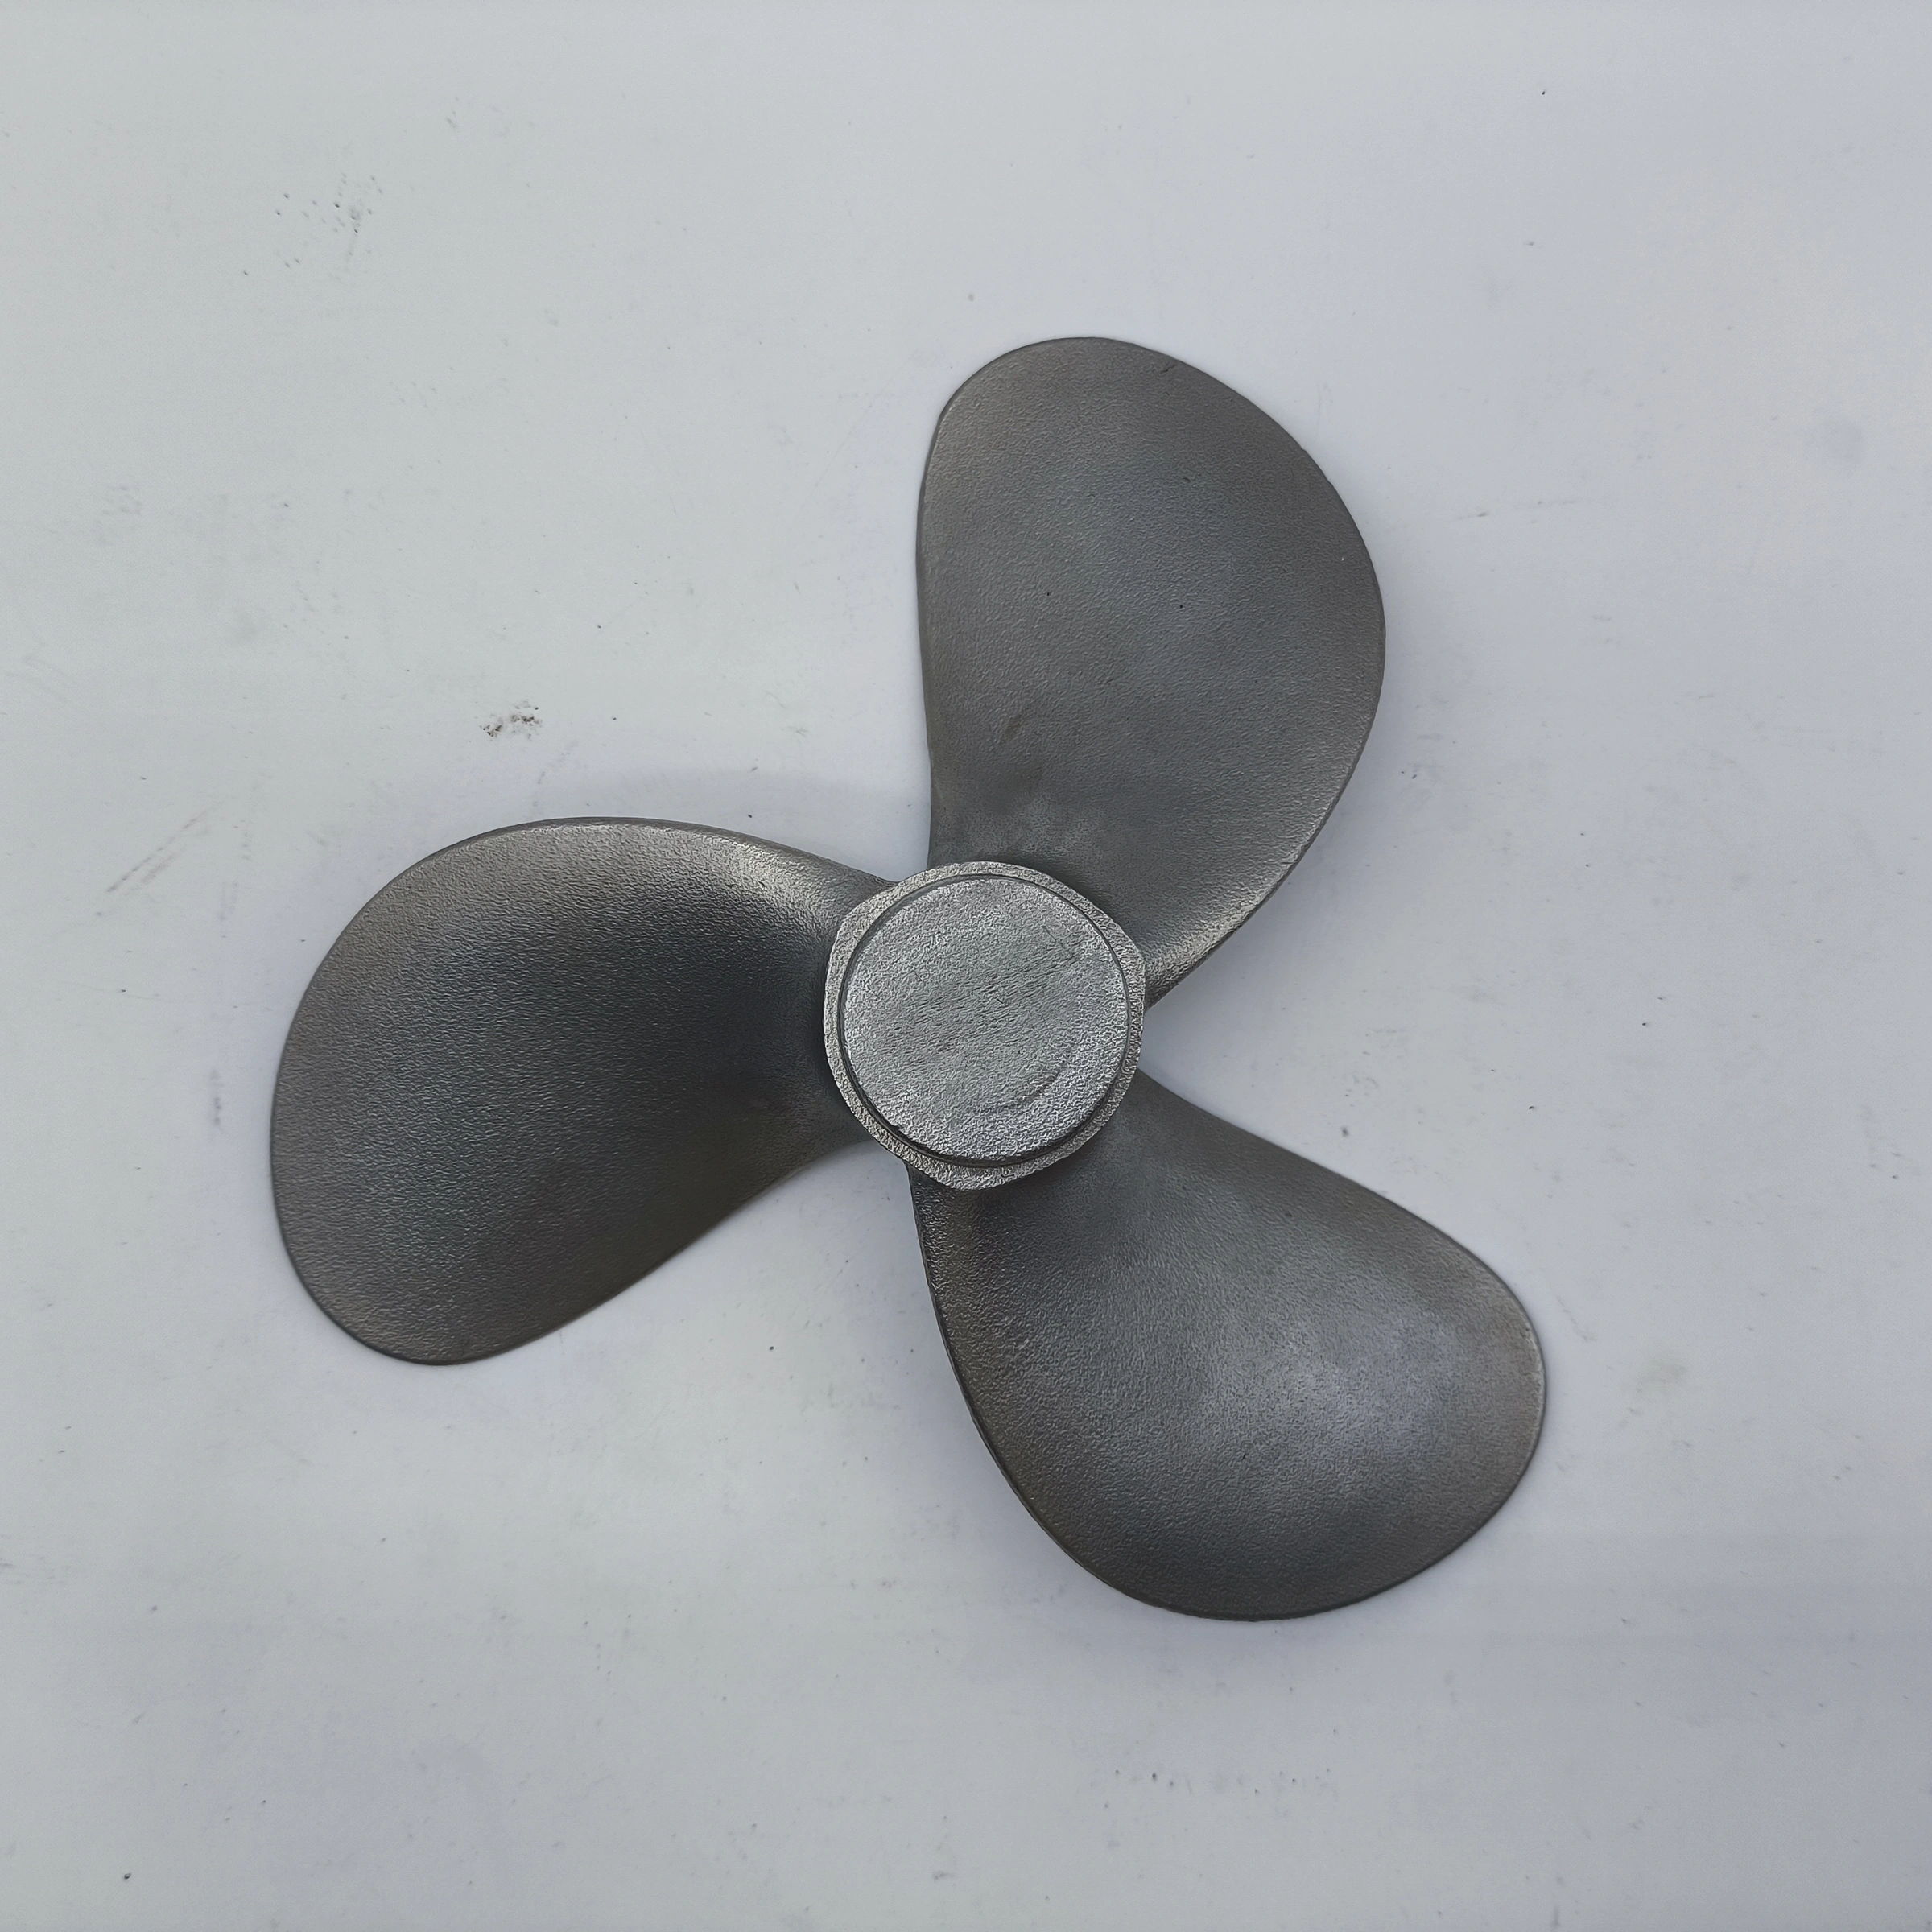
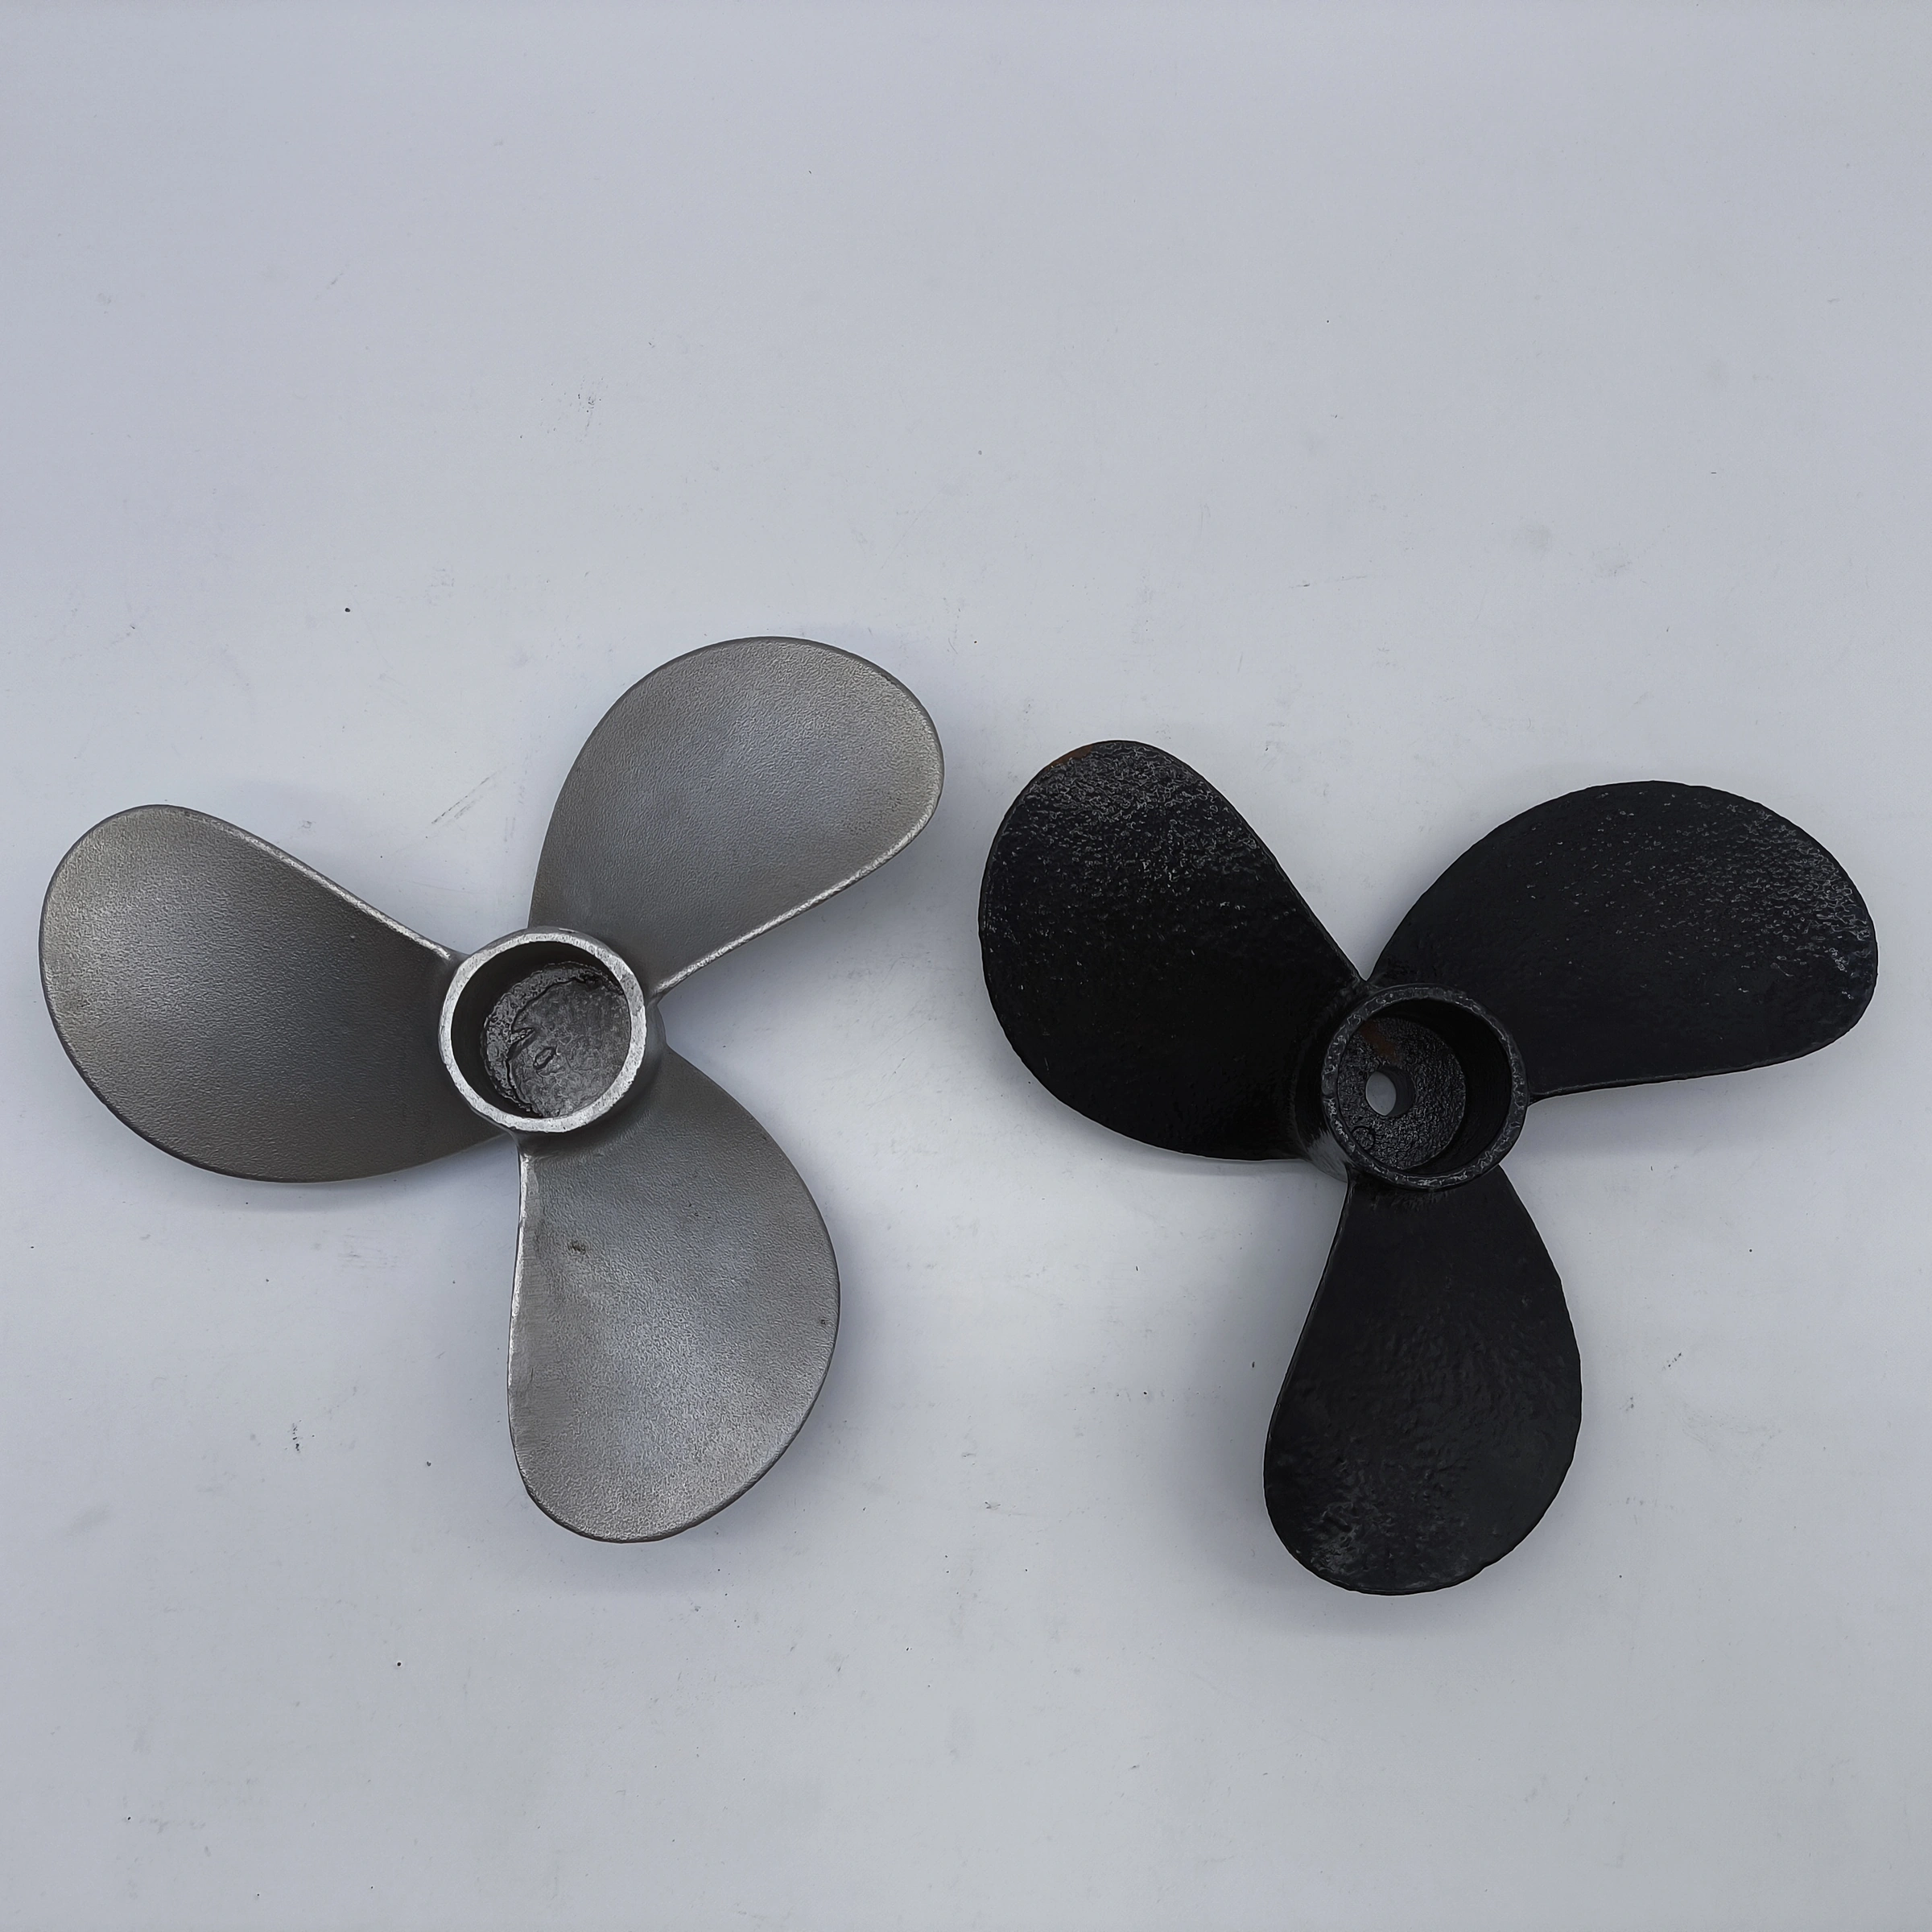
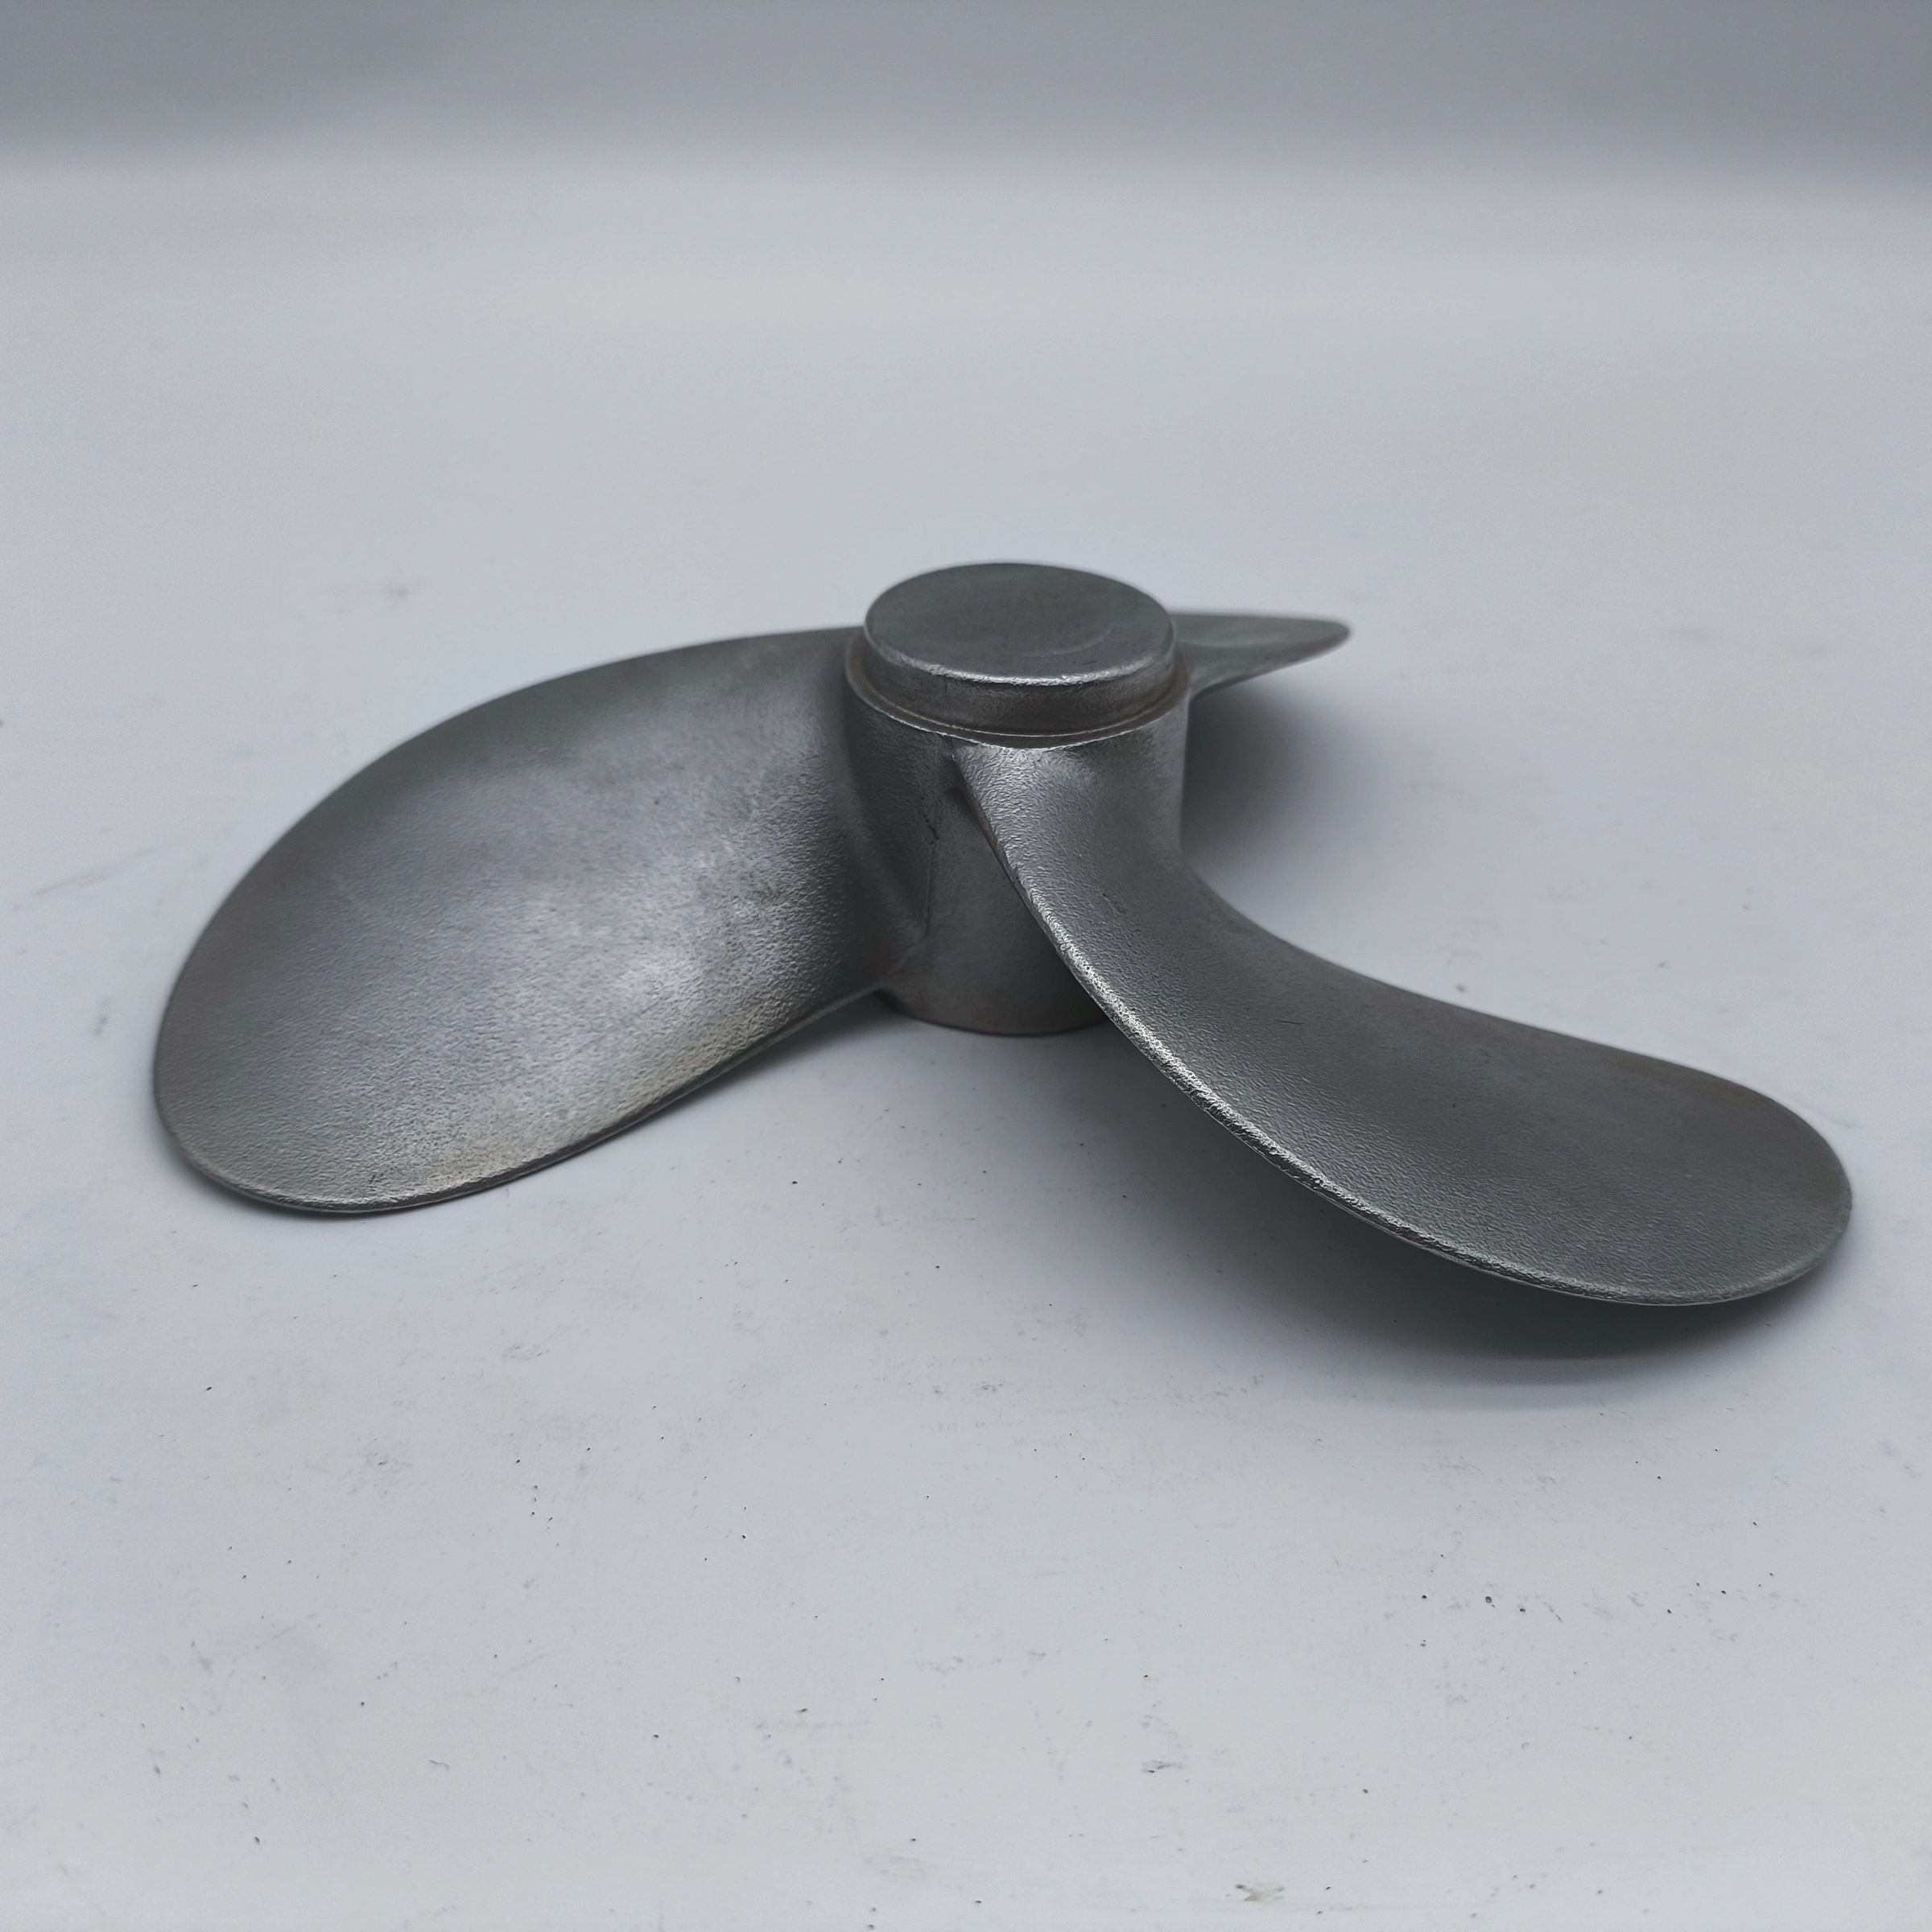
Custom Marine Cast Steel Three Blade Propellers with Coated Sand Investment Lost Wax Silica Sol Casting and CNC Enquiries
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
MaterialStainless Steel,Carbon Steel,Aluminum,Iron, and etc.
-
ProcessLost wax, Investment casting, Silica sol castingOther Process3D printing/CNC machining/Molding/Surface treatment/Heat treatment
-
SizeCustomer's Drawing RequiredToleranceCT4-CT6 (Investment Casting)
-
Surface roughness1.6-3.2 (Ra- μm)Drawing format2D/(PDF/CAD)3D(IGES/STEP)
-
Surface treatmentPainting,Powder Coating,Polishing, Electroplating, Shoot blasting,etc.CertificationISO9001:2015
-
Quality ControlStrictly 100% Inspection
Marine cast-steel three-blade propeller enquiries include coated-sand requirements and selected investment/lost-wax or silica-sol casting with CNC work. Separate stainless-steel, carbon-steel, aluminum or iron components need their own complete grade and route definition. Provide the actual propeller drawing and required supplied state.
Define blade, mounting and service geometry
Show the three-blade design and its connection to the intended assembly. Mark datums and dimensions controlling mounting, contact and working relationships. State the actual marine and rotating duty and the design-specific material or service-acceptance requirements for the selected component.
Assign casting and CNC acceptance
CT4–CT6 is the investment-casting reference, with roughness specified as Ra1.6–3.2 µm. Identify applicable features and the supplied stage separately from final CNC limits. Additional requests include 3D printing, molding, surface work and heat treatment, with each operation’s actual role to define.
Set surfaces and strict inspection
Painting, powder coating, polishing, electroplating and shot blasting are named finishes for a compatible substrate. Define coverage, masking and appearance at working or visible areas. The stated strict 100% inspection should assess agreed characteristics using specified methods and records.
- Supply 2D PDF/CAD or 3D IGES/STEP data.
- Provide quantity and the controlling revision.
- Request applicable ISO9001:2015 documents and scope.
- Explain what an initial propeller must demonstrate.
Retain accepted blade, mounting and finish changes with the drawing so production acceptance follows the actual marine component and delivered condition.