OEM Custom Aluminum Sand Die Cast Parts with CNC Tooling Prototypes and Separate Stainless Ductile Iron Services
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
Casting MethodDie Casting
-
MaterialStainless Steel, Ductile Iron, Aluminum, Spectrometer AnalysisSurface TreatmentShot Blasting, Powder Coating, Hot Dip Galvanized, E-coating, Painting
-
Tolerance & Surface RoughnessCT4-CT6 (Investment), CT10-CT12 (Sand), Ra 1.6-3.2 (Smooth Finish)Tooling & Mold DesignIn-house Tooling Design, Mold Manufacturing, Prototyping Service
-
Service TypeOEM/ODM Custom Manufacturing / PrototypingDrawing FormatsSTEP, STP, IGES, DXF, DWG, PDF
-
CertificationISO 9001, IATF 16949 , AS 9100 , CE, RoHSQuality Control100% Inspection, CMM, Projector, Caliper, Salt Spray Test
-
Lead Time7-10 Days (Prototype), 15-25 Days (Mass Production)
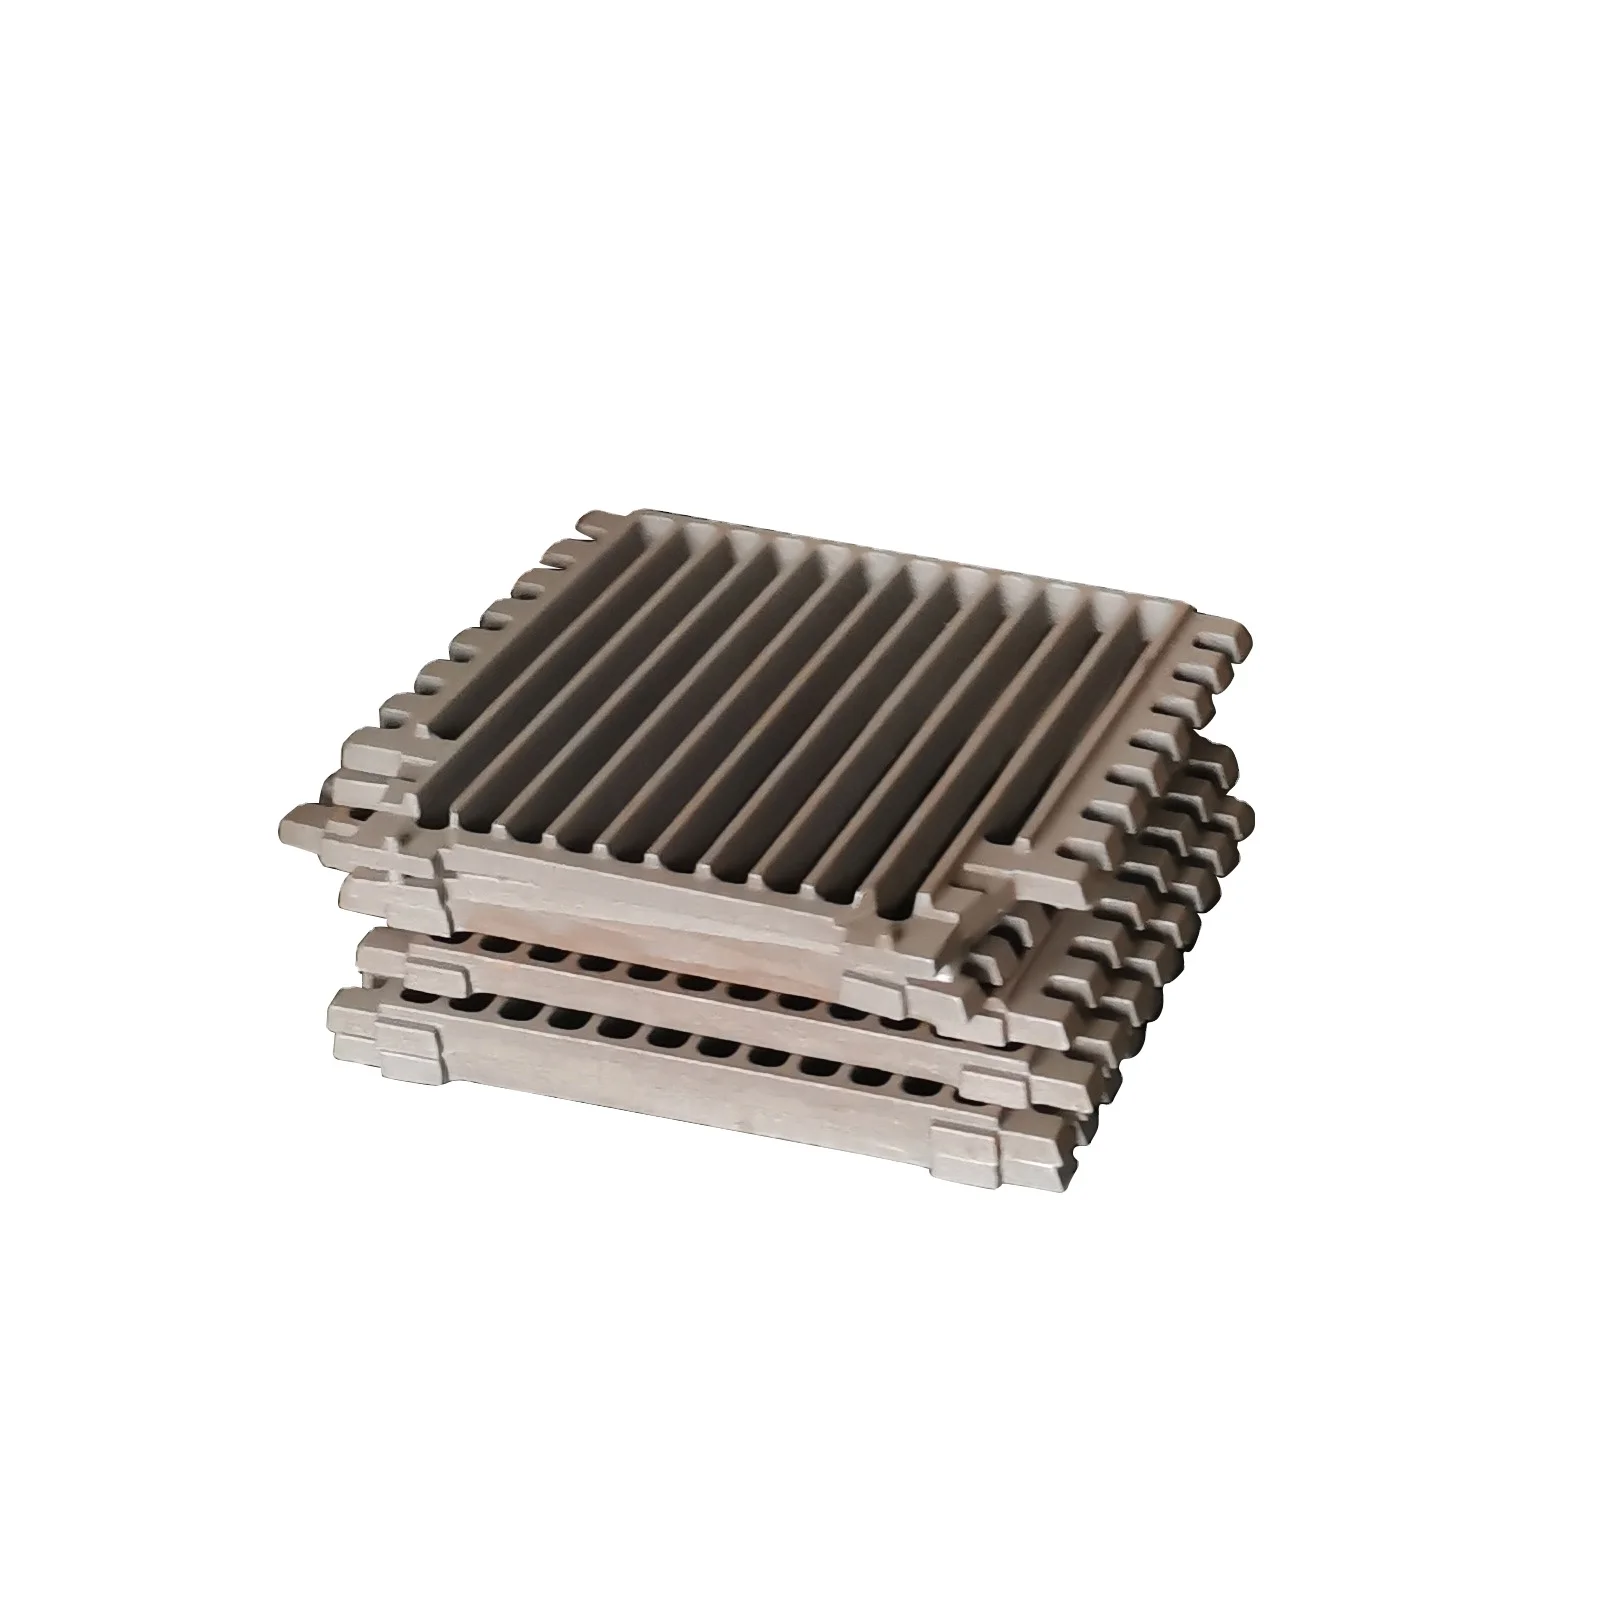
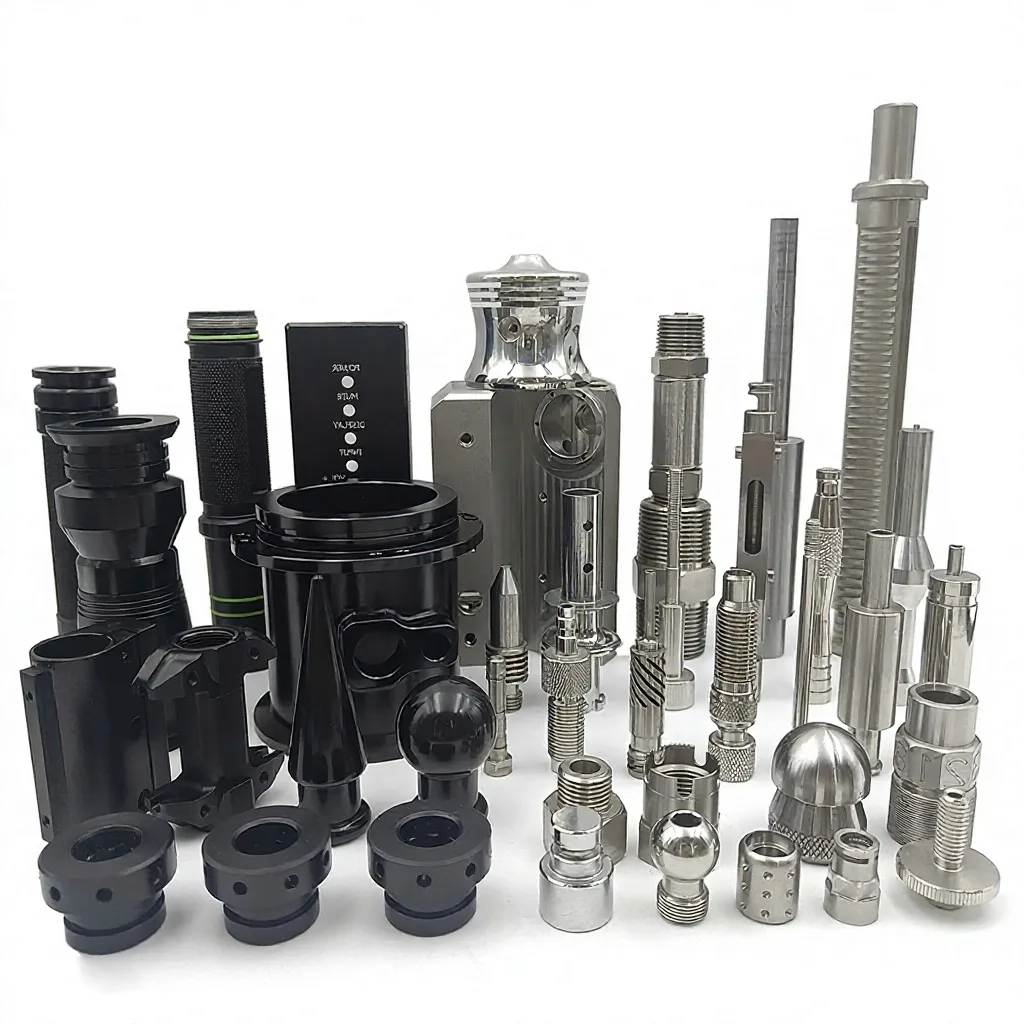
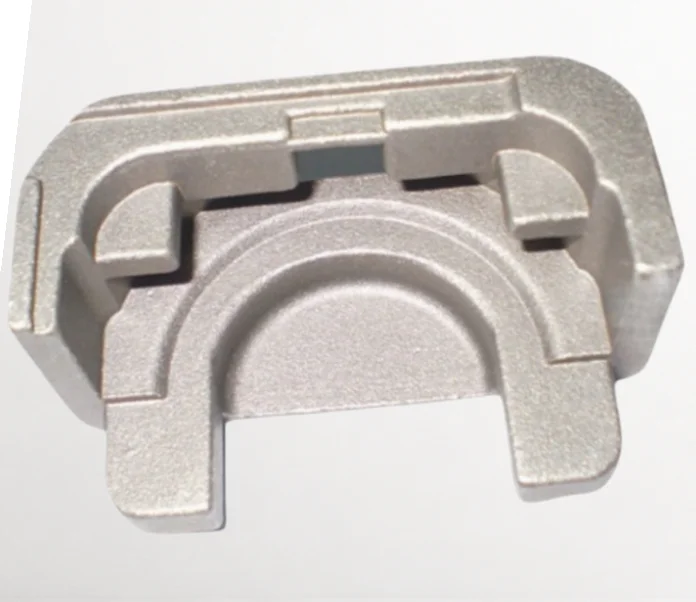
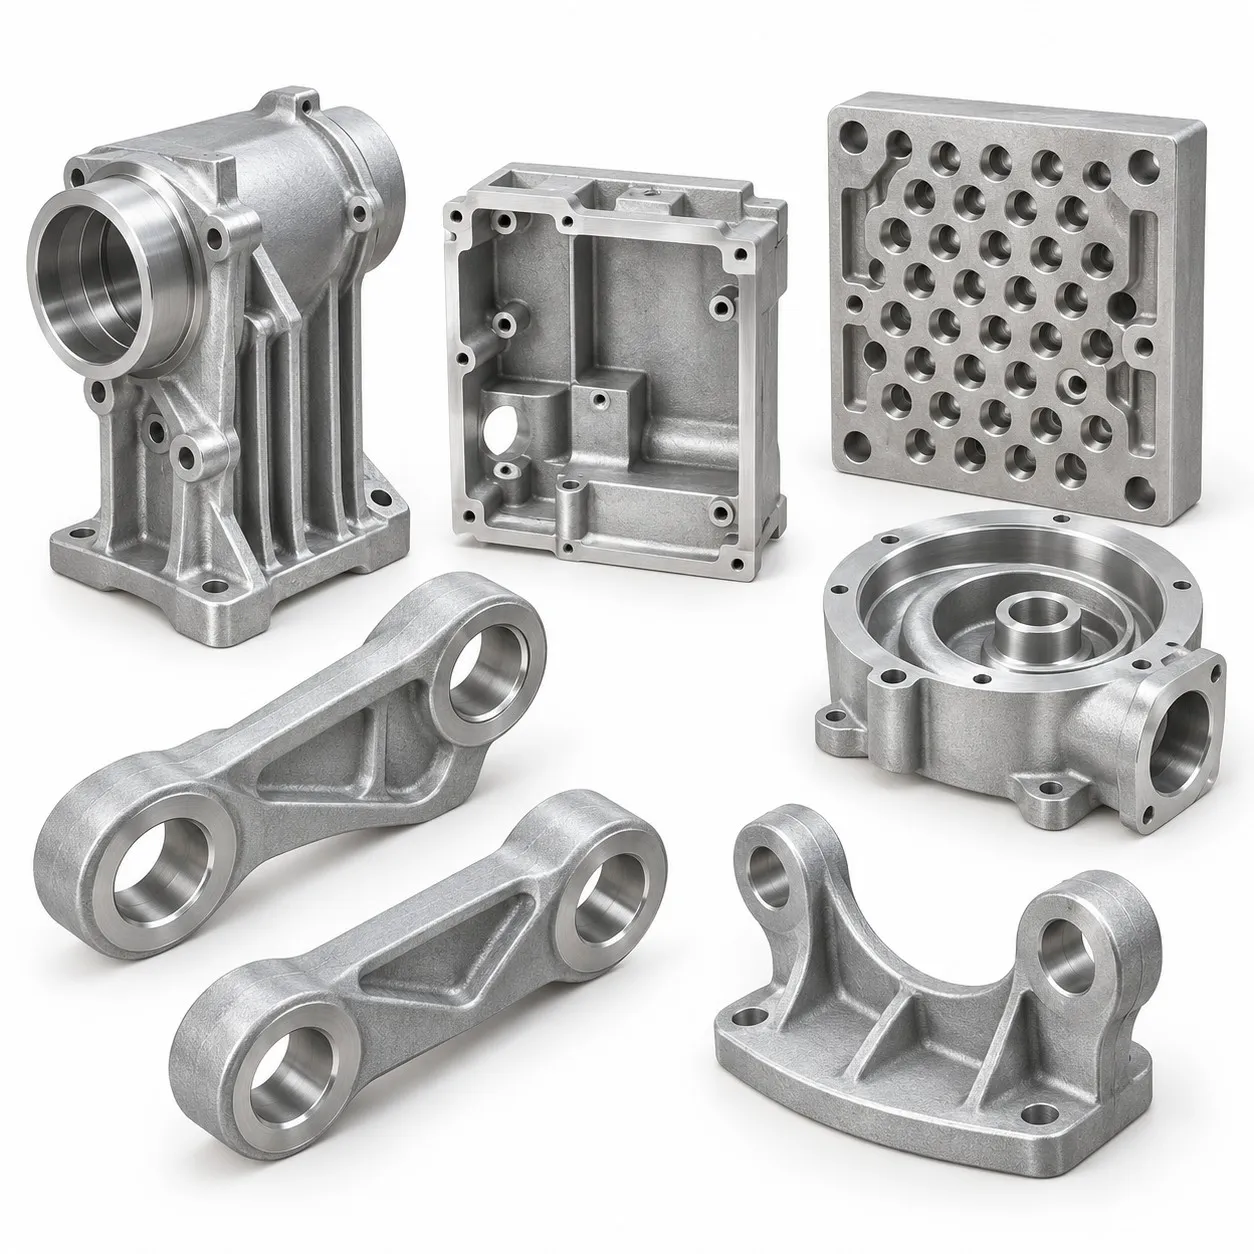
OEM/ODM aluminum-component enquiries cover sand or die casting with CNC machining, alongside separately specified stainless-steel or ductile-iron parts. In-house tooling design, mold manufacturing and prototyping are named services. Define the actual grade, route and deliverable for the drawing.
Assign casting and surface limits by process
References distinguish CT4–CT6 for investment casting from CT10–CT12 for sand casting. The smooth-finish reference is Ra1.6–3.2, with unit and applicable surfaces to be agreed. Identify the controlled dimensions and supplied stage used to accept the selected component.
Select inspection for the ordered part
The scope names 100% inspection, spectrometer analysis, CMM, projector, caliper and salt-spray testing. Define the actual methods, coverage and acceptance criteria needed for the material, dimensions and surface. Connect sample evaluation to those records and the chosen supplied condition.
Coordinate finish and design information
Shot blasting, powder coating, hot-dip galvanizing, E-coating and painting are finish choices for suitable materials. Mark coverage and masking around functional areas. Accepted formats are STEP, STP, IGES, DXF, DWG and PDF; keep their revision and geometry consistent.
Identify qualification and approval scope
Request applicable ISO9001, IATF16949, AS9100, CE and RoHS documents with their covered object and activities. Provide quantity and the controlled drawing with the part or tooling requirements. Keep production acceptance tied to the actual route, geometry and finish rather than assuming every material shares one configuration or qualification.