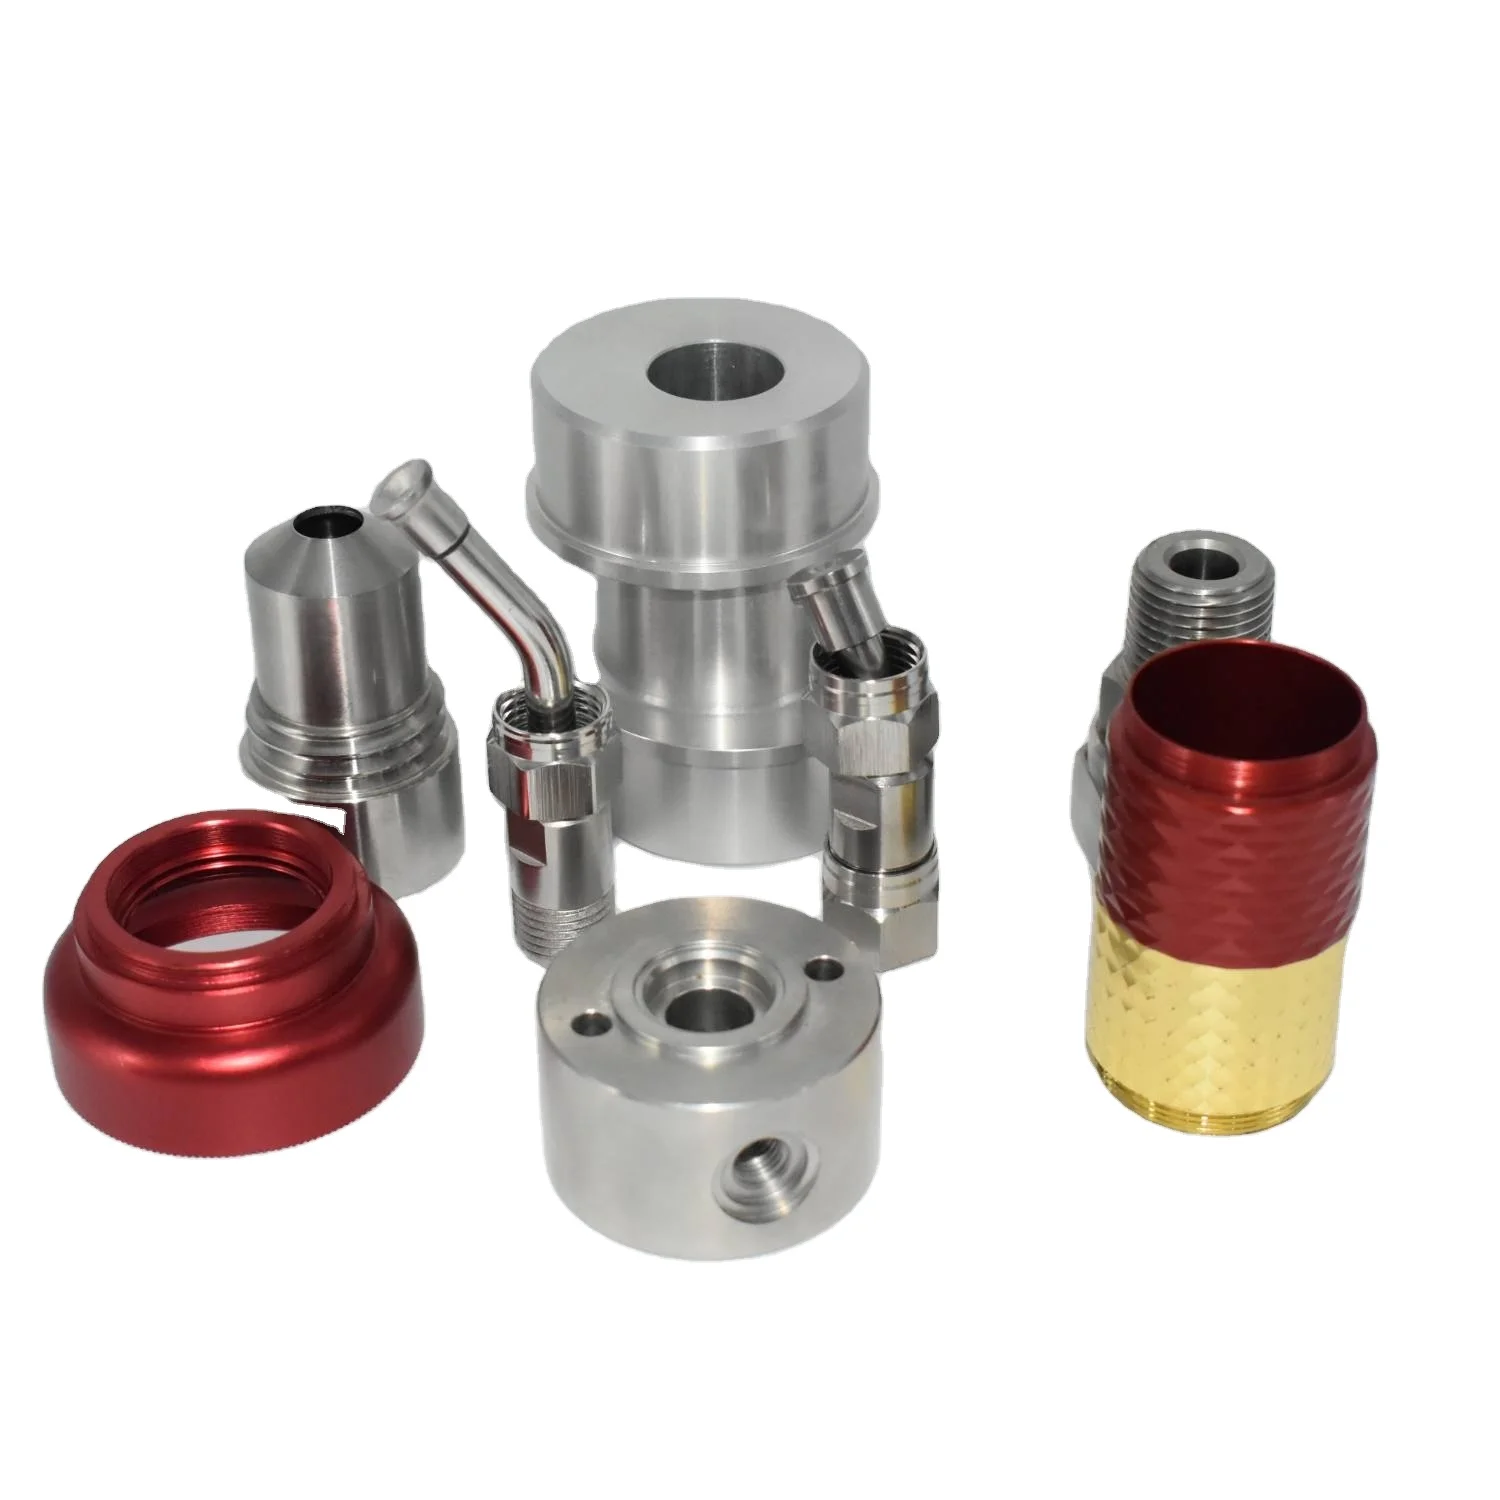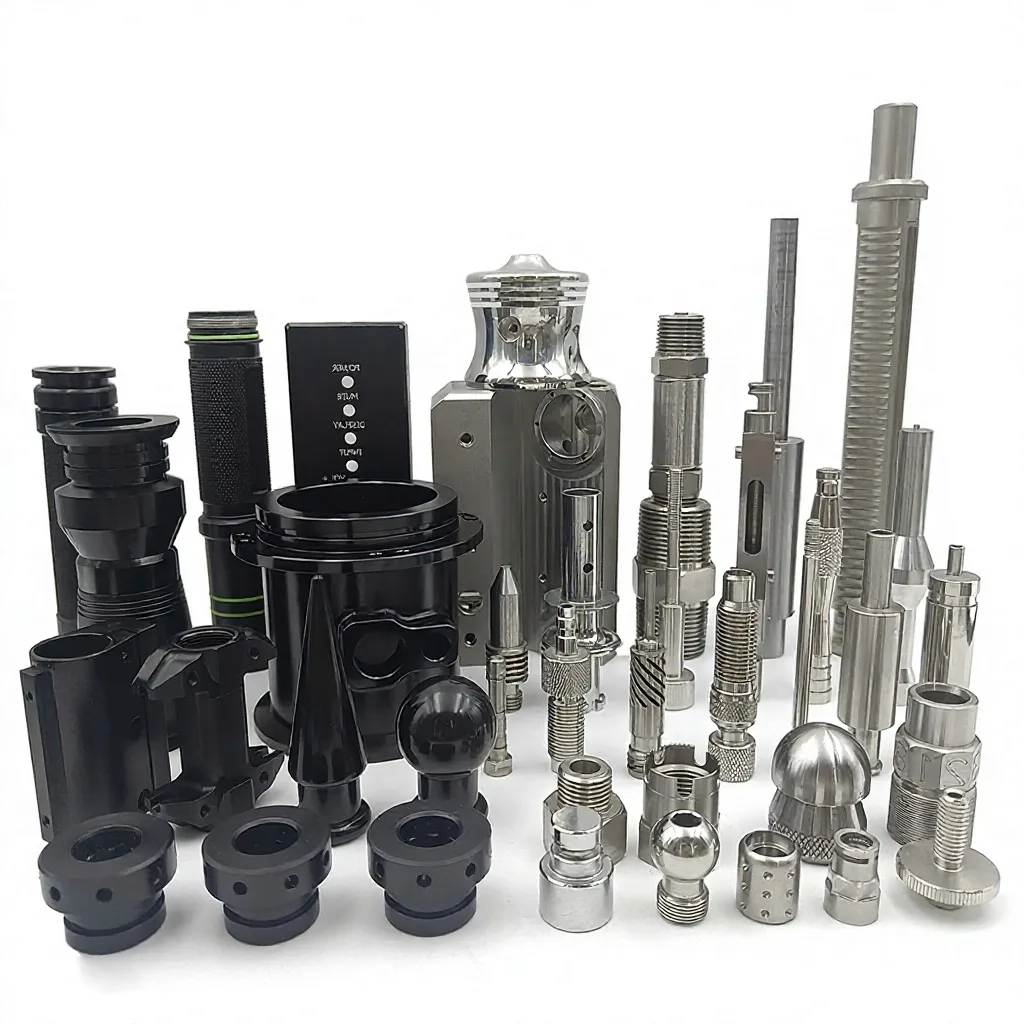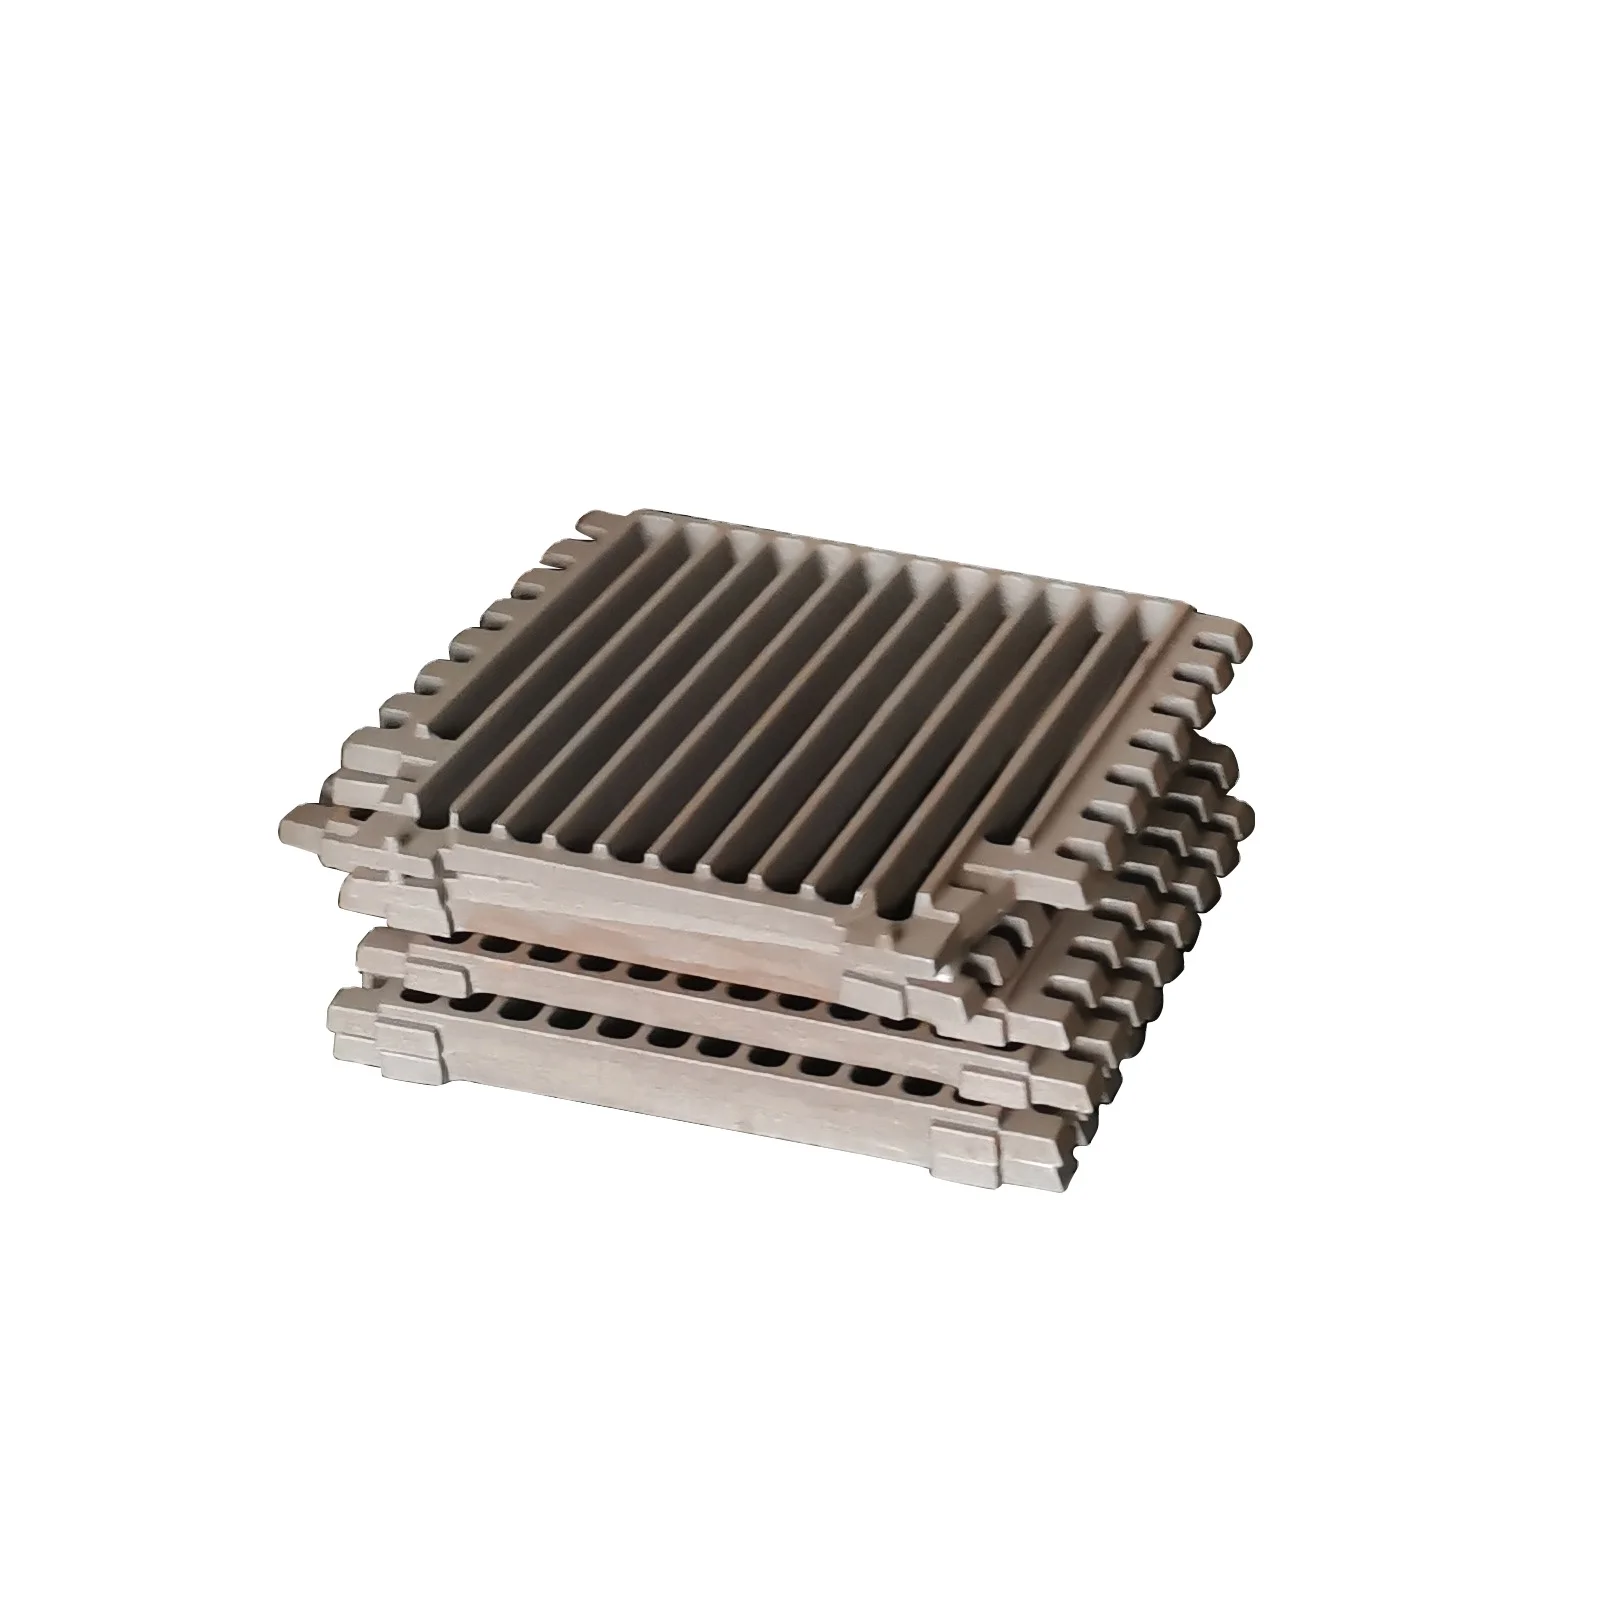
Large Heavy Stainless Steel Lost Wax Investment Cast Parts with CNC Machining up to IT7 CT4 CT8 and Selected Surface Requirements
Direct factory support
Get a quote that fits your project
Send your drawing or product reference, material grade and required quantity. Relia will review the requirements with you.
- Drawing & specification review
Confirm the supply scope and critical requirements.
- Samples before custom production
Review inspected samples before approving a batch.
- Inspection documents
Agree material and dimensional records for your part.
-
ItemLost Wax Casting Services Metal Sand Casting Investment Casting Parts
-
MaterialSS304,SS316 etc. As customers request.Manufacturing ProcessLost wax casting, option Lost wax casting
-
Casting ToleranceCT4-8 for casting for Lost Wax CastingMachining ProcessCNC Machining/ Lathing/ Milling/ Turning/ Boring/ Drilling etc.
-
Machining TolearnceUp to IT7, Ra 0.8~3.2 , according to customer requirementSurface TreatmentSurface Passivatin, Polish. As customer requests.
-
Package of steel castingMulti-layer wooden box/pallet, with big plastic bag insideLead TimeAbout 50 days for Lost Wax Casting
-
Servicelnvestment casting service
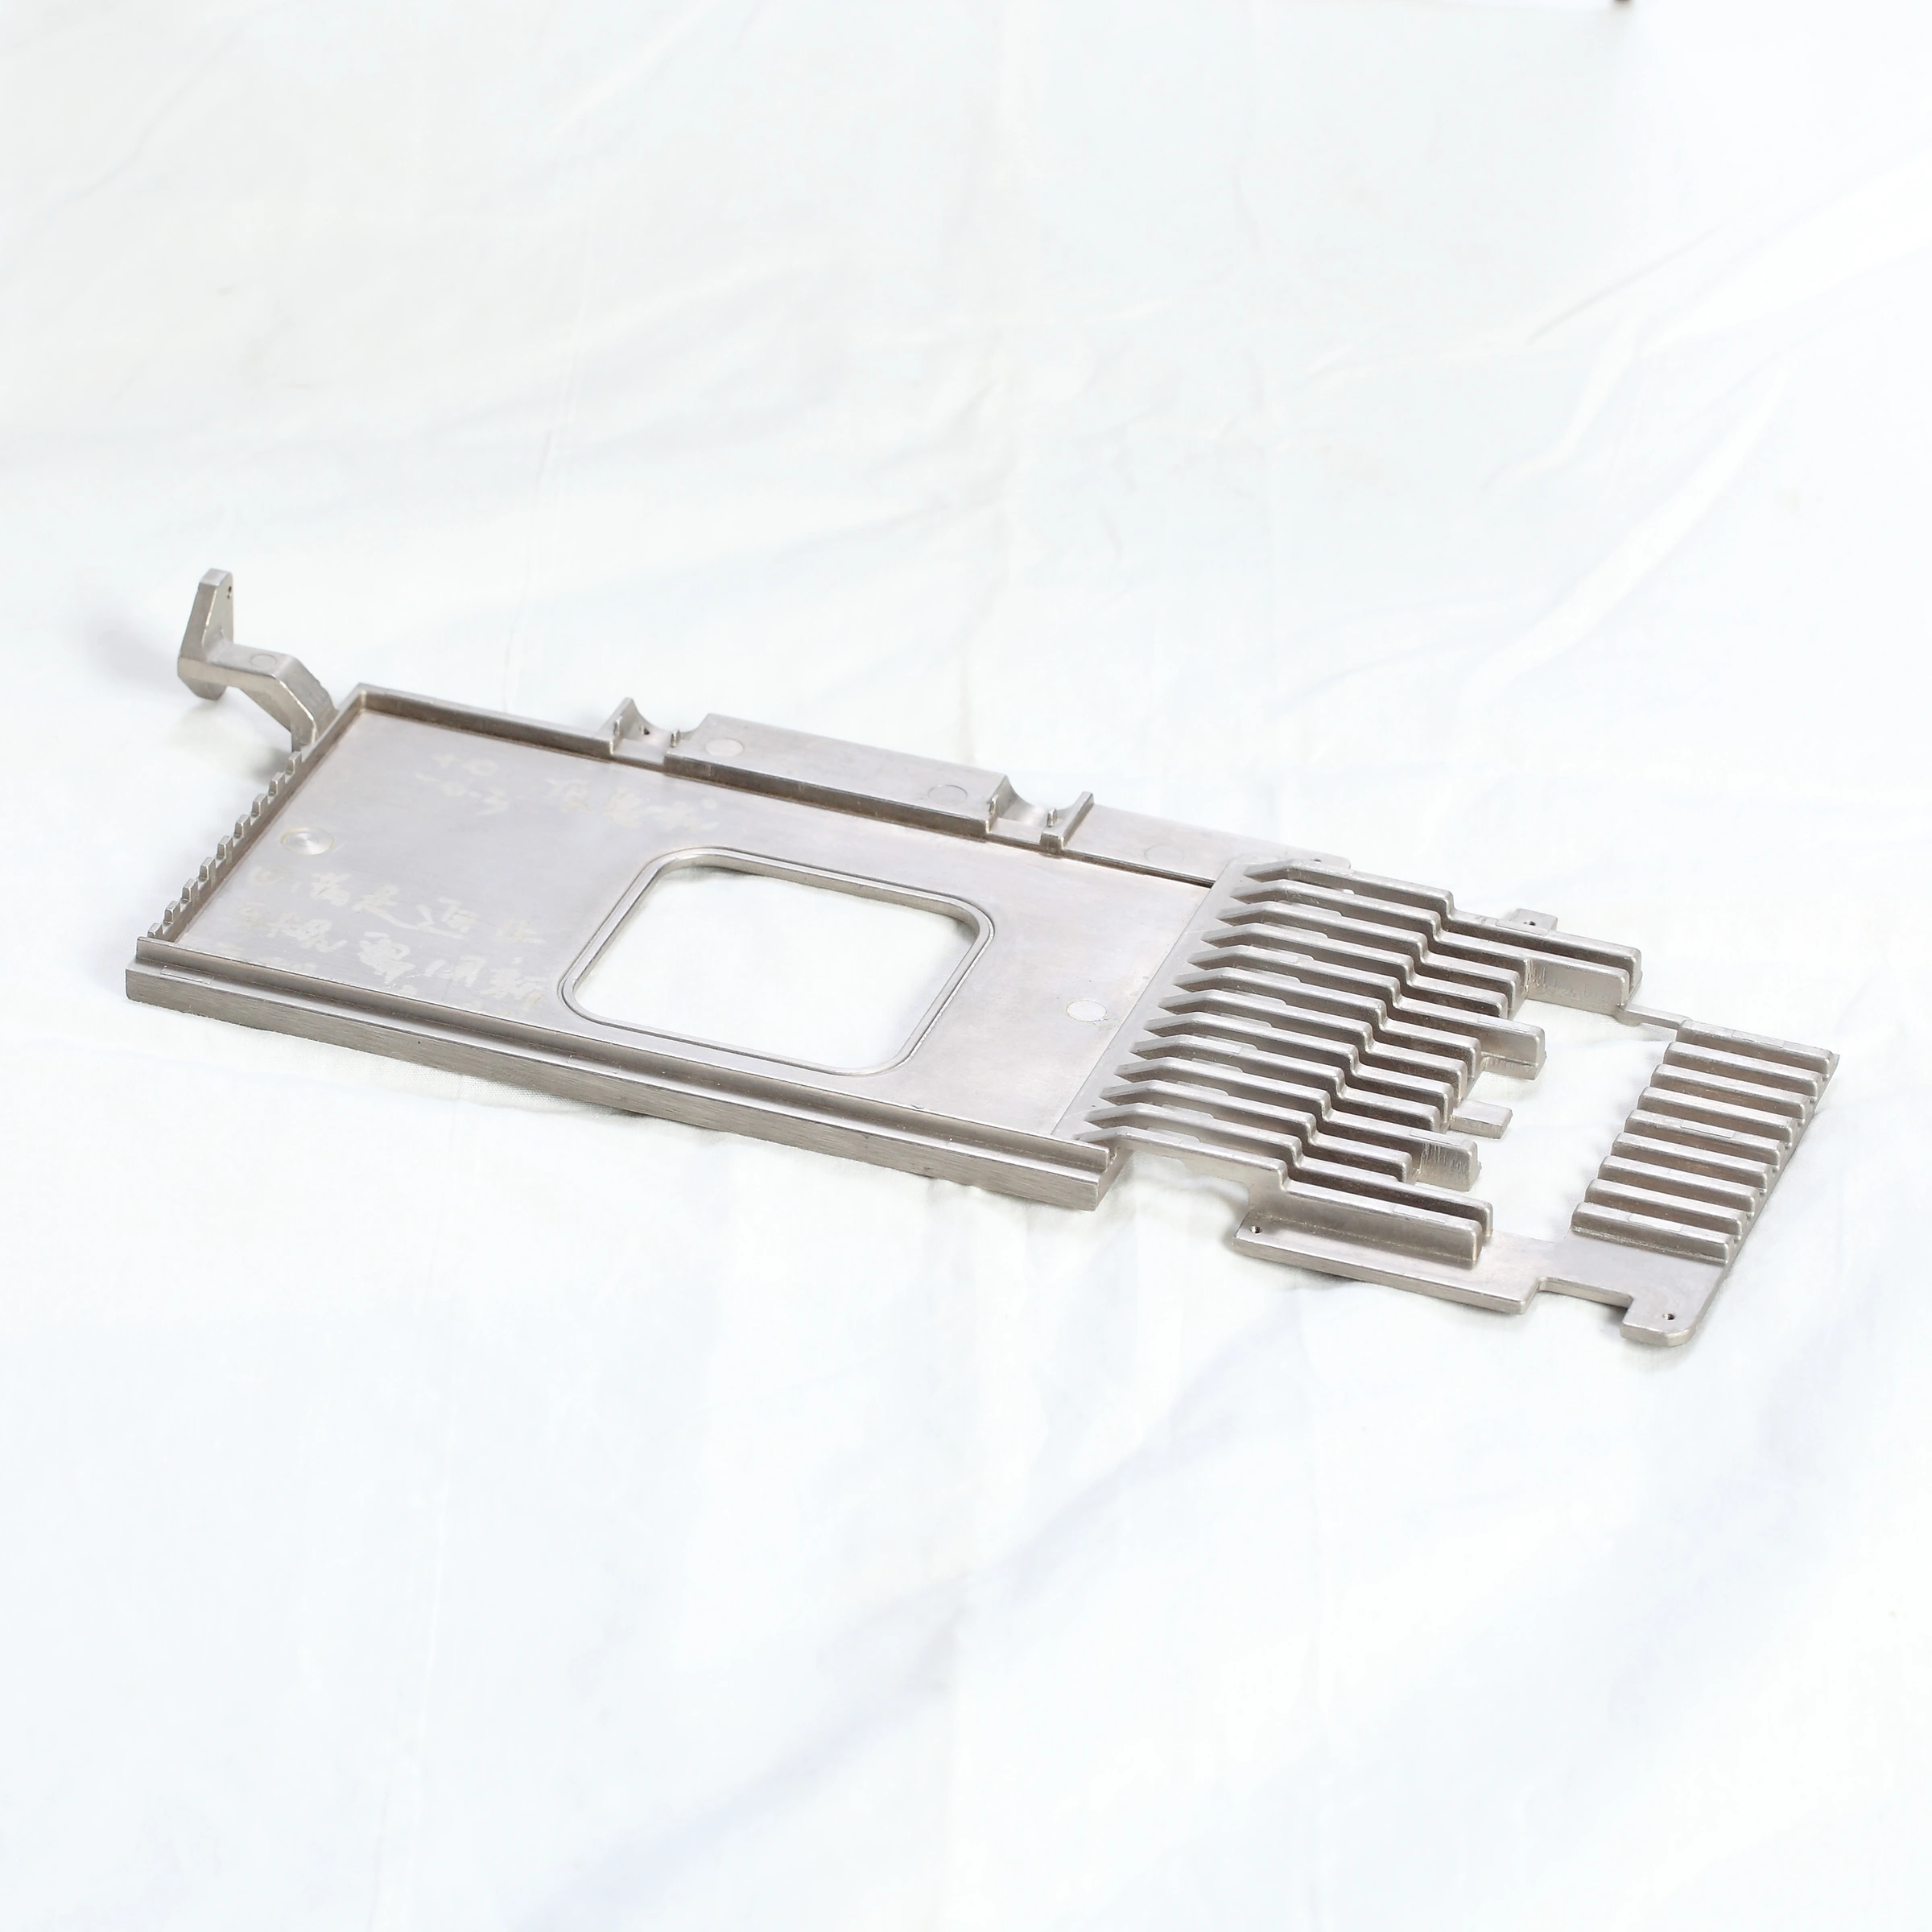
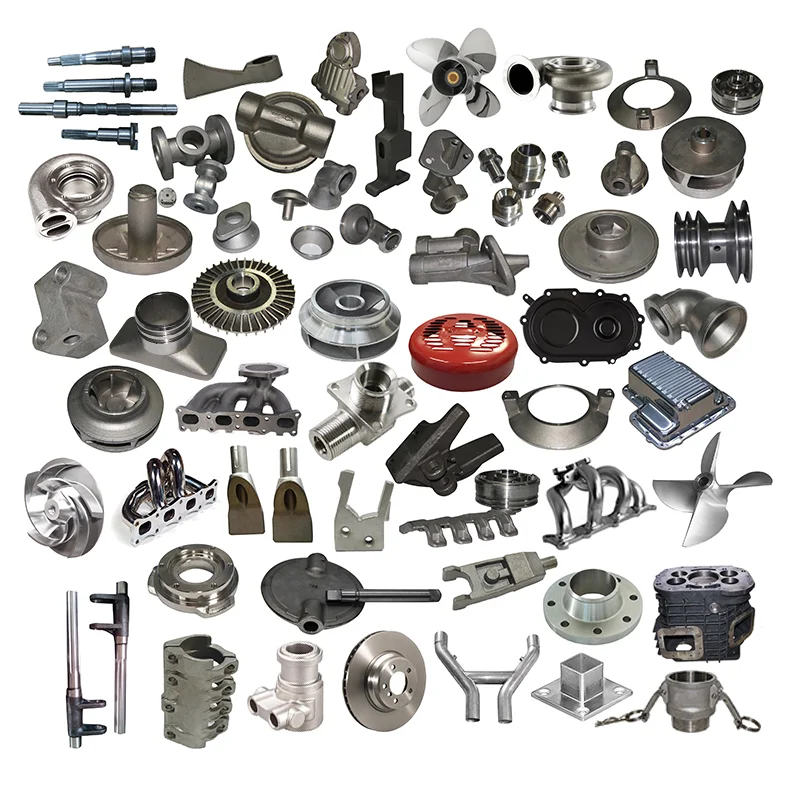
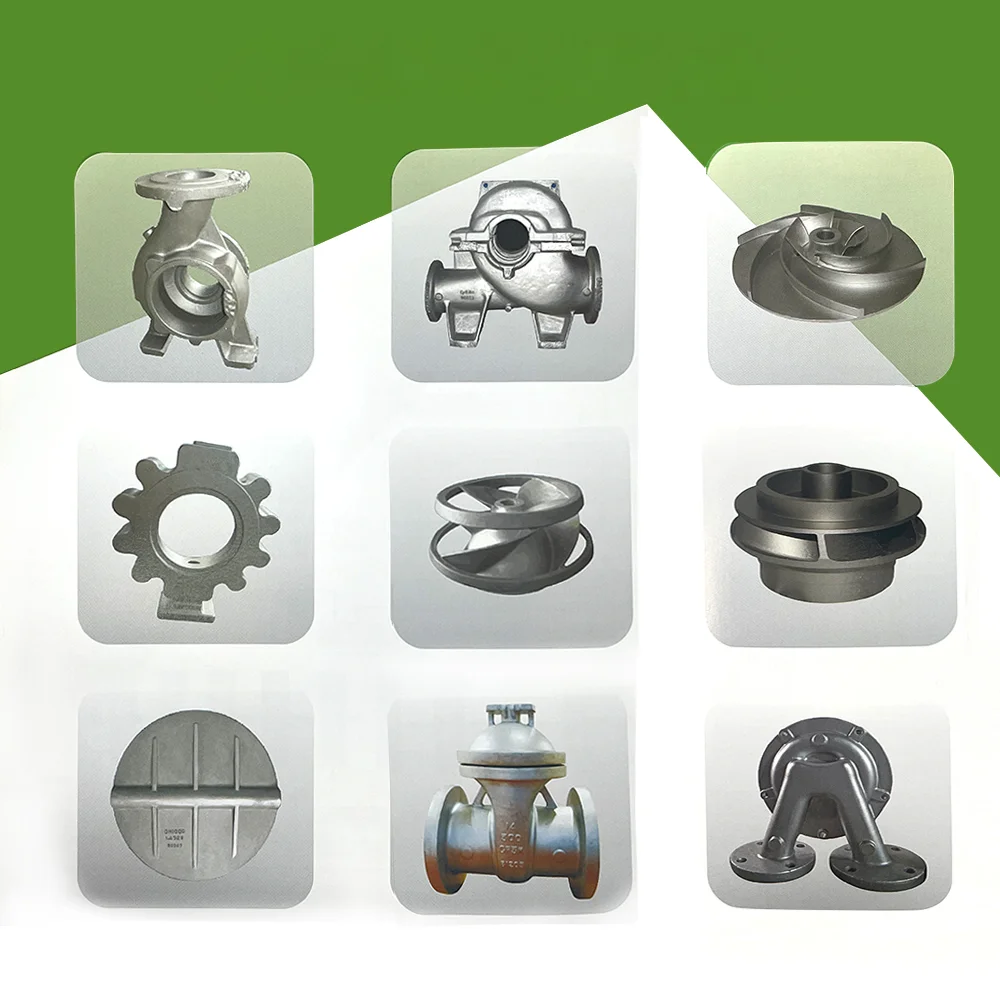
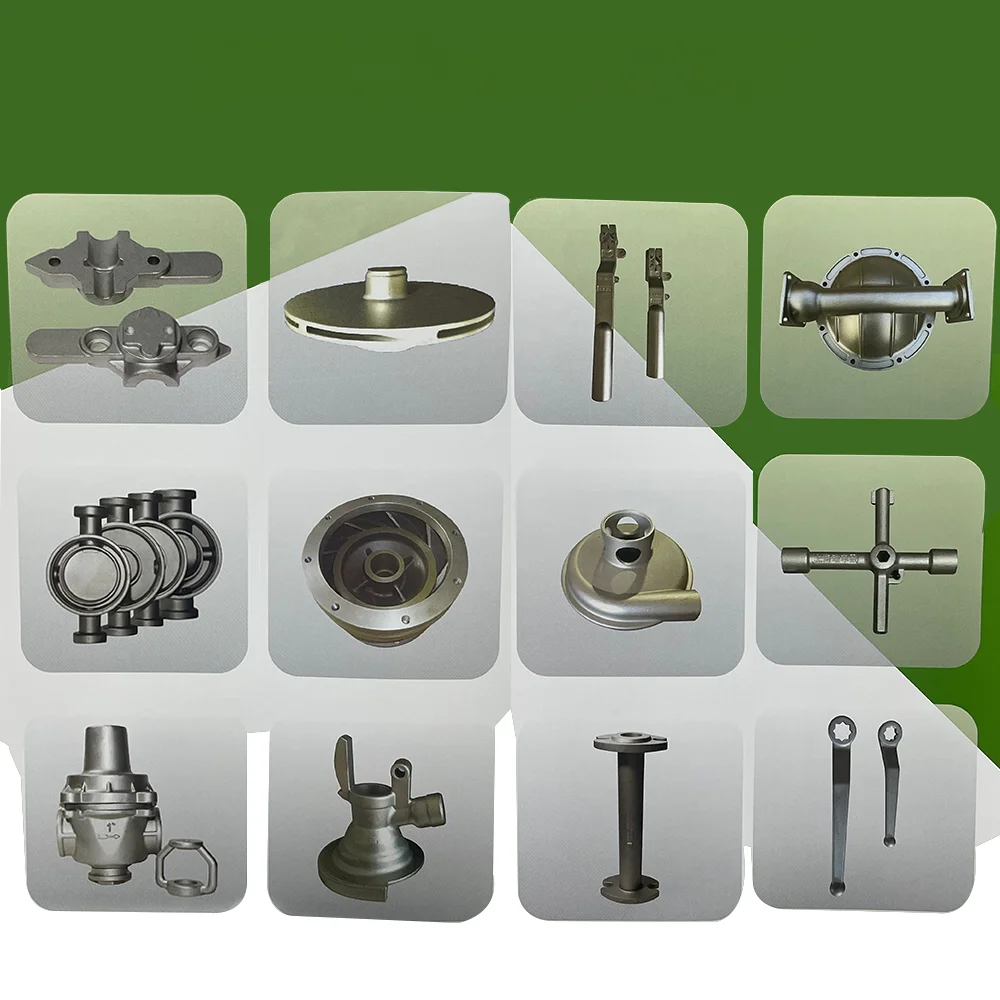
Large and heavy stainless-steel parts can be requested through lost-wax investment casting with CNC machining. SS304 and SS316 are material descriptions requiring the actual cast-grade specification selected for the order. Define component geometry, required condition and the supplied state around the chosen working duty.
Separate casting and final machining limits
Lost-wax casting tolerance is CT4–CT8, while machining is offered up to IT7 on selected dimensions. Mark the interfaces requiring final work and establish measurement conditions. A Ra0.8–3.2 requirement needs its unit and actual face defined for surface acceptance.
Scope the machining operations
Lathe/turning work, milling, boring and drilling are named alongside CNC machining. Identify the selected methods and the geometry each must deliver. An additional metal-sand-casting enquiry should establish its actual route separately from the chosen investment-cast component.
Specify passivated or polished condition
Passivation and polishing are available surface requests. Define treated areas, coverage and final appearance or working-contact result. Connect the required finish and any masking to the actual substrate and interfaces governing installation.
- Packing uses multilayer wooden box or pallet with a large inner plastic bag.
- State the stainless part’s quantity and controlling drawing revision.
- Identify material, dimensional and surface approval records.
- Agree actual size and capacity scope for the selected large component.
Retain accepted grade, machining and supplied-surface decisions within the component definition used for further requests.